
Double End Studs
Super Industries
“Global Manufacturer of Heavy & Custom Engineered Fasteners for Oil & Gas, Power & EPC Contractors.”
Super Industries manufactures Double End Studs designed for heavy mechanical assemblies used in energy, industrial processing, and infrastructure equipment. These fastening components are supplied for engineering applications where high clamping reliability, controlled preload, and repeatable assembly conditions are required.
1. Industry Context & System Relevance
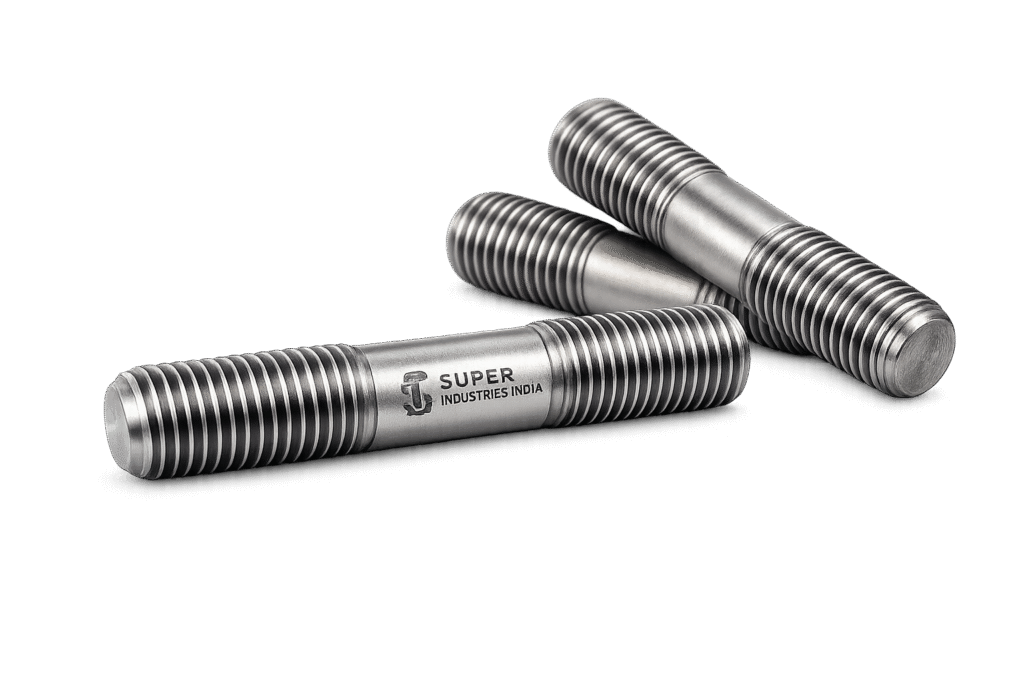
Role of Double End Studs in Heavy Mechanical Assemblies
Large industrial systems depend on high-integrity mechanical joints that maintain preload under thermal, mechanical, and vibration loads. Double end studs are used in these systems as permanent threaded anchors within equipment bodies, allowing components to be clamped using removable nuts.
Typical equipment assemblies require repeated maintenance cycles, inspection intervals, and controlled torque application. In such systems, direct bolt fastening can damage tapped holes or reduce thread integrity over time. Double end studs address this issue by keeping the stud fixed within the base material.
Industrial Systems Using Double End Studs
Double end studs are commonly specified in the following industrial environments:
Oil & Gas Facilities
Production manifolds
Separator vessels
Compressor skids
Pipeline pump stations
Refineries
Distillation column assemblies
Reactor equipment
Heat exchanger covers
Process piping flanges
Power Plants
Steam turbines
Boiler systems
Generator housings
Pressure piping equipment
Petrochemical Units
Cracking furnaces
Hydrocarbon processing equipment
Reactor vessels
Catalytic systems
Pressure Equipment
Pressure vessels
Manways and access covers
Flanged pressure connections
Rotating Machinery
Compressor casings
Pump housings
Turbine casings
Heavy Structural Equipment
Large gear housings
Mining equipment
Steel mill machinery
Infrastructure Machinery
Bridge equipment assemblies
Heavy fabrication systems
Across these sectors, mechanical engineers frequently select stud-nut fastening systems instead of conventional bolts due to the performance advantages of stud installation.
Why Double End Studs Are Preferred Over Conventional Bolts
1. Protection of Base Threads
When bolts are repeatedly installed and removed, the internal threads of the base component experience wear. This is particularly problematic in expensive equipment bodies such as:
- turbine casings
- pump housings
- pressure vessel flanges
With double end studs, the stud remains fixed in the tapped hole. Only the external nut is removed during maintenance, preserving the integrity of the base material threads.
2. Improved Alignment During Assembly
Studs act as alignment guides during installation of heavy components.
For example:
- Heat exchanger covers
- Large flange connections
- Turbine casing halves
When the stud remains installed in the base flange, components can be positioned accurately before nut tightening begins.
This reduces installation errors and improves assembly efficiency.
3. Improved Load Distribution
Double end studs distribute load across the threaded engagement region more uniformly than conventional bolts.
Benefits include:
- improved stress distribution in base threads
- reduced localized thread damage
- improved joint reliability
4. High Temperature Stability
In high-temperature systems, such as boilers and steam turbines, repeated thermal cycles can cause thermal expansion and contraction of bolted joints.
Stud-nut systems provide more predictable performance because:
- the stud remains thermally stabilized in the base component
- nut tightening occurs externally
This reduces the risk of thread galling and internal thread damage.
5. Maintenance Efficiency
Maintenance crews prefer stud systems in large assemblies because they simplify disassembly.
Benefits include:
- easier component removal
- consistent torque application
- reduced installation time
Studs also allow multiple tightening cycles without degrading the base material.
6. Reduced Thread Wear in Critical Components
In heavy equipment such as compressors and turbines, the base components may be:
- forged steel housings
- pressure vessel shells
- expensive castings
Using double end studs prevents repeated wear of internal threads in these components, extending equipment life.
Mechanical Stability in Critical Equipment
Double end studs are particularly important where high clamping loads must be maintained under extreme service conditions.
Examples include:
- high pressure flanged joints
- rotating machinery casings
- high temperature equipment
Studs allow engineers to maintain controlled preload while minimizing damage to base materials.
Super Industries
Global Manufacturer of Heavy & Custom Engineered Fasteners & Flanges.
2. Technical Definition
Definition of Double End Studs
Double End Studs are threaded fasteners consisting of a cylindrical rod with threads provided at both ends, while the center portion may be either threaded or unthreaded depending on design requirements.
In most configurations:
- one threaded end is installed permanently into a tapped hole in the base component
- the opposite threaded end is used for nut tightening
The stud therefore functions as a fixed anchor within the base structure, enabling removable clamping through external nuts.
Structural Characteristics
Typical characteristics of double end studs include:
• Cylindrical steel rod body
• Threaded ends on both sides
• Controlled thread length on each end
• Defined overall stud length
• Chamfered thread entry
The center section may be:
- fully threaded
- partially threaded
- plain shank depending on design standard
Stud-Nut Fastening System
Double end studs operate as part of a two-component fastening system:
Component 1 — Stud
Installed into the base material.
Component 2 — Nut
Applies clamping force when tightened.
This configuration separates:
- the threaded engagement region in the base material
- the load application region during tightening
The result is improved durability of the threaded hole.
Thread Engagement Logic
For effective performance, stud installation must provide sufficient thread engagement length within the base component.
Typical engineering guidance suggests:
Thread engagement depth ≈ 1 to 1.5 times stud diameter
This ensures that:
- shear strength of engaged threads exceeds tensile strength of the stud
- the stud fails before thread stripping occurs
Exact values depend on:
- base material strength
- stud material grade
- operating loads
Difference Between Double End Studs and Other Stud Types
Stud fasteners are often confused with other threaded components. However, several distinctions exist.
Double End Studs
Characteristics:
• Threads on both ends
• Stud installed permanently in base component
• Nut used on exposed end
• Both thread lengths typically equal
Typical applications:
- machinery housings
- structural assemblies
- maintenance-accessible joints
Stud Bolts
Stud bolts are different in configuration.
Characteristics:
• Fully threaded across entire length
• Nuts installed on both ends
• Used in flange connections
Typical applications:
- pressure piping flanges
- ASME B16 flange assemblies
Tap End Studs
Tap end studs are similar but include unequal thread lengths.
Characteristics:
• short threaded end (tap end)
• longer nut end
• designed for deep tapped holes
Used where internal threads are deeper than external clamping requirements.
Fully Threaded Studs
Fully threaded studs contain continuous threads across the entire length.
Characteristics:
• no plain shank section
• equal thread pitch across rod
• often used with two nuts
Applications include general fastening or tie-rod style assemblies.
Functional Distinction
From an engineering perspective:
| Fastener Type | Installation Method | Typical Use |
|---|---|---|
| Double End Studs | One end fixed in base | Machinery assemblies |
| Stud Bolts | Nuts on both ends | Flange joints |
| Tap End Studs | Deep internal thread engagement | Equipment frames |
| Fully Threaded Studs | Continuous threading | Structural fastening |
Selecting the correct stud type depends on:
- equipment geometry
- load conditions
- service environment
- maintenance requirements
Super Industries
Global Manufacturer of Heavy & Custom Engineered Fasteners & Flanges
3. Mechanical Fastening Principle
Understanding the mechanics of threaded fasteners is critical for engineers specifying double end studs.
The purpose of the stud-nut assembly is to generate controlled clamping force, commonly called preload, which holds the joined components together.
Bolt Preload Mechanics
When a nut is tightened on the exposed thread of a double end stud, the stud experiences tensile elongation.
This elongation produces a clamping force between the joined components.
The behavior can be summarized as:
Nut tightening → stud tension → joint compression.
The stud effectively behaves like an elastic spring.
Elastic Stretch of Studs
A properly tightened stud experiences elastic elongation.
This elongation provides:
• stable clamping force
• resistance to loosening
• predictable load distribution
If tightening exceeds the elastic limit, plastic deformation occurs and the stud may lose its ability to maintain preload.
Load Transfer Mechanism
Load transfer occurs through several interfaces:
- Nut to stud threads
- Stud to internal threads in base material
- Clamped components between nut and base
The tensile force generated in the stud is balanced by compressive force in the jointed components.
Thread Friction Behavior
When tightening nuts on studs, most of the applied torque does not directly produce tension.
Typical distribution:
• 50% torque lost to thread friction
• 40% lost to nut face friction
• ~10% converted into useful preload
Therefore, lubrication conditions significantly affect the final clamping force.
Friction Coefficients
Friction conditions vary depending on surface treatment.
Typical approximate coefficients:
Dry threads: 0.18 – 0.25
Lubricated threads: 0.10 – 0.15
Lower friction increases achievable preload for the same torque.
Lubrication Impact on Torque Values
Lubrication reduces friction between mating threads.
Common lubricants include:
- molybdenum disulfide compounds
- graphite-based lubricants
- anti-seize compounds
Proper lubrication improves:
• torque consistency
• preload accuracy
• prevention of galling in stainless steel studs
Torque vs Tension Relationship
Torque applied to the nut generates tension in the stud.
This relationship is approximated by the formula:
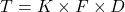
Where:
T = tightening torque
F = desired preload force
D = nominal stud diameter
K = torque coefficient
Below is the mathematical relationship used in fastening calculations.
T = K F D
The torque coefficient K depends on friction conditions.
Typical values:
Dry steel threads: 0.20 – 0.25
Lubricated threads: 0.15 – 0.18
Joint Compression Behavior
The jointed components behave like a compressive spring.
When the stud is tensioned:
• stud stretches
• joint compresses
A stable joint requires the stud stiffness to be lower than joint stiffness, ensuring that most external loads do not significantly reduce clamping force.
Importance of Controlled Preload
Proper preload is critical to prevent:
• joint separation
• fatigue failure
• vibration loosening
In pressure equipment and rotating machinery, insufficient preload can cause:
- flange leakage
- gasket failure
- bolt fatigue cracking
Thread Root Stress Concentration
Threads contain geometric discontinuities that create stress concentration points.
The root of the thread is the most critical region where fatigue cracks may initiate.
Engineering practices therefore emphasize:
• controlled preload
• correct thread rolling processes
• material quality
These factors increase fatigue life.
Summary of Mechanical Behavior
Double end studs operate as elastic tension members within mechanical assemblies.
The stud:
• converts tightening torque into axial tension
• compresses joined components
• maintains joint integrity under load
Understanding these mechanics is essential for:
- torque specification
- stud material selection
- joint reliability analysis
4. Applicable Standards (ASTM / DIN / ISO / ASME)
Engineering-grade Double End Studs used in heavy industrial systems are manufactured and supplied in accordance with internationally recognized standards. These standards define material chemistry, mechanical properties, thread geometry, dimensional tolerances, and testing requirements necessary for reliable operation in mechanical assemblies.
Compliance with these standards allows EPC contractors, consultants, and inspection agencies to verify that the supplied fasteners meet specified performance requirements for pressure equipment, rotating machinery, and structural assemblies.
ASTM Standards for Double End Studs
ASTM standards primarily define material grades and mechanical properties used for studs operating under different temperature and service conditions.
ASTM A193
ASTM A193 covers alloy and stainless steel bolting materials for high-temperature or high-pressure service.
Common grades used for Double End Studs include:
| Grade | Material Type | Typical Application |
|---|---|---|
| B7 | Alloy steel | Pressure vessels, flanges, machinery |
| B16 | Chromium-molybdenum alloy | High temperature equipment |
| B8 | Stainless steel 304 | Corrosion resistant environments |
| B8M | Stainless steel 316 | Chemical processing equipment |
These grades are widely used in:
- petrochemical plants
- refineries
- steam systems
- rotating machinery housings
ASTM A320
ASTM A320 specifies alloy steel bolting materials for low-temperature service.
Typical grades include:
| Grade | Material | Service Conditions |
|---|---|---|
| L7 | Quenched & tempered alloy steel | Low temperature service |
| L43 | Nickel alloy steel | Cryogenic environments |
These studs are used where impact resistance at sub-zero temperatures is required.
Applications include:
- LNG facilities
- cryogenic equipment
- cold climate pipeline systems
ASTM A307
ASTM A307 covers carbon steel bolts and studs for general engineering applications.
These are commonly used in:
- structural equipment
- machinery frames
- infrastructure assemblies
ASTM A354
ASTM A354 specifies high-strength alloy steel fasteners.
Grades commonly used include:
| Grade | Strength Level |
|---|---|
| BD | High-strength structural fasteners |
These materials are used where high tensile load capacity is required.
ASME Standards
ASME B1.1 — Unified Inch Screw Threads
This standard defines:
- thread form geometry
- pitch diameter tolerances
- thread engagement characteristics
It governs UNC and UNF thread series used in inch-based stud designs.
ASME B18 Series — Fastener Specifications
The ASME B18 standards define:
- dimensional characteristics of fasteners
- manufacturing tolerances
- thread length and chamfer details
These standards ensure interchangeability of fasteners used in large industrial assemblies.
DIN Standards
DIN standards are widely used in European industrial systems.
Two primary DIN standards govern double end studs.
DIN 939
DIN 939 defines double end studs with unequal thread lengths.
Typical features include:
- tap end thread
- nut end thread
- defined center shank section
These studs are used where deeper internal thread engagement is required.
DIN 938
DIN 938 specifies double end studs with equal thread lengths on both ends.
These are typically used in:
- machine assemblies
- structural equipment
- maintenance-accessible joints
ISO Standards
ISO 898
ISO 898 specifies mechanical properties of fasteners made of carbon and alloy steel.
The standard defines:
- yield strength
- tensile strength
- elongation limits
- hardness ranges
Common ISO property classes include:
| Class | Minimum Tensile Strength |
|---|---|
| 8.8 | 800 MPa |
| 10.9 | 1000 MPa |
| 12.9 | 1200 MPa |
These classes determine load capacity of studs under tensile stress.
ISO Metric Thread Standards
ISO metric standards define:
- thread pitch
- thread angle (60°)
- tolerance classes
Metric thread systems are widely used in European and Asian industrial equipment.
Role of Standards in Stud Selection
Engineering teams select Double End Studs based on three primary criteria defined by standards:
- Mechanical strength
- Temperature capability
- Corrosion resistance
Standards allow designers to match stud grade with service conditions in equipment systems.
5. Material & Grade Options
Material selection is critical for Double End Studs because the stud must withstand tensile stress, environmental exposure, and thermal cycling without failure.
Industrial studs are manufactured from several material categories depending on application requirements.
Carbon Steel Stud Materials
Carbon steel studs are widely used in general industrial assemblies where corrosion exposure is limited.
Typical grades include:
| Material Grade | Standard | Application |
|---|---|---|
| ASTM A307 | Carbon steel | Structural assemblies |
| ASTM A193 B7 | Alloy steel | Pressure equipment |
| ASTM A193 B16 | Cr-Mo alloy steel | High temperature systems |
Low Temperature Alloy Steels
Low-temperature studs are designed to maintain impact resistance and toughness at sub-zero temperatures.
Typical materials include:
| Grade | Material Type | Typical Use |
|---|---|---|
| ASTM A320 L7 | Quenched & tempered alloy steel | Low temperature piping |
| ASTM A320 L43 | Nickel alloy steel | Cryogenic systems |
These materials are tested using Charpy impact tests to verify toughness.
Stainless Steel Stud Materials
Stainless steels are used where corrosion resistance is required.
Typical grades include:
| Grade | Composition | Application |
|---|---|---|
| ASTM A193 B8 | SS304 | Food and chemical equipment |
| ASTM A193 B8M | SS316 | Marine and chemical plants |
Advantages include:
- corrosion resistance
- oxidation resistance
- non-magnetic properties
Duplex & Super Duplex Materials
Duplex stainless steels provide higher strength and improved corrosion resistance compared to standard stainless steels.
Common grades include:
| Grade | Material Type |
|---|---|
| F51 | Duplex stainless steel |
| F53 | Super duplex |
| F55 | Super duplex high strength |
These materials are commonly used in:
- offshore oil platforms
- seawater equipment
- desalination plants
High Temperature Alloy Steels
Certain industrial systems require studs capable of operating at elevated temperatures exceeding 500°C.
Typical alloys include:
| Grade | Composition | Use |
|---|---|---|
| F11 | Cr-Mo alloy | Steam piping |
| F22 | Cr-Mo alloy | Boilers |
| F91 | High-temperature alloy | Power plant turbines |
These materials maintain strength and creep resistance at elevated temperatures.
Material Comparison Table
| Grade | Yield Strength | Tensile Strength | Temperature Range | Corrosion Resistance | Typical Industry Use |
|---|---|---|---|---|---|
| ASTM A193 B7 | ~720 MPa | ~860 MPa | -29°C to 425°C | Moderate | Pressure equipment |
| ASTM A193 B16 | ~860 MPa | ~965 MPa | Up to 540°C | Moderate | High temperature systems |
| ASTM A320 L7 | ~720 MPa | ~860 MPa | Down to -101°C | Moderate | Cryogenic pipelines |
| ASTM A193 B8 | ~205 MPa | ~515 MPa | Up to 400°C | High | Chemical plants |
| ASTM A193 B8M | ~205 MPa | ~515 MPa | Up to 450°C | High | Marine environments |
| Duplex F51 | ~450 MPa | ~620 MPa | Up to 300°C | Very High | Offshore equipment |
| Super Duplex F55 | ~550 MPa | ~750 MPa | Up to 300°C | Excellent | Seawater systems |
6. Heat Treatment Information
Heat treatment processes are applied to improve the mechanical properties and structural integrity of Double End Studs.
These processes control:
- microstructure
- hardness
- tensile strength
- fatigue resistance
Normalizing
Normalizing involves heating the steel above its critical temperature followed by controlled air cooling.
Benefits include:
- grain refinement
- improved machinability
- uniform microstructure
This process is commonly applied to carbon steel studs.
Quenching and Tempering
Quenching and tempering is widely used for alloy steel studs such as ASTM A193 B7.
Process steps include:
- Heating steel above transformation temperature
- Rapid quenching in oil or water
- Tempering at controlled temperature
This produces:
- high tensile strength
- improved toughness
- controlled hardness
Stress Relieving
Stress relieving is applied after machining operations to remove residual stresses created during thread cutting or rolling.
Benefits include:
- dimensional stability
- reduced distortion
- improved fatigue life
Solution Annealing (Stainless Steel)
Stainless steel studs undergo solution annealing.
Process steps:
- Heating to ~1050°C
- Rapid cooling
Effects include:
- dissolution of carbides
- restoration of corrosion resistance
- improved ductility
Charpy Impact Testing
Low-temperature studs must demonstrate adequate toughness.
Charpy impact testing measures:
- energy absorbed during fracture
- ductile-to-brittle transition behavior
ASTM A320 studs are commonly tested using this method.
7. Manufacturing Process of Double End Studs
Manufacturing double end studs requires strict dimensional control and metallurgical verification to ensure reliable performance in industrial assemblies.
The typical production process includes the following steps.
1. Raw Material Inspection
Incoming steel bars are inspected for:
- chemical composition
- mechanical properties
- surface defects
Material traceability begins at this stage.
2. Bar Cutting
Steel bars are cut to required lengths using:
- band saws
- CNC cutting machines
Cut length accounts for:
- thread length
- chamfer allowance
3. CNC Turning
Precision turning operations produce:
- accurate stud diameter
- smooth surface finish
- chamfered thread entry
4. Thread Rolling or Thread Cutting
Two thread manufacturing methods are used.
Thread Rolling
Cold forming process that compresses material to create threads.
Advantages:
- improved surface finish
- increased fatigue strength
- work-hardened thread surface
Thread Cutting
Machining process used for:
- large diameter studs
- hardened materials
- special thread forms
5. Heat Treatment
After thread production, studs undergo heat treatment depending on material grade.
Processes include:
- quenching and tempering
- normalizing
- solution annealing
6. Surface Finishing
Surface treatment may include:
- black oxide coating
- phosphating
- galvanizing
These finishes improve corrosion resistance.
7. Straightness Correction
Long studs may undergo straightening operations to maintain axial alignment and dimensional accuracy.
8. Dimensional Inspection
Each production batch undergoes:
- thread gauge inspection
- length verification
- straightness measurement
9. Marking & Traceability
Studs are marked according to standards.
Typical markings include:
- material grade
- manufacturer identification
- heat number
Traceability is maintained through manufacturing records.
10. Final Packaging
Finished studs are packaged to prevent:
- corrosion
- mechanical damage
- thread deformation
Packaging methods include:
- oil wrapping
- export-grade wooden crates
- sealed containers
Dimensional Control Discipline
Manufacturers supplying EPC projects maintain strict control over:
- thread pitch accuracy
- stud straightness
- concentricity
- dimensional tolerances
8.Engineering Design Data for Double End Studs
Mechanical fasteners used in heavy industrial assemblies must be selected using quantifiable engineering data rather than generic dimensional information. For Double End Studs, design parameters include:
- stud diameter
- thread pitch
- engagement depth
- tensile capacity
- torque values
- preload forces
These parameters ensure that the stud maintains adequate clamping force without exceeding material stress limits.
The following sections present reference engineering tables and calculation guidelines commonly used by mechanical engineers, EPC contractors, and inspection agencies when specifying stud fasteners.
A. Technical Dimension Tables
Dimensional selection of Double End Studs depends on equipment geometry, flange thickness, and required thread engagement.
The following table provides typical dimensional guidelines used in heavy mechanical assemblies.
| Stud Diameter | Thread Pitch | Typical Stud Length Range | Thread Length (Each End) | Recommended Nut Size |
|---|---|---|---|---|
| M10 | 1.5 mm | 40 – 120 mm | 20 – 30 mm | M10 Hex Nut |
| M12 | 1.75 mm | 50 – 150 mm | 25 – 35 mm | M12 Hex Nut |
| M16 | 2.0 mm | 60 – 200 mm | 30 – 40 mm | M16 Heavy Hex Nut |
| M20 | 2.5 mm | 80 – 250 mm | 35 – 50 mm | M20 Heavy Hex Nut |
| M24 | 3.0 mm | 100 – 300 mm | 40 – 60 mm | M24 Heavy Hex Nut |
| M30 | 3.5 mm | 120 – 400 mm | 50 – 70 mm | M30 Heavy Hex Nut |
| M36 | 4.0 mm | 150 – 500 mm | 60 – 80 mm | M36 Heavy Hex Nut |
These values are commonly used in:
- turbine housings
- pressure vessel covers
- large equipment assemblies
Actual dimensions are determined by:
- equipment thickness
- gasket compression requirements
- design load capacity
Thread Engagement Guidelines
To prevent thread stripping in the base component, sufficient engagement depth must be provided.
Typical engineering practice:
Minimum thread engagement = 1 × stud diameter
For softer materials such as aluminum or cast iron, engagement may increase to:
1.5 × stud diameter
This ensures the shear strength of engaged threads exceeds the tensile capacity of the stud.
B. Mechanical Property Table
Mechanical properties of studs are defined by material standards such as ASTM A193 and ISO 898.
The following table presents typical values used for engineering design.
| Material Grade | Yield Strength | Tensile Strength | Elongation | Hardness | Impact Values |
|---|---|---|---|---|---|
| ASTM A193 B7 | ~720 MPa | ~860 MPa | 16% | 248–321 HB | Moderate |
| ASTM A193 B16 | ~860 MPa | ~965 MPa | 14% | 285–352 HB | Moderate |
| ASTM A320 L7 | ~720 MPa | ~860 MPa | 16% | 248–321 HB | High at low temp |
| ASTM A193 B8 | ~205 MPa | ~515 MPa | 30% | 95 HRB | Good |
| ASTM A193 B8M | ~205 MPa | ~515 MPa | 30% | 95 HRB | Excellent corrosion |
| Duplex F51 | ~450 MPa | ~620 MPa | 25% | 270 HB | High |
| Super Duplex F55 | ~550 MPa | ~750 MPa | 25% | 300 HB | Very High |
These values are used when calculating:
- allowable preload
- safety factors
- maximum joint load capacity
C. Torque Chart for Double End Studs
Torque values must be carefully selected to produce sufficient preload without exceeding yield strength.
Torque values depend on:
- stud diameter
- thread pitch
- lubrication condition
- material grade
The following chart presents typical torque values used in engineering practice.
Torque Chart (Reference Values)
| Stud Diameter | Thread Pitch | Dry Torque (B7) | Lubricated Torque (B7) | Dry Torque (Class 8.8) | Dry Torque (Class 10.9) |
|---|---|---|---|---|---|
| M12 | 1.75 | 70 Nm | 50 Nm | 75 Nm | 105 Nm |
| M16 | 2.0 | 170 Nm | 120 Nm | 180 Nm | 250 Nm |
| M20 | 2.5 | 340 Nm | 240 Nm | 360 Nm | 500 Nm |
| M24 | 3.0 | 580 Nm | 420 Nm | 600 Nm | 830 Nm |
| M30 | 3.5 | 1150 Nm | 820 Nm | 1200 Nm | 1650 Nm |
| M36 | 4.0 | 2000 Nm | 1450 Nm | 2100 Nm | 2900 Nm |
These values assume:
- standard thread friction
- hardened washers or nut faces
- uniform tightening conditions
Actual torque requirements may vary based on:
- lubrication condition
- gasket compression
- joint stiffness
D. Preload Calculation Guide
The purpose of tightening a stud is to create preload, which clamps the joint components together.
The preload force must be sufficient to prevent joint separation during service loads.
Torque–Tension Relationship
The relationship between torque and stud tension is commonly expressed as:

Where:
T = tightening torque
K = torque coefficient
F = preload force
D = nominal stud diameter
Typical torque coefficient values:
| Condition | K Value |
|---|---|
| Dry threads | 0.20 – 0.25 |
| Lubricated threads | 0.15 – 0.18 |
Bolt Preload Formula
Preload can also be estimated from allowable stress levels.

Where:
σ = tensile stress in stud
F = preload force
A = tensile stress area of the thread
Engineering practice typically limits preload to 60–75% of the yield strength.
Example Engineering Calculation
Consider:
Stud Diameter = M20
Material Grade = ASTM A193 B7
Yield Strength = 720 MPa
Approximate tensile stress area:
A ≈ 245 mm²
Allowable preload:
60% of yield stress.
Calculation:
F = 0.6 × σ × A
Result:
F ≈ 0.6 × 720 × 245
Stress vs Load Capacity Concept
The tensile load capacity of a stud depends on its stress area and material strength.
For example:
| Stud Diameter | Tensile Stress Area | Yield Strength (B7) | Approx Load Capacity |
|---|---|---|---|
| M12 | 84 mm² | 720 MPa | ~60 kN |
| M16 | 157 mm² | 720 MPa | ~113 kN |
| M20 | 245 mm² | 720 MPa | ~176 kN |
| M24 | 353 mm² | 720 MPa | ~254 kN |
| M30 | 561 mm² | 720 MPa | ~403 kN |
These values provide engineers with an estimate of maximum allowable loading.
F. Corrosion Resistance Comparison Table
Environmental conditions significantly influence stud material selection.
The following table compares corrosion performance of common materials.
| Material | Marine Environment | Acidic Conditions | High Humidity | Hydrocarbon Exposure |
|---|---|---|---|---|
| Carbon Steel | Low | Low | Moderate | Good |
| Stainless Steel 304 | Moderate | Moderate | High | Good |
| Stainless Steel 316 | High | High | High | Good |
| Duplex Stainless | Very High | Very High | Very High | Excellent |
| Alloy Steel | Low | Low | Moderate | Excellent |
Proper material selection prevents:
- corrosion-induced weakening
- stress corrosion cracking
- thread seizure
Inspection & Quality Control Methods
Quality assurance of Double End Studs is critical for industrial installations where mechanical failure can lead to equipment downtime or safety hazards.
Inspection procedures verify:
- material integrity
- dimensional accuracy
- mechanical properties
Positive Material Identification (PMI)
PMI testing confirms the chemical composition of the material using spectroscopic analysis.
This ensures compliance with specified material grades such as:
- ASTM A193 B7
- ASTM A320 L7
- stainless steel grades
Ultrasonic Testing (UT)
Ultrasonic inspection detects internal defects such as:
- inclusions
- voids
- internal cracks
This method is particularly important for large diameter studs used in critical equipment.
Magnetic Particle Inspection (MPI)
MPI detects surface and near-surface cracks in ferromagnetic materials.
It is widely used after heat treatment and machining operations.
Dye Penetrant Inspection (DPI)
Dye penetrant inspection identifies surface defects in non-magnetic materials such as stainless steel.
Hardness Testing
Hardness tests verify that heat treatment has produced the required mechanical properties.
Common methods include:
- Rockwell hardness testing
- Brinell hardness testing
Thread Gauge Inspection
Thread accuracy is verified using:
- GO gauges
- NO-GO gauges
This ensures that threads comply with specified tolerance classes.
Dimensional Inspection
Dimensional checks verify:
- overall length
- thread length
- diameter tolerances
- straightness
Precision measurement tools include:
- micrometers
- vernier calipers
- thread micrometers
9.Documentation & Certification
Industrial fasteners supplied for EPC projects typically require certification according to EN 10204 standards.
EN 10204 3.1 Certification
Provides:
- material test reports
- chemical analysis
- mechanical property results
Issued by the manufacturer.
EN 10204 3.2 Certification
Provides independent verification from:
- third-party inspection agencies
- client-authorized inspectors
This level of documentation is commonly required for pressure equipment projects.
Third-Party Inspection (TPI)
Major projects may require inspection by independent agencies such as:
- Lloyd’s Register
- Bureau Veritas
- TÜV
- DNV
These inspectors verify:
- raw material traceability
- heat treatment records
- dimensional compliance
- testing results
10. Industries Served
Double End Studs are widely used across heavy industrial sectors where high-strength threaded fastening systems are required for machinery assemblies, pressure equipment, and structural components.
In these sectors, studs are preferred because they provide stable thread engagement, repeatable preload conditions, and protection of internal threads in expensive equipment components.
The following industries commonly specify Double End Studs as part of their mechanical fastening systems.
Oil & Gas Upstream Facilities
Exploration and production facilities contain numerous mechanical systems operating under high pressure, vibration, and cyclic loads. Double end studs are used extensively in these installations to secure equipment components while allowing maintenance access.
Typical applications include:
- wellhead equipment assemblies
- compressor housings
- drilling machinery components
- separator vessels
- pump station equipment
Stud fastening systems are used because they allow disassembly without damaging tapped equipment threads, which is critical in remote installations where equipment repair options are limited.
Refineries
Refining operations involve equipment operating at elevated temperatures and high pressures. In such environments, fasteners must maintain stable preload despite thermal cycling and vibration.
Double End Studs are used in:
- distillation column covers
- reactor vessel assemblies
- heat exchanger housings
- pump casings
- rotating machinery frames
These assemblies require studs capable of maintaining clamping force under thermal expansion conditions.
Power Generation Plants
Power plants contain equipment subjected to high temperature steam systems and dynamic mechanical loads. Stud fasteners are used in components requiring periodic inspection or replacement.
Typical power plant applications include:
- steam turbine casings
- generator housings
- boiler inspection covers
- pressure piping systems
- high-temperature equipment enclosures
In these applications, double end studs allow controlled torque application during maintenance shutdowns.
Petrochemical Plants
Petrochemical processing units involve equipment exposed to corrosive chemicals, hydrocarbon vapors, and elevated temperatures.
Studs manufactured from stainless steel or corrosion-resistant alloys are commonly used in:
- catalytic cracking reactors
- chemical processing equipment
- piping manifolds
- pump assemblies
Material selection in these environments is often governed by corrosion resistance and chemical compatibility.
Hydrogen Processing Plants
Hydrogen production systems impose stringent requirements on mechanical fasteners due to:
- high operating pressure
- hydrogen embrittlement risks
- elevated temperatures
Double End Studs used in hydrogen service must meet strict material selection and testing criteria.
Common applications include:
- hydrogen reformers
- compressor systems
- pressure containment equipment
Steel Manufacturing Facilities
Heavy equipment used in steel plants operates under extreme mechanical loads and continuous vibration.
Double End Studs are used in:
- rolling mill housings
- furnace equipment
- heavy gear assemblies
- structural machinery components
Stud-based fastening systems simplify maintenance operations in large industrial machinery.
Infrastructure Equipment & Heavy Engineering Plants
Large fabrication plants and infrastructure machinery rely on stud fasteners for structural assemblies and equipment installation.
Applications include:
- bridge machinery systems
- construction equipment frames
- large structural supports
- heavy fabrication machinery
Stud installation allows equipment components to be secured while maintaining serviceability during equipment life cycles.
11. Export Capability & Global Supply
Industrial fasteners used in large-scale engineering projects must meet international documentation, packaging, and logistics requirements.
Manufacturers supplying Double End Studs for global projects must demonstrate the ability to support export-grade manufacturing and project supply logistics.
Super Industries supplies Double End Studs for international projects requiring compliance with global engineering standards and procurement procedures.
Regions Served
Industrial fasteners are exported to engineering contractors and equipment manufacturers in several regions.
United States
Fasteners supplied to the United States typically comply with:
- ASTM material specifications
- ASME thread standards
- project-specific engineering requirements
These studs are used in oil refineries, power plants, and heavy industrial equipment.
European Union
European projects often require compliance with:
- DIN dimensional standards
- ISO mechanical property standards
- EN certification documentation
Stud fasteners supplied to European markets must also meet traceability and inspection documentation requirements.
Middle East
Energy infrastructure projects in the Middle East require large volumes of high-strength fasteners for:
- oil production facilities
- petrochemical plants
- pipeline infrastructure
- refinery equipment
Double End Studs used in these projects often require third-party inspection and detailed material certification.
Southeast Asia
Industrial development across Southeast Asia has increased demand for fasteners used in:
- power generation plants
- petrochemical facilities
- heavy engineering projects
Export shipments must comply with regional engineering standards and shipping documentation requirements.
Export Packaging Standards
Export shipments of Double End Studs must be protected against corrosion and mechanical damage during transportation.
Typical export packaging includes:
- rust preventive oil coating
- moisture-resistant wrapping
- sealed plastic packaging for stainless steel studs
- wooden crates for large orders
Proper packaging prevents:
- thread damage
- corrosion during transit
- mechanical deformation
Documentation for International Supply
Project shipments generally require the following documentation:
- material test certificates
- dimensional inspection reports
- heat treatment records
- packing lists
- export declarations
These documents support customs clearance and project inspection procedures.
Procurement & Installation View
Engineers and procurement teams specifying Double End Studs must consider several installation and handling factors to ensure reliable joint performance.
Stud Installation Methods
Correct installation of studs ensures that the stud remains securely seated in the base component while allowing proper tightening of the external nut.
Two commonly used installation methods are described below.
Double Nut Method
This method uses two nuts temporarily threaded onto the exposed end of the stud.
Procedure:
- Thread the stud into the base component.
- Install two nuts on the exposed end.
- Tighten the nuts against each other to lock them together.
- Use a wrench to rotate the stud into position.
- Remove the nuts after installation.
This method prevents damage to the exposed threads.
Stud Driver Tools
Stud driver tools are specialized devices designed for installing studs without damaging the threads.
Advantages include:
- faster installation
- reduced thread damage
- improved alignment during assembly
These tools are commonly used in production assembly environments.
Torque Tightening Sequence
When multiple studs are used to clamp large components, tightening must follow a controlled sequence to ensure uniform load distribution.
Typical tightening practice includes:
- Initial snug tightening
- Sequential tightening using a cross-pattern
- Final torque application
This approach prevents uneven gasket compression and joint distortion.
Lubrication During Installation
Lubrication improves torque accuracy and prevents thread galling.
Common lubricants include:
- molybdenum disulfide compounds
- anti-seize lubricants
- graphite-based compounds
Lubrication is particularly important for:
- stainless steel studs
- high temperature fasteners
Re-Torque Requirements
Certain assemblies require re-torque after initial installation.
Reasons include:
- gasket compression relaxation
- thermal expansion effects
- settlement of joint components
Maintenance procedures often include re-checking torque values after equipment startup.
Field Inspection Checklist
Before commissioning mechanical assemblies using Double End Studs, inspection teams typically verify:
- stud material grade markings
- correct stud length
- proper thread engagement depth
- correct torque values applied
- lubrication conditions
Inspection ensures that the fastening system meets project specifications and engineering requirements.
Storage & Handling Discipline
Proper storage prevents corrosion and mechanical damage to stud threads.
Recommended storage practices include:
- indoor dry storage conditions
- sealed packaging for stainless steel studs
- separation by material grade and size
- application of rust-preventive oil for carbon steel studs
Studs should remain in protective packaging until installation to maintain thread integrity.
Custom Engineering Capabilities
Industrial equipment manufacturers frequently require non-standard stud configurations based on equipment geometry or project requirements.
Manufacturers supplying EPC projects must therefore support custom engineering requirements.
Non-Standard Stud Lengths
Custom stud lengths may be required for:
- thick equipment flanges
- pressure vessel covers
- specialized machinery assemblies
Special Thread Forms
Certain equipment requires specialized thread profiles including:
- fine pitch threads
- custom tolerance classes
- non-standard thread engagement lengths
Large Diameter Studs
Heavy equipment may require studs exceeding standard diameter ranges.
Large diameter studs are commonly used in:
- turbine housings
- large compressors
- pressure vessel assemblies
High Temperature Alloy Studs
For equipment operating at elevated temperatures, studs may be manufactured from high-temperature alloy steels such as chromium-molybdenum alloys.
These materials provide:
- creep resistance
- thermal stability
- high-temperature strength
Project-Specific Marking
Project documentation may require custom marking that includes:
- material grade
- heat number
- manufacturer identification
- project reference numbers
Traceability marking supports inspection and quality verification during project audits.
Engineering Summary
Double End Studs are a critical component of mechanical fastening systems used in heavy industrial equipment.
Their design allows:
- permanent thread engagement within base components
- controlled preload through external nut tightening
- repeated assembly and disassembly without damaging equipment threads
For engineering applications, proper selection of studs requires evaluation of:
- material grade
- thread dimensions
- preload requirements
- operating temperature
- environmental exposure
Compliance with ASTM, ASME, DIN, and ISO standards ensures that studs meet the mechanical and dimensional requirements necessary for safe operation in industrial systems.
Manufacturing processes must maintain strict dimensional control, heat treatment verification, and inspection documentation to meet the expectations of EPC contractors and third-party inspection agencies.
When correctly selected, installed, and maintained, Double End Studs provide reliable fastening performance in applications ranging from pressure vessels and turbines to heavy machinery and structural assemblies.