FORGED FLANGES
“Global Manufacturer of Heavy & Custom Engineered Fasteners for Oil & Gas, Power & EPC Contractors.”
1. Industry Context & System Relevance
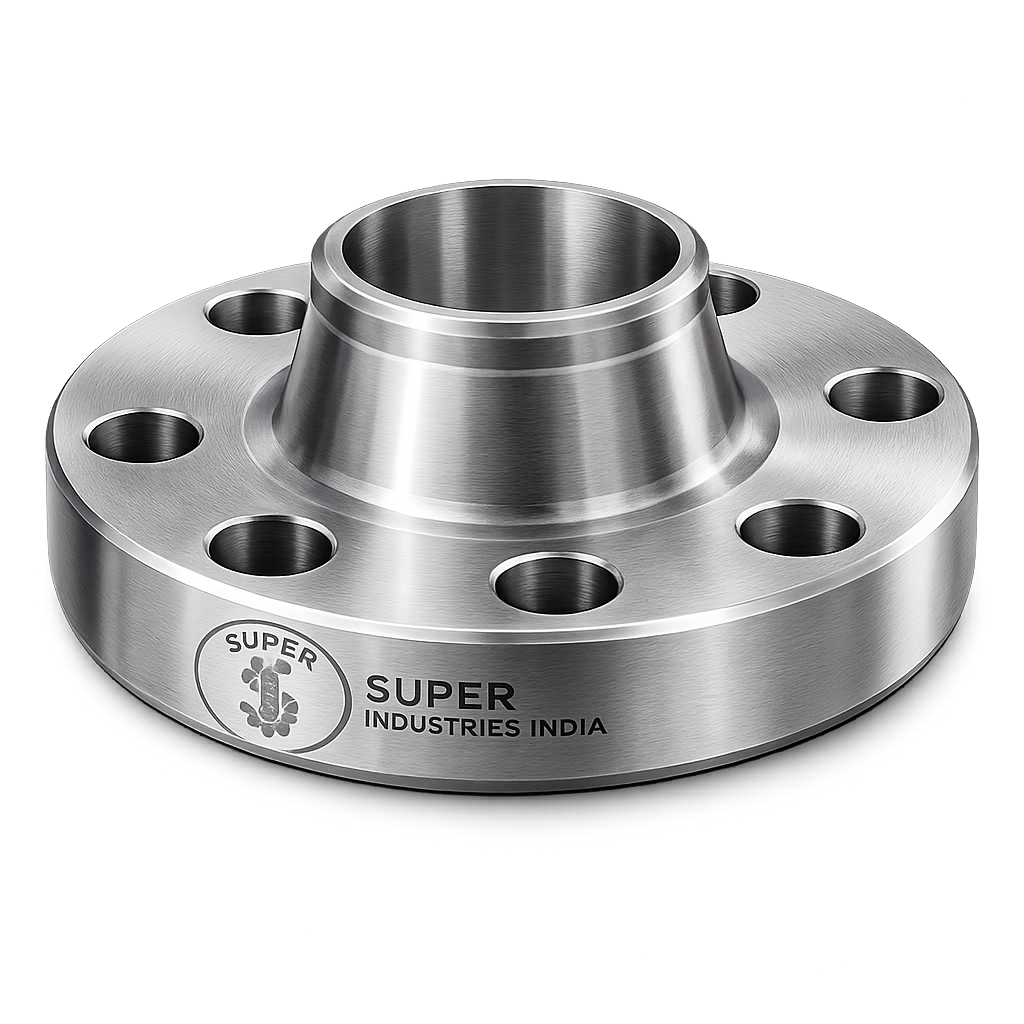
Forged Flanges are fundamental pressure-boundary components used in engineered piping systems where controlled assembly, disassembly, and inspection access are mandatory. Their application spans across high-integrity industrial environments where pressure containment, leak prevention, and maintenance accessibility must be simultaneously achieved.
Role in Pressure Piping Systems
In pressure piping systems, Forged Flanges function as detachable mechanical joints that connect:
- Pipe-to-pipe interfaces
- Pipe-to-valve connections
- Pipe-to-equipment nozzles
- Pipe-to-instrumentation assemblies
Unlike permanent welded joints, flange assemblies provide a bolted and gasketed interface that allows:
- Controlled compression sealing
- Periodic inspection
- Replacement of internal components
- Isolation for maintenance
Application Across Industrial Sectors
Refinery & Petrochemical Systems
- High-pressure hydrocarbon processing lines
- Crude distillation units
- Catalytic cracking systems
- Hydrogen service lines
Flanged joints are used where frequent inspection or catalyst replacement is required.
Power Generation Plants
- Main steam lines
- Boiler feedwater systems
- Turbine inlet/outlet connections
High-pressure and high-temperature conditions necessitate flanges with controlled metallurgy and predictable sealing performance.
LNG & Cryogenic Systems
- Liquefaction trains
- Cryogenic transfer lines
- Storage tank connections
Forged Flanges in these systems require materials with low-temperature toughness and resistance to brittle fracture.
Offshore Platforms
- Subsea and topside piping
- High-pressure riser systems
- Injection lines
Flanges are selected for their ability to accommodate installation constraints and allow disassembly in constrained offshore environments.
Process & Chemical Plants
- Acidic and corrosive service lines
- Multi-phase flow systems
- Reactor feed and discharge piping
Material selection and gasket compatibility are critical in such environments.
Selection Over Welded and Threaded Systems
Compared to Welded Joints
| Parameter | Welded Joint | Forged Flange Joint |
|---|---|---|
| Permanence | Permanent | Removable |
| Inspection Access | Limited | Full access |
| Maintenance | Requires cutting | Simple disassembly |
| Leak Control | Dependent on weld integrity | Controlled via gasket compression |
Forged Flanges are selected where:
- Periodic maintenance is expected
- Internal inspection is required
- Equipment replacement cycles are defined
Compared to Threaded Systems
| Parameter | Threaded Joint | Forged Flange Joint |
|---|---|---|
| Pressure Capability | Limited | High pressure capable |
| Sealing Mechanism | Thread interference | Gasket compression |
| Leakage Risk | Higher under vibration | Controlled under preload |
| Size Limitation | Small bore | Full range (NPS ½” to 60”+) |
Flanged joints are preferred in:
- High-pressure applications
- High-temperature systems
- Critical service environments
Functional Advantages of Forged Flanges
- Maintainability: Enables repeated assembly/disassembly without material degradation
- Inspection Accessibility: Allows internal pipeline inspection and gasket replacement
- Controlled Sealing: Bolt preload ensures predictable gasket compression
- Alignment Flexibility: Facilitates alignment adjustments during installation
- System Integrity: Supports pressure containment under cyclic and thermal loads
Super Industries
Global Manufacturer of Heavy & Custom Engineered Fasteners & Flanges
2. Technical Definition of Forged Flanges
Forged Flanges are pressure-retaining mechanical components manufactured through controlled forging processes, designed to connect piping elements via bolted joints and gasket-sealed interfaces.
Core Functional Definition
A Forged Flange is:
- A forged metallic ring with machined sealing surfaces
- Designed to transfer bolt load into gasket compression
- Used to create a leak-tight joint under internal pressure
- Engineered to withstand:
- Internal pressure
- External piping loads
- Thermal expansion stresses
Forging Advantage (Grain Flow Control)
Unlike cast or plate-cut flanges, forged flanges exhibit:
- Directional grain flow aligned with stress paths
- Reduced internal defects (voids, inclusions)
- Improved fatigue resistance
- Enhanced mechanical strength
This makes them suitable for:
- High-pressure systems
- Cyclic loading conditions
- Critical service applications
Primary Types of Forged Flanges
Weld Neck Flange (WN)
- Long tapered hub
- Butt-welded to pipe
- Provides smooth stress transition
- Preferred for high-pressure and cyclic service
Slip-On Flange (SO)
- Slides over pipe
- Fillet welded (inside and outside)
- Used in moderate pressure systems
Blind Flange (BL)
- Solid disc
- Used to close pipeline ends
- Withstands full system pressure
Socket Weld Flange (SW)
- Socket connection for small bore piping
- Internal shoulder for pipe seating
- Used in high-pressure small diameter systems
Threaded Flange (TH)
- Internal threads
- No welding required
- Used in low-pressure or hazardous environments where welding is restricted
Lap Joint Flange (LJ)
- Used with stub end
- Allows rotational alignment
- Suitable for systems requiring frequent dismantling
Long Weld Neck (LWN)
- Extended hub
- Used for pressure vessels and special applications
- Designed for high stress concentration areas
Flange Facing Types
Raised Face (RF)
- Most commonly used
- Concentrates gasket load
- Suitable for soft gasket sealing
Ring Type Joint (RTJ)
- Metal-to-metal sealing
- Uses metallic ring gasket
- Designed for high-pressure, high-temperature service
Flat Face (FF)
- Entire face is flat
- Used with non-metallic piping systems (e.g., cast iron)
- Prevents flange damage due to uneven loading
3. Engineering & Sealing Principle
The sealing performance of Forged Flanges is governed by the interaction between:
- Bolt preload
- Gasket compression
- Flange rigidity
- Internal pressure forces
Bolt Preload Mechanics
Bolts are tensioned during installation to create preload force, which:
- Compresses the gasket
- Generates sealing stress
- Maintains joint integrity under pressure
Key Concept:
Bolt load must exceed the force generated by internal pressure attempting to separate the joint.
Gasket Compression Theory
Gaskets act as deformable elements that:
- Fill surface irregularities
- Create a seal under compressive stress
Two key parameters define gasket behavior:
m Factor (Maintenance Factor)
- Represents gasket’s ability to maintain seal under pressure
- Used in flange design calculations
y Factor (Seating Stress)
- Minimum stress required to seat the gasket initially
Sealing Stress vs Internal Pressure
For leak-tight performance:
- Initial gasket seating stress must exceed y factor
- Operating stress must satisfy m × internal pressure
Failure to maintain this balance leads to:
- Leakage
- Gasket blowout
- Joint separation
Flange Rotation Under Load
Under bolt preload and internal pressure:
- Flange faces tend to rotate outward
- This reduces gasket compression at the inner diameter
Design considerations include:
- Flange thickness
- Hub geometry (in WN flanges)
- Bolt distribution
Bolt Relaxation Behavior
Over time, bolt preload may reduce due to:
- Gasket creep
- Thermal cycling
- Material relaxation
This leads to:
- Reduced sealing stress
- Increased leakage risk
Mitigation:
- Controlled tightening procedures
- Re-torque practices
- Selection of appropriate gasket material
RTJ vs Soft Gasket Sealing
RTJ Sealing (Metallic)
- Metal-to-metal contact
- High seating stress
- Suitable for extreme pressure and temperature
Advantages:
- Minimal creep
- High integrity sealing
Soft Gasket Sealing
- Uses materials like graphite, PTFE
- Requires controlled compression
Advantages:
- Better conformity
- Suitable for lower pressure applications
Surface Finish Requirements
Flange face finish directly affects sealing performance.
Typical roughness:
- 125–250 AARH (3.2–6.3 µm Ra) for RF flanges
Too smooth:
- Reduces gasket grip
Too rough:
- Causes leakage paths
RTJ grooves require:
- Precision machining
- Tight tolerances
- Controlled surface finish
Leakage Prevention Mechanism
Leakage is prevented when:
- Bolt preload ≥ internal separating force
- Gasket stress ≥ minimum required sealing stress
- Flange deformation remains within allowable limits
Engineering control involves:
- Proper flange selection (class & type)
- Correct gasket specification
- Accurate bolt torque application
Summary of Sealing System Behavior
| Component | Function |
|---|---|
| Bolts | Provide preload force |
| Flange | Transfers load to gasket |
| Gasket | Creates seal |
| Internal Pressure | Attempts to separate joint |
A stable flange joint is achieved when:
- Load distribution is uniform
- Material properties are within specified limits
- Installation practices follow defined torque procedures
4. Applicable Standards (ASME / ASTM / DIN / EN / ISO)
Forged Flanges are governed by internationally accepted dimensional, material, and inspection standards. Compliance ensures interchangeability, pressure integrity, and acceptance in EPC projects.
ASME Dimensional Standards
ASME B16.5
Covers:
- NPS ½” to 24”
- Pressure Classes: 150 to 2500
- Dimensions:
- Outside diameter (OD)
- Bolt circle diameter (BCD)
- Flange thickness
- Facing dimensions (RF, RTJ, FF)
Application:
- Oil & Gas piping
- Refineries
- Power plants
- General process piping
ASME B16.47 Series A & B
Covers:
- NPS 26” to 60”
Series A:
- Larger bolt circle
- Higher strength design
- Used in critical services
Series B:
- Smaller bolt circle
- Economical
- Used in less critical applications
ASTM Material Standards
Material standards define:
- Chemical composition
- Mechanical properties
- Heat treatment conditions
Common standards:
- ASTM A105 → Carbon steel forged flanges
- ASTM A350 LF2 → Low-temperature carbon steel
- ASTM A182 → Stainless & alloy steel forged flanges
European Standards (DIN / EN)
DIN EN 1092-1
Defines:
- PN pressure ratings (PN6 to PN100+)
- Metric-based flange dimensions
- Facing types and tolerances
Application:
- European EPC projects
- Chemical and water systems
ISO Flange Systems
ISO standards provide:
- Global harmonization
- Interchangeability between regions
- Standardized pressure-temperature relationships
Standards Mapping
| Standard | Coverage | Pressure Range | Typical Application |
|---|---|---|---|
| ASME B16.5 | NPS ≤ 24” | Class 150–2500 | Oil & Gas, Power |
| ASME B16.47 | NPS 26”–60” | High pressure | Pipelines, offshore |
| ASTM A105 | Material | Moderate temp | General piping |
| ASTM A350 LF2 | Material | Low temp | Cryogenic systems |
| ASTM A182 | Material | High temp/corrosion | Refinery, chemical |
| EN 1092-1 | Metric flanges | PN rated | EU projects |
| ISO | Global | Varies | International projects |
5. Material & Grade Options
Material selection for Forged Flanges is driven by:
- Operating pressure and temperature
- Corrosive environment
- Mechanical loading conditions
- Project specifications
Carbon Steel Forged Flanges
ASTM A105
- Standard carbon steel forging grade
- Suitable for ambient to moderate temperature service
ASTM A350 LF2
- Designed for low-temperature service
- Improved impact toughness
- Used in sub-zero applications
Stainless Steel Forged Flanges
ASTM A182 F304
- Austenitic stainless steel
- General corrosion resistance
ASTM A182 F316
- Contains molybdenum
- Enhanced resistance to chlorides and chemicals
Alloy Steel Forged Flanges
ASTM A182 F11
- Chromium-molybdenum alloy
- Suitable for elevated temperature service
ASTM A182 F22
- Higher strength than F11
- Used in high-pressure and high-temperature systems
Duplex & Super Duplex Grades
ASTM A182 F51 (Duplex)
- Dual-phase microstructure
- High strength and corrosion resistance
ASTM A182 F53 (Super Duplex)
- Superior pitting and crevice corrosion resistance
- Used in offshore and marine environments
Material Property Table
| Grade | Yield Strength (MPa) | Tensile Strength (MPa) | Temperature Range | Corrosion Resistance | Typical Use |
|---|---|---|---|---|---|
| A105 | ≥ 250 | 485–620 | -29°C to 425°C | Low | General piping |
| A350 LF2 | ≥ 250 | 485–620 | -46°C to 345°C | Low | Low-temperature service |
| F304 | ≥ 205 | 515–720 | Up to 870°C | Moderate | Chemical processing |
| F316 | ≥ 205 | 515–720 | Up to 870°C | High | Marine, chemical |
| F11 | ≥ 275 | 415–585 | Up to 540°C | Moderate | Power plants |
| F22 | ≥ 415 | 585–760 | Up to 600°C | Moderate | High-pressure systems |
| F51 | ≥ 450 | 620–880 | -50°C to 300°C | High | Offshore |
| F53 | ≥ 550 | 750–950 | -50°C to 300°C | Very High | Marine, subsea |
6. Heat Treatment of Forged Flanges
Heat treatment is applied to achieve:
- Required mechanical properties
- Grain refinement
- Residual stress reduction
- Improved toughness
Normalizing
- Heating above critical temperature
- Air cooling
Effect:
- Refines grain structure
- Improves uniformity
- Enhances strength
Quenching & Tempering (Q&T)
- Rapid cooling (quenching)
- Followed by reheating (tempering)
Effect:
- Increases strength
- Improves toughness
- Reduces brittleness
Used for:
- Alloy steel grades (F11, F22)
Solution Annealing (Stainless Steel)
- Heating to high temperature
- Rapid quenching
Effect:
- Dissolves carbides
- Restores corrosion resistance
- Improves ductility
Stress Relieving
- Heating below transformation temperature
- Controlled cooling
Effect:
- Reduces residual stresses
- Prevents distortion during machining
Hardness & Microstructure Control
| Material | Typical Hardness (HB) | Microstructure |
|---|---|---|
| A105 | 120–180 | Ferrite-Pearlite |
| LF2 | 120–180 | Fine-grained ferrite |
| F11/F22 | 150–220 | Tempered martensite |
| SS304/316 | 150–200 | Austenitic |
| Duplex | 200–300 | Austenite + Ferrite |
Impact Testing (Charpy V-Notch)
Conducted for:
- Low-temperature applications
- Critical service conditions
Ensures:
- Resistance to brittle fracture
- Compliance with project specifications
7. Manufacturing Process of Forged Flanges
Forged Flanges are produced through a controlled sequence ensuring dimensional accuracy and metallurgical integrity.
Raw Material Inspection
- Verification of chemical composition
- Ultrasonic testing for internal defects
- Traceability through heat numbers
Cutting & Heating
- Billets cut to required size
- Heated in controlled furnaces
Temperature control is critical to:
- Avoid overheating
- Maintain metallurgical properties
Closed-Die Forging
- Material shaped using dies under high pressure
Results in:
- Controlled grain flow
- Dense structure
- Improved mechanical strength
Heat Treatment
Applied as per material grade:
- Normalizing
- Q&T
- Solution annealing
Ensures required mechanical properties.
CNC Machining
Precision machining operations include:
- Bore machining
- Hub profiling (WN flanges)
- Facing operations
Achieves:
- Tight tolerances
- Surface finish requirements
Facing & Drilling
- Machining of RF/RTJ/FF faces
- Drilling of bolt holes as per BCD
Accuracy is critical for:
- Proper bolt alignment
- Load distribution
RTJ Groove Machining
For RTJ flanges:
- Precision groove cutting
- Dimensional tolerance control
- Surface finish verification
Surface Finishing
- Removal of scale and burrs
- Application of protective coatings
Marking & Traceability
Each Forged Flange is marked with:
- Material grade
- Heat number
- Size and pressure class
- Manufacturer identification
Ensures:
- Full traceability
- Compliance with inspection requirements
Surface Finish Options
Surface protection and flange face finish are critical for storage, corrosion resistance, and sealing performance.
External Surface Coatings
Anti-Rust Oil Coating
- Temporary protection during storage and transport
Black Paint
- Protection against atmospheric corrosion
Galvanizing
- Zinc coating for corrosion resistance
- Used in water systems
PTFE Coating
- Chemical resistance
- Used in aggressive environments
Passivation (Stainless Steel)
- Enhances corrosion resistance
- Removes surface contaminants
Flange Face Finish
Critical for gasket sealing.
Typical finish:
- 125–250 AARH (3.2–6.3 µm Ra)
Types:
- Spiral serrated finish (standard RF)
- Smooth finish (special applications)
Surface Finish Impact
| Condition | Effect |
|---|---|
| Too Smooth | Poor gasket grip |
| Too Rough | Leakage paths |
| Controlled Finish | Optimal sealing |
RTJ Groove Finish
- Precision machined
- Low roughness
- Tight dimensional tolerances
Ensures:
- Metal-to-metal sealing integrity
A. Dimensional Reference Table (ASME B16.5 – Representative)
The following table provides indicative dimensions for commonly used Forged Flanges. Final dimensions must always be verified against the latest ASME standards and project specifications.
| NPS | Class | OD (mm) | BCD (mm) | Bolt Size | No. of Bolts | Thickness (mm) |
|---|---|---|---|---|---|---|
| 2” | 150 | 152 | 120.7 | M16 | 4 | 17.5 |
| 2” | 300 | 165 | 127 | M16 | 8 | 20.6 |
| 4” | 150 | 229 | 190.5 | M16 | 8 | 23.9 |
| 4” | 600 | 292 | 235 | M20 | 8 | 47.8 |
| 6” | 300 | 318 | 269.9 | M20 | 12 | 36.6 |
| 8” | 600 | 419 | 362 | M24 | 12 | 55.6 |
| 10” | 900 | 508 | 431.8 | M30 | 16 | 85.9 |
| 12” | 1500 | 584 | 482.6 | M33 | 16 | 117.3 |
Engineering Notes:
- Increase in pressure class results in increased thickness and bolt quantity
- Bolt Circle Diameter (BCD) governs load distribution
- Thickness is directly related to flange rigidity and rotation resistance
B. Pressure–Temperature Rating Table (Indicative)
Pressure ratings depend on material and temperature as defined in ASME B16.5.
| Class | Pressure (Bar) @ Ambient | Temperature (°C) | Material | Remarks |
|---|---|---|---|---|
| 150 | ~19 | Up to 200 | A105 | Low-pressure service |
| 300 | ~51 | Up to 200 | A105 | Moderate pressure |
| 600 | ~102 | Up to 200 | A105 | Process piping |
| 900 | ~153 | Up to 200 | A105 | High-pressure systems |
| 1500 | ~255 | Up to 200 | A105 | Critical service |
| 2500 | ~425 | Up to 200 | A105 | Extreme pressure |
Engineering Consideration:
- Pressure rating decreases as temperature increases
- Material grade selection is critical at elevated temperatures
C. Torque Chart for Bolting (Indicative Values)
Torque values are dependent on bolt size, lubrication condition, and friction coefficient. The following table provides engineering reference values.
| Bolt Size | Class | Torque (Nm) – Lubricated | Torque (Nm) – Dry |
|---|---|---|---|
| M16 | 150 | 70 | 100 |
| M16 | 300 | 110 | 150 |
| M20 | 300 | 210 | 280 |
| M20 | 600 | 320 | 420 |
| M24 | 600 | 550 | 720 |
| M24 | 900 | 720 | 950 |
| M30 | 900 | 1200 | 1550 |
| M33 | 1500 | 1800 | 2300 |
Torque Application Notes
- Lubricated bolts reduce friction → lower torque required
- Dry bolts increase torque variability
- Torque must be applied in controlled increments
- Use calibrated torque wrenches or hydraulic tensioners
D. Preload Calculation Guide
Proper bolt preload is essential to achieve leak-tight sealing.
1. Bolt Load Formula
Bolt preload force:

Where:
- ( F ) = Bolt preload force (N)
- ( \sigma_b ) = Bolt stress (MPa)
- ( A_b ) = Bolt tensile stress area (mm²)
2. Gasket Seating Load
Initial seating load:

Where:
- ( y ) = Gasket seating stress
- ( A_g ) = Effective gasket area
3. Operating Load Requirement
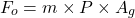
Where:
- ( m ) = Gasket factor
- ( P ) = Internal pressure
- ( A_g ) = Gasket area
4. Design Condition
For safe sealing:
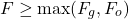
5. Sample Calculation
Given:
- Bolt size: M20
- Tensile stress area ( A_b = 245 , mm^2 )
- Bolt stress ( \sigma_b = 200 , MPa )
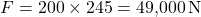
If:
- Gasket seating load = 35,000 N
- Operating load = 42,000 N
Then:
- Required load = 42,000 N
- Available bolt load = 49,000 N
Condition satisfied → Joint is safe
6. Safety Margin
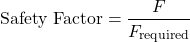
Recommended:
- Minimum safety factor: 1.2 to 1.5
E. Mechanical Property Table
| Material | Yield Strength (MPa) | Tensile Strength (MPa) | Elongation (%) | Hardness (HB) | Impact (J) |
|---|---|---|---|---|---|
| A105 | ≥ 250 | 485–620 | ≥ 20 | 120–180 | Moderate |
| LF2 | ≥ 250 | 485–620 | ≥ 22 | 120–180 | High (low temp) |
| F304 | ≥ 205 | 515–720 | ≥ 30 | 150–200 | High |
| F316 | ≥ 205 | 515–720 | ≥ 30 | 150–200 | High |
| F11 | ≥ 275 | 415–585 | ≥ 20 | 150–220 | Moderate |
| F22 | ≥ 415 | 585–760 | ≥ 18 | 170–220 | Moderate |
| F51 | ≥ 450 | 620–880 | ≥ 25 | 200–300 | High |
| F53 | ≥ 550 | 750–950 | ≥ 25 | 250–320 | High |
F. Corrosion Resistance Comparison Table
| Material | Marine | Acidic | High Temperature | Hydrocarbon |
|---|---|---|---|---|
| Carbon Steel (A105) | Low | Low | Moderate | High |
| SS304 | Moderate | Moderate | High | High |
| SS316 | High | High | High | High |
| Alloy Steel (F11/F22) | Low | Low | Very High | High |
| Duplex (F51) | Very High | High | Moderate | High |
| Super Duplex (F53) | Excellent | Very High | Moderate | High |
8. Inspection & Quality Control
Inspection of Forged Flanges ensures compliance with dimensional, material, and performance requirements.
Positive Material Identification (PMI)
- Verifies chemical composition
- Conducted using XRF or OES
- Ensures correct material grade
Ultrasonic Testing (UT)
- Detects internal discontinuities
- Identifies:
- Voids
- Inclusions
- Cracks
Magnetic Particle Inspection (MPI)
- Surface and near-surface defect detection
- Applicable for ferromagnetic materials
Dye Penetrant Testing (DPT)
- Detects surface cracks
- Used for stainless steel and non-magnetic materials
Dimensional Inspection
Verification of:
- OD, ID
- BCD
- Bolt hole alignment
- Thickness
- Facing dimensions
Hardness Testing
- Confirms heat treatment results
- Ensures compliance with material standards
Hydrostatic Testing (Assembly Level)
- Conducted on assembled flange joints
- Validates sealing performance under pressure
Documentation & Certification
EN 10204 Certification
- 3.1 Certificate: Manufacturer test certificate
- 3.2 Certificate: Third-party verified certificate
Includes:
- Chemical composition
- Mechanical properties
- Heat treatment details
- Test results
Third-Party Inspection (TPI)
Inspection agencies may include:
- Independent inspection bodies
- Client-appointed inspectors
- EPC consultant representatives
Scope includes:
- Stage inspection
- Final inspection
- Documentation review
Traceability System
Each Forged Flange is traceable through:
- Heat number
- Batch number
- Material certificate
Ensures:
- Full lifecycle traceability
- Compliance with EPC requirements
9. Industries Served
Forged Flanges are deployed across multiple industries where pressure containment, mechanical integrity, and inspection accessibility are critical.
Oil & Gas Sector
Upstream (Exploration & Production)
- Wellhead connections
- High-pressure injection lines
- Subsea flow systems
Requirements:
- High-pressure ratings (Class 900–2500)
- Corrosion-resistant materials (Duplex / Super Duplex)
- Fatigue resistance under cyclic loads
Midstream (Transportation)
- Pipeline booster stations
- Compressor stations
- Metering skid connections
Requirements:
- Large diameter flanges (ASME B16.47)
- Resistance to external loads and vibration
- Reliable sealing over long operational cycles
Downstream (Refining & Processing)
- Distillation columns
- Reactor piping
- Hydrogen service
Requirements:
- High-temperature alloy steels
- RTJ sealing for critical joints
- Resistance to chemical corrosion
Petrochemical Industry
- Polymer processing units
- Chemical reactors
- Solvent handling systems
Material selection focuses on:
- Stainless steel (F304 / F316)
- Chemical compatibility
- Corrosion resistance
Power Generation
Thermal Power Plants
- Boiler systems
- Main steam pipelines
- Turbine connections
Requirements:
- Alloy steel flanges (F11 / F22)
- Resistance to creep and thermal fatigue
Nuclear Power Systems
- High-integrity piping systems
- Safety-critical connections
Requirements:
- Strict dimensional tolerance
- Full traceability
- Third-party inspection compliance
LNG & Cryogenic Systems
- LNG liquefaction plants
- Storage tanks
- Transfer pipelines
Requirements:
- Low-temperature materials (ASTM A350 LF2, Duplex)
- Charpy impact-tested flanges
- Resistance to brittle fracture
Offshore & Marine
- Offshore platforms
- FPSO systems
- Seawater injection lines
Requirements:
- Super Duplex materials (F53)
- Resistance to chloride-induced corrosion
- High fatigue resistance
Hydrogen & Emerging Energy Systems
- Hydrogen pipelines
- Electrolyzer systems
- Carbon capture systems
Requirements:
- Material compatibility with hydrogen
- Resistance to hydrogen embrittlement
- High-integrity sealing systems
10. Export Capability & Global Supply
Super Industries supports international EPC and industrial projects with structured export and documentation systems.
Export Regions
- United States
- European Union
- Middle East (UAE, Saudi Arabia, Qatar)
- Southeast Asia (Singapore, Indonesia, Malaysia)
Packaging Standards
Forged Flanges are supplied in seaworthy export packaging:
- Wooden crates (fumigated)
- Palletized packaging
- Anti-corrosion wrapping
- Protective flange face covers
Purpose:
- Prevent mechanical damage
- Protect sealing surfaces
- Ensure corrosion resistance during transit
Documentation Package
Each shipment includes:
- Material Test Certificates (MTC – EN 10204 3.1 / 3.2)
- Dimensional inspection reports
- Heat treatment records
- NDT reports (UT, PMI, MPI/DPT)
- Compliance certificates (ASME / ASTM / EN)
Logistics & Project Execution Capability
- Bulk supply for EPC projects
- Lot-wise traceability
- Stage inspection coordination
- Delivery scheduling aligned with project timelines
11. Procurement & Installation View
Forged Flanges require controlled installation practices to ensure sealing integrity and long-term performance.
Gasket Installation
- Verify gasket type and rating
- Ensure clean and undamaged flange faces
- Proper centering of gasket
Bolt Tightening Sequence
Bolts must be tightened in a star (cross) pattern:
- Initial snug tightening
- 30% of final torque
- 60% of final torque
- 100% of final torque
- Final pass for uniformity
Purpose:
- Uniform load distribution
- Minimized flange distortion
- Consistent gasket compression
Torque Tightening Practices
- Use calibrated torque tools
- Apply lubrication where specified
- Avoid over-tightening
Re-Torque Practice
- Required after initial pressurization or thermal cycling
- Compensates for gasket creep and bolt relaxation
Inspection Checkpoints
Before commissioning:
- Bolt torque verification
- Alignment check
- Gasket integrity verification
- Leak testing
Storage & Handling
- Store in dry conditions
- Protect flange faces with covers
- Avoid stacking damage
12. Custom Engineering Capabilities
Super Industries supports project-specific requirements for Forged Flanges beyond standard specifications.
Non-Standard Dimensions
- Custom OD, thickness, and bore
- Project-specific dimensional tolerances
High-Thickness / High-Pressure Flanges
- Designed for Class 1500–2500 applications
- Enhanced rigidity and load capacity
Special RTJ Groove Configurations
- Custom groove dimensions
- Compatibility with non-standard ring gaskets
Custom Drilling Patterns
- Modified bolt hole arrangements
- Special BCD configurations
Project Identification & Stamping
- Client-specific marking
- Traceability coding
- EPC documentation alignment
Engineering Conclusion
Forged Flanges are critical pressure-boundary components that integrate mechanical design, material science, and sealing engineering into a single functional unit.
Their performance is governed by:
- Correct selection of pressure class
- Proper material specification
- Controlled manufacturing and heat treatment
- Accurate machining and surface finishing
- Verified inspection and certification
- Proper installation and preload control
From an EPC and consultant evaluation perspective, a compliant Forged Flange must demonstrate:
- Conformance to ASME / ASTM / EN standards
- Verified mechanical and chemical properties
- Dimensional accuracy within specified tolerances
- Traceability from raw material to final product
- Documented inspection and testing records
Super Industries supplies Forged Flanges aligned with these engineering requirements, supporting:
- Pressure system reliability
- Inspection compliance
- Global project execution standards