
FULLY THREADED STUDS
Super Industries
“Global Manufacturer of Heavy & Custom Engineered Fasteners for Oil & Gas, Power & EPC Contractors.”
Super Industries manufactures industrial fastening components used in high-integrity mechanical and structural assemblies where predictable preload behavior, controlled thread engagement, and dimensional consistency are required for engineered bolted joints. Among these fastening components, Fully Threaded Studs serve an important role in assemblies requiring full-length thread engagement, adjustable clamping configurations, and multi-nut fastening arrangements used across heavy industry and capital equipment sectors.
1. Industry Context & System Relevance
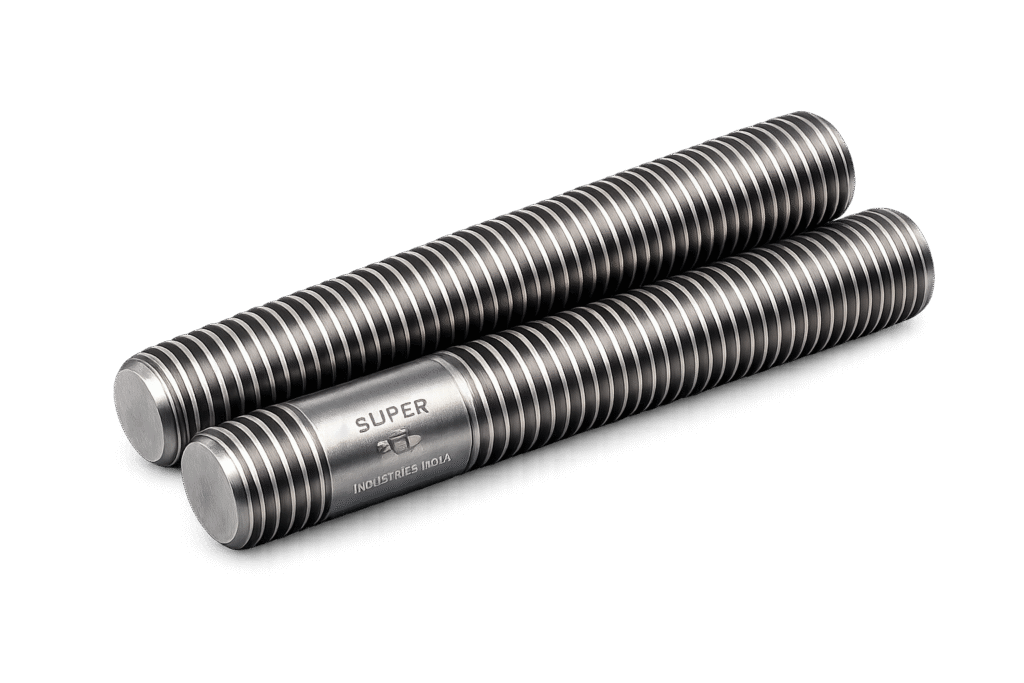
Role of Fully Threaded Studs in Industrial Fastening Systems
Industrial mechanical systems rely on high-strength bolted joints to maintain structural stability, pressure containment, and mechanical alignment under operational loading conditions. In many assemblies, fasteners must provide:
- High tensile load capacity
- Predictable preload behavior
- Full thread engagement across adjustable clamping distances
- Compatibility with multi-nut fastening arrangements
Fully Threaded Studs are frequently selected when an assembly requires continuous external threading along the entire length of the fastener, enabling flexible installation configurations while maintaining full thread engagement.
Because the entire length of the stud is threaded, nuts can be positioned at any point along the stud body, allowing engineers to adjust clamping distance without modifying the fastener geometry.
This feature becomes particularly relevant in industrial assemblies where equipment tolerances, gasket compression, or component stack heights vary during installation.
Industrial Applications
Fully Threaded Studs are used across multiple heavy industrial sectors where controlled mechanical fastening is necessary for safe operation.
Oil & Gas Facilities
In upstream and midstream installations, equipment such as valve systems, pump housings, and instrumentation supports often require adjustable threaded fasteners. Fully Threaded Studs allow technicians to compensate for variations in component stack heights while maintaining uniform thread engagement.
Typical applications include:
- Equipment mounting frames
- Instrumentation panels
- Structural bracing assemblies
- Process skid installations
Refineries & Petrochemical Plants
Large process facilities involve thousands of bolted connections supporting piping systems, structural supports, equipment bases, and modular installations. Fully Threaded Studs provide flexibility in situations where standard bolt lengths may not provide sufficient engagement.
Typical refinery uses include:
- Structural steel bracing
- Pipe support systems
- Equipment mounting structures
- Modular plant assemblies
Power Generation Facilities
Thermal and combined cycle power plants rely on heavy equipment installations requiring adjustable fastening systems during erection and maintenance phases.
Examples include:
- Turbine support structures
- Heat exchanger frames
- Generator base plates
- Structural anchoring assemblies
Fully Threaded Studs allow the use of double-nut clamping arrangements that provide precise positioning and locking capability.
Pressure Vessels & Process Equipment
Certain pressure equipment installations involve structural or auxiliary mounting components where threaded rods are used for alignment or positioning purposes.
Fully Threaded Studs may be applied in:
- Equipment support brackets
- Vessel insulation support systems
- Internal support frames
Steel Plants & Heavy Manufacturing
Heavy machinery used in rolling mills, furnaces, and casting equipment requires robust fastening systems capable of resisting vibration and dynamic loads.
Fully Threaded Studs are used in:
- Structural frames
- Maintenance platforms
- Equipment alignment systems
- Machine base assemblies
Infrastructure Projects
Large infrastructure installations such as bridges, transportation hubs, and industrial buildings also utilize threaded rod-type fasteners for adjustable clamping systems.
Applications include:
- Structural steel assemblies
- Expansion joint systems
- Equipment support frames
- Temporary erection structures
Engineering Reasons for Selecting Fully Threaded Studs
Engineers specify Fully Threaded Studs for several mechanical and installation advantages.
1. Uniform Thread Engagement
Because threads extend along the entire length of the stud, nut engagement can occur at any position, allowing consistent clamping regardless of component thickness variations.
2. Adjustable Clamping Length
Unlike fixed-length bolts, Fully Threaded Studs allow nuts to be positioned precisely to accommodate different component stack heights.
3. Multi-Nut Clamping Systems
Fully Threaded Studs enable double-nut or lock-nut configurations, which are frequently used in:
- vibration-prone environments
- structural bracing assemblies
- equipment alignment systems
4. Simplified Installation for Long Fasteners
For long fastening requirements, handling a threaded rod with nuts installed after placement is often easier than inserting a long bolt through multiple components.
5. Replacement Flexibility
If the clamping configuration changes, the stud length may remain unchanged while nut positioning adjusts the effective clamping distance.
Comparison with Other Fastener Types
Hex Bolts
Hex bolts have a partially threaded shank, designed to provide shear resistance when the unthreaded portion occupies the shear plane. However, they provide less flexibility for adjustable clamping distances.
Partially Threaded Studs
Partially threaded studs include a smooth section between threaded ends. They are commonly used in flange assemblies but do not allow nut placement along the entire length.
Double End Studs
Double End Studs have threads on both ends with a central unthreaded body and are typically installed into tapped holes. They are used where one end remains permanently fixed.
Tap End Studs
Tap End Studs include unequal thread lengths and are designed specifically for threaded hole engagement.
Fully Threaded Studs
Fully Threaded Studs differ from the above fasteners by offering:
- continuous threading
- flexible nut positioning
- adaptable clamping configurations
These characteristics make them suitable for structural and adjustable fastening systems.
2. Technical Definition
Engineering Definition of Fully Threaded Studs
Fully Threaded Studs are cylindrical fasteners consisting of a straight rod with continuous external threading along the entire length of the fastener.
They are designed to be installed using:
- two nuts on opposite ends, or
- one or more nuts positioned along the threaded body.
Unlike bolts, Fully Threaded Studs do not include an integral head. Clamping force is generated through the tightening of nuts against mating components.
Thread Geometry
Thread geometry determines how load is transferred between the stud and the nut.
Important geometric parameters include:
- Major diameter
- Minor diameter
- Pitch diameter
- Thread pitch
- Thread flank angle
These parameters determine the contact area between mating threads, which influences load capacity and friction behavior.
Thread Engagement Length
The thread engagement length refers to the axial distance over which mating threads share the applied load.
Proper engagement ensures:
- adequate load distribution across threads
- prevention of thread stripping
- predictable tensile performance
For most applications, minimum engagement is determined relative to the nominal diameter of the fastener and the strength of the mating material.
Clamping Force Mechanics
The primary purpose of a threaded fastener is to create clamping force between joint members.
When a nut is tightened on a Fully Threaded Stud:
- The stud undergoes elastic elongation.
- The clamped components undergo compressive deformation.
- The resulting preload generates friction between joint surfaces.
This friction resists external forces attempting to separate or slide the joint components.
Tension vs Shear Loading
Threaded fasteners can experience different types of loads.
Tensile Loading
Tensile load acts along the axis of the stud and attempts to stretch the fastener.
Fully Threaded Studs primarily resist tensile loads through the tensile stress area of the threaded section.
Shear Loading
Shear forces act perpendicular to the axis of the fastener.
In threaded rods, the shear plane often passes through the threaded portion, which reduces the shear area compared with a bolt with a smooth shank.
For this reason, engineers typically evaluate shear capacity carefully when specifying fully threaded fasteners in structural applications.
Typical Use in Mechanical Assemblies
Fully Threaded Studs are commonly used in:
- structural clamping assemblies
- equipment mounting systems
- heavy machinery alignment structures
- pressure equipment support structures
- adjustable fastening systems
Because nuts can be positioned along the full thread length, these studs provide installation flexibility while maintaining full thread engagement.
Super Industries
Global Manufacturer of Heavy & Custom Engineered Fasteners & Flanges
3. Mechanical Fastening Principle
Bolt Preload Mechanics
The mechanical performance of any threaded fastener depends primarily on the preload generated during tightening.
Preload is the tensile force created within the stud when the nut is tightened. This force compresses the joint members together.
Proper preload is essential because it determines:
- joint stability
- resistance to vibration loosening
- sealing integrity in gasketed joints
- fatigue resistance under cyclic loading
Elastic Stretch of Studs
When a nut is tightened, the stud behaves like a tension spring.
The applied torque causes the stud to elongate elastically. This elongation generates tensile force inside the fastener.
The clamped components simultaneously compress under the applied load.
The balance between stud elongation and joint compression establishes the final clamping force.
Relationship Between Torque and Preload
In most installations, preload is controlled through torque application.
Torque applied to the nut must overcome:
- thread friction
- nut bearing friction
- elastic deformation of the stud
Because friction consumes a large portion of the applied torque, only a fraction of the torque is converted into useful tensile preload.
Nut Factor (K Value)
The torque-tension relationship is commonly expressed using a nut factor, often designated as K.
This coefficient represents the combined effect of thread friction and bearing friction.
The value of K varies depending on:
- surface finish
- lubrication condition
- coating type
- thread geometry
Typical K values range between 0.15 and 0.25.
Thread Friction Behavior
Thread friction occurs at two locations:
- Between mating threads
- Between the nut face and the bearing surface
Surface coatings, lubrication, and thread finish strongly influence the friction coefficient.
Variations in friction cause variations in achieved preload, which is why controlled lubrication is often specified during installation.
Joint Integrity Under Vibration
Industrial equipment often operates under:
- vibration
- thermal cycling
- dynamic loads
These conditions may reduce preload over time through mechanisms such as:
- embedding of surface roughness
- gasket creep
- relaxation of joint materials
Fully Threaded Studs used with double-nut locking configurations can help maintain preload by preventing nut rotation.
Additionally, adequate preload ensures that external loads are carried primarily through joint friction rather than direct shear on the fastener.
Cyclic Load Resistance
Repeated loading cycles can cause fatigue failure if the stress range within the stud becomes excessive.
Maintaining sufficient preload ensures that the joint remains in compression, reducing the cyclic stress experienced by the fastener.
4. Applicable Standards
ASTM, DIN, ISO & ASME Framework
Industrial threaded fasteners are governed by two primary categories of standards:
- Material Standards
- Dimensional and Thread Standards
Understanding the distinction between these categories is essential for specifying Fully Threaded Studs in engineering documentation and EPC procurement specifications.
Material Standards
Material standards define:
- chemical composition
- mechanical properties
- heat treatment requirements
- testing procedures
They ensure that the fastener material achieves the required tensile strength, ductility, and temperature performance.
Common ASTM material specifications used for Fully Threaded Studs include:
ASTM A193
ASTM A193 covers alloy steel and stainless steel bolting materials intended for high-temperature or high-pressure service.
Typical grades include:
- ASTM A193 B7 – chromium-molybdenum alloy steel
- ASTM A193 B16 – high-temperature alloy steel
- ASTM A193 B8 – stainless steel 304
- ASTM A193 B8M – stainless steel 316
These materials are frequently used in refinery, petrochemical, and power plant equipment.
ASTM A320
ASTM A320 covers bolting materials used in low-temperature service, particularly where fracture toughness and impact resistance are required.
Typical grades include:
- ASTM A320 L7 – alloy steel for low temperature
- ASTM A320 B8 – stainless steel for cryogenic environments
These materials are often specified for LNG facilities and cold process equipment.
ASTM A307
ASTM A307 covers carbon steel bolts and threaded rods intended for general structural applications where extremely high strength is not required.
This specification is commonly used in:
- structural assemblies
- equipment supports
- infrastructure projects
ASTM A354
ASTM A354 defines high-strength alloy steel fasteners, commonly used in heavy structural applications requiring high tensile capacity.
Grades include:
- Grade BC
- Grade BD
ASTM F1554
ASTM F1554 specifies anchor bolts used in structural anchoring applications, which may also be produced in fully threaded configurations for adjustable installation.
Thread Standards
Thread geometry and dimensional accuracy are governed by internationally recognized thread standards.
These standards ensure interchangeability between fasteners and nuts manufactured in different facilities.
ASME B1.1 – Unified Inch Screw Threads
ASME B1.1 defines:
- UNC (Unified National Coarse) threads
- UNF (Unified National Fine) threads
- thread tolerances
- pitch diameter limits
UNC threads are commonly used in heavy structural applications due to their greater thread depth and improved resistance to thread stripping.
ISO Metric Threads
Metric thread standards are defined by ISO specifications that govern:
- metric thread geometry
- pitch values
- tolerance classes
Metric threaded studs are widely used in European industrial equipment and global machinery installations.
DIN Thread Specifications
DIN thread standards are frequently referenced in European mechanical design and equipment manufacturing.
They define:
- thread profiles
- tolerances
- dimensional compatibility with ISO metric systems.
Relationship Between Material and Dimensional Standards
In engineering documentation, both material and dimensional standards must be specified.
Example specification:
ASTM A193 B7 Fully Threaded Studs
Threads per ASME B1.1 UNC Series
This format ensures that:
- the material meets mechanical property requirements
- the thread geometry meets dimensional compatibility standards
Such dual referencing is standard practice in EPC procurement documentation.
5. Material & Grade Options
Material selection determines the load capacity, corrosion resistance, and operating temperature limits of Fully Threaded Studs.
The most common materials fall into four categories:
- Carbon Steel
- Stainless Steel
- Alloy Steel
- High-Performance Corrosion-Resistant Alloys
Carbon Steel Fasteners
Carbon steel materials are widely used where moderate strength and general corrosion conditions are acceptable.
Common grades include:
- ASTM A307
- ASTM A36
These materials are typically used in structural assemblies and infrastructure equipment where operating temperatures are moderate and environmental corrosion exposure is limited.
Stainless Steel Fasteners
Stainless steel Fully Threaded Studs are selected for environments where corrosion resistance is required.
Common grades include:
- ASTM A193 B8 (Type 304 Stainless Steel)
- ASTM A193 B8M (Type 316 Stainless Steel)
- ASTM A320 B8
Stainless steels provide improved resistance to oxidation and chemical corrosion while maintaining good ductility.
Alloy Steel Fasteners
Alloy steels are used when high tensile strength and temperature resistance are required.
Common grades include:
- ASTM A193 B7
- ASTM A193 B16
These materials contain chromium and molybdenum alloying elements that improve strength and heat resistance.
Low Temperature Alloy Steel
For sub-zero environments and cryogenic service, materials must maintain toughness at low temperatures.
The most commonly used grade is:
- ASTM A320 L7
This material undergoes controlled heat treatment and impact testing to ensure fracture resistance at low temperatures.
High-Performance Corrosion Resistant Alloys
In aggressive industrial environments, specialized alloys may be specified.
Examples include:
- Duplex stainless steel
- Super duplex stainless steel
- Nickel-based alloys
These materials are used in environments involving:
- chloride exposure
- offshore installations
- chemical processing equipment
Material Comparison Table
| Material Grade | Typical Yield Strength | Typical Tensile Strength | Temperature Range | Corrosion Resistance | Typical Industry Use |
|---|---|---|---|---|---|
| ASTM A193 B7 | ~720 MPa | ~860 MPa | −29°C to 425°C | Moderate | Oil & gas equipment |
| ASTM A193 B16 | ~860 MPa | ~1030 MPa | Up to 540°C | Moderate | High-temperature service |
| ASTM A307 | ~250 MPa | ~400 MPa | Ambient service | Low | Structural assemblies |
| ASTM A193 B8 | ~205 MPa | ~515 MPa | −200°C to 400°C | Good | Chemical plants |
| ASTM A193 B8M | ~205 MPa | ~515 MPa | −200°C to 400°C | Very good | Marine environments |
| ASTM A320 L7 | ~720 MPa | ~860 MPa | −101°C service | Moderate | LNG facilities |
| Duplex Stainless Steel | ~450 MPa | ~620 MPa | −50°C to 300°C | High | Offshore structures |
The final material selection depends on:
- required mechanical strength
- operating temperature
- corrosion exposure
- design safety factors
6. Heat Treatment Information
Heat treatment is used to develop the required mechanical properties in alloy and carbon steel fasteners.
Different materials require different thermal processing methods.
Quenching and Tempering
High-strength alloy steels such as ASTM A193 B7 and B16 are typically subjected to quenching and tempering.
The process involves:
- Heating the steel above the austenitizing temperature
- Rapid cooling (quenching)
- Controlled reheating (tempering)
This process produces a microstructure that provides:
- high tensile strength
- improved toughness
- controlled hardness
Solution Annealing
Stainless steels such as ASTM A193 B8 and B8M are heat treated through solution annealing.
The process involves heating the material to dissolve chromium carbides and restore corrosion resistance.
Rapid cooling prevents precipitation of carbides that could reduce corrosion resistance.
Normalizing
Some carbon steel materials are normalized to improve:
- grain structure uniformity
- mechanical consistency
- machinability
This process refines the microstructure through controlled heating and air cooling.
Stress Relieving
After machining or thread cutting, stress relieving may be applied to reduce residual stresses in the material.
This process helps prevent distortion and improves dimensional stability.
Hardness Control
Heat treatment processes must achieve hardness levels specified by the relevant ASTM standards.
Excessive hardness can cause brittle fracture, while insufficient hardness may reduce load capacity.
Hardness is typically verified through:
- Rockwell hardness testing
- Brinell hardness testing
Hydrogen Embrittlement Prevention
High-strength steels are susceptible to hydrogen embrittlement, a condition where absorbed hydrogen reduces ductility and causes delayed cracking.
Preventive measures include:
- controlled plating processes
- baking after electroplating
- appropriate heat treatment control
Charpy V-Notch Impact Testing
For low-temperature applications, materials may require Charpy V-notch impact testing.
This test measures the energy absorbed during fracture, providing an indication of material toughness under impact loading conditions.
Impact testing is particularly relevant for materials such as:
- ASTM A320 L7
which are used in cryogenic environments.
7. Manufacturing Process
Production of Fully Threaded Studs
Manufacturing Fully Threaded Studs requires strict dimensional control and material traceability to ensure mechanical reliability in industrial fastening systems.
The production process generally follows a defined sequence.
Raw Material Verification
Manufacturing begins with inspection of incoming steel bars or rods.
Verification typically includes:
- mill test certificate review
- chemical composition verification
- dimensional checks
- ultrasonic inspection for internal defects
This step ensures compliance with the specified ASTM material grade.
Bar Cutting
Steel bars are cut to the required stud length using automated cutting equipment.
Cutting tolerances must ensure that final thread lengths and stud dimensions meet engineering specifications.
Thread Rolling or Thread Cutting
Threads are produced using one of two methods.
Thread Rolling
Thread rolling forms the thread profile by plastically deforming the material.
Advantages include:
- improved surface finish
- increased fatigue strength
- work-hardened thread surface
Thread rolling is commonly used for high-strength fasteners.
Thread Cutting
Thread cutting removes material to produce the thread profile.
This method is typically used when:
- large diameters are required
- specialized thread forms are specified
- short production batches are needed
Heat Treatment
After thread formation, heat treatment is performed according to the specified material grade.
The process ensures that mechanical properties such as tensile strength and hardness meet ASTM requirements.
Straightening
Long threaded studs may undergo straightening operations to ensure axial alignment.
Straightness is critical for proper nut engagement and installation.
Surface Finishing
Surface treatment may be applied to improve corrosion resistance or installation performance.
The type of finish depends on project specifications and service environment.
Final Inspection
Finished studs undergo dimensional and mechanical verification before packaging.
Inspection procedures typically include:
- thread gauge verification
- dimensional measurement
- hardness testing
- visual inspection
Marking & Traceability
Industrial fasteners must remain traceable to their manufacturing batch and material heat number.
Marking practices may include:
- grade identification
- manufacturer identification
- heat number reference
8. Engineering Tables, Torque Charts, Calculations & Inspection
This section provides the engineering data, calculation methods, and inspection procedures used when specifying, installing, and verifying Fully Threaded Studs in industrial mechanical and structural fastening systems.
The information presented here reflects typical engineering practice used by EPC contractors, mechanical design engineers, and inspection authorities when evaluating bolted joint performance.
Tables and calculation methods are provided to support:
- joint design calculations
- installation torque selection
- load capacity assessment
- inspection verification
A. Thread Dimension Reference Tables
Thread geometry directly affects the tensile stress area and load capacity of a threaded fastener.
Design engineers use standardized thread dimensions to ensure compatibility with nuts and tapped holes.
The tensile stress area (As) represents the effective cross-sectional area resisting tensile loads in threaded fasteners.
Unified Thread Series (Typical Industrial Sizes)
| Nominal Diameter | Thread Pitch | Thread Series | Threads Per Inch | Stress Area (mm²) | Recommended Nut Size |
|---|---|---|---|---|---|
| 1/4 in | 1.27 mm | UNC | 20 | 31.8 | 7/16 in |
| 3/8 in | 1.59 mm | UNC | 16 | 77.5 | 9/16 in |
| 1/2 in | 1.81 mm | UNC | 13 | 141.9 | 3/4 in |
| 5/8 in | 2.12 mm | UNC | 11 | 226.0 | 15/16 in |
| 3/4 in | 2.54 mm | UNC | 10 | 334.5 | 1-1/8 in |
| 7/8 in | 2.82 mm | UNC | 9 | 462.0 | 1-5/16 in |
| 1 in | 3.18 mm | UNC | 8 | 606.0 | 1-1/2 in |
| 1-1/8 in | 3.63 mm | UNC | 7 | 763.0 | 1-11/16 in |
| 1-1/4 in | 3.63 mm | UNC | 7 | 969.0 | 1-7/8 in |
| 1-1/2 in | 3.63 mm | UNC | 6 | 1419.0 | 2-1/4 in |
These values represent standardized thread geometry used in heavy industrial fastening.
Metric Thread Reference Table
| Nominal Diameter | Thread Pitch | Thread Series | Stress Area (mm²) | Typical Nut Size |
|---|---|---|---|---|
| M10 | 1.5 mm | Metric Coarse | 58 | 17 mm |
| M12 | 1.75 mm | Metric Coarse | 84 | 19 mm |
| M16 | 2.0 mm | Metric Coarse | 157 | 24 mm |
| M20 | 2.5 mm | Metric Coarse | 245 | 30 mm |
| M24 | 3.0 mm | Metric Coarse | 353 | 36 mm |
| M30 | 3.5 mm | Metric Coarse | 561 | 46 mm |
| M36 | 4.0 mm | Metric Coarse | 817 | 55 mm |
Metric threads are widely used in European industrial equipment and international machinery installations.
B. Mechanical Property Table
Mechanical properties define the load capacity and deformation behavior of Fully Threaded Studs.
| Material Grade | Yield Strength (MPa) | Tensile Strength (MPa) | Elongation (%) | Hardness Range |
|---|---|---|---|---|
| ASTM A307 | 250 | 400 | 23 | HRB 70-95 |
| ASTM A193 B7 | 720 | 860 | 16 | HRC 24-35 |
| ASTM A193 B16 | 860 | 1030 | 15 | HRC 28-36 |
| ASTM A193 B8 | 205 | 515 | 30 | HRB 85-95 |
| ASTM A193 B8M | 205 | 515 | 30 | HRB 85-95 |
| ASTM A320 L7 | 720 | 860 | 16 | HRC 24-35 |
Mechanical property requirements are verified through:
- tensile testing
- hardness testing
- chemical composition analysis
These values determine the maximum preload that can safely be applied during installation.
C. Torque Chart for Fully Threaded Studs
Installation torque must generate sufficient bolt preload without exceeding the proof load of the material.
The following values represent typical installation torque for lubricated and dry conditions.
Torque Chart (Approximate Engineering Reference)
| Stud Size | ASTM A193 B7 Lubricated Torque (Nm) | ASTM A193 B7 Dry Torque (Nm) | ASTM A193 B16 Lubricated Torque (Nm) | Stainless Steel Lubricated Torque (Nm) |
|---|---|---|---|---|
| 1/2 in | 90 | 120 | 110 | 60 |
| 5/8 in | 180 | 230 | 210 | 120 |
| 3/4 in | 320 | 420 | 360 | 210 |
| 7/8 in | 510 | 670 | 580 | 340 |
| 1 in | 770 | 1010 | 860 | 500 |
| 1-1/8 in | 1080 | 1420 | 1210 | 690 |
| 1-1/4 in | 1500 | 1980 | 1670 | 950 |
| 1-1/2 in | 2600 | 3450 | 2900 | 1600 |
Actual torque values depend on:
- lubrication condition
- surface coating
- thread condition
- installation method
For critical applications, hydraulic tensioning or calibrated torque equipment may be used.
D. Preload Calculation Guide
Correct preload ensures that the joint remains compressed under external loading conditions.
Bolt Preload Formula
The tensile force generated in a threaded fastener depends on the applied torque, nut factor, and stud diameter.

Where:
F = Bolt preload (N)
T = Applied torque (Nm)
K = Nut factor (dimensionless friction coefficient)
D = Nominal bolt diameter (m)
Typical nut factor (K) values:
| Condition | K Value |
|---|---|
| Dry threads | 0.20 – 0.25 |
| Light lubrication | 0.15 – 0.18 |
| PTFE coated | 0.10 – 0.13 |
Tensile Stress Equation
The stress generated in the stud during tightening is determined by the applied preload and the tensile stress area.

Where:
σ = tensile stress
F = preload force
A = tensile stress area
The calculated stress must remain below the proof strength of the fastener material.
Sample Engineering Calculation
Example:
Stud size: 1 inch ASTM A193 B7
Torque applied: 770 Nm
Nut factor: 0.18
Preload calculation:
F = 770 / (0.18 × 0.0254)
F ≈ 168,000 N
This preload must be verified against the allowable load capacity of the stud material.
Safety Margin Considerations
Engineering design typically limits preload to approximately 70–75% of the proof load.
This safety margin ensures:
- prevention of yielding during tightening
- tolerance for torque variation
- adequate fatigue life under cyclic loads
E. Yield Strength Load Capacity Trends
The load capacity of Fully Threaded Studs increases proportionally with diameter and material strength.
General trends include:
- Larger diameters produce significantly higher tensile capacity due to increased stress area.
- Alloy steels such as ASTM A193 B16 provide higher strength compared with carbon steel.
- Stainless steels generally provide lower yield strength but improved corrosion resistance.
- Fine thread series increase stress area slightly and may improve fatigue resistance.
Design engineers must consider both material strength and thread stress area when determining load capacity.
F. Corrosion Resistance Comparison
Corrosion resistance is a major factor when selecting materials for threaded fasteners used in industrial environments.
| Material | Marine Environment | Acidic Environment | High Humidity | Hydrocarbon Exposure |
|---|---|---|---|---|
| Carbon Steel | Poor | Poor | Moderate | Good |
| Stainless Steel 304 | Moderate | Moderate | Good | Good |
| Stainless Steel 316 | Good | Good | Excellent | Excellent |
| Duplex Stainless Steel | Excellent | Very Good | Excellent | Excellent |
| Alloy Steel B7 | Moderate | Poor | Moderate | Excellent |
Material selection must consider:
- exposure to chlorides
- chemical process fluids
- atmospheric conditions
- operating temperature
In offshore environments, duplex stainless steel fasteners may be specified due to their high resistance to chloride stress corrosion.
9. Inspection & Quality Control Methods
Quality verification of Fully Threaded Studs involves multiple inspection techniques to ensure compliance with project specifications.
Positive Material Identification (PMI)
PMI testing verifies the chemical composition of alloy materials using spectrometric analysis.
This process confirms that the material grade matches the specified alloy composition.
Ultrasonic Testing (UT)
Ultrasonic inspection detects internal discontinuities such as:
- voids
- inclusions
- cracks
This method is often applied to larger diameter fasteners.
Magnetic Particle Inspection (MPI)
MPI is used to detect surface and near-surface defects in ferromagnetic materials.
It is commonly applied after heat treatment.
Dye Penetrant Inspection (DPI)
DPI detects fine surface cracks in both ferrous and non-ferrous materials.
This method is particularly useful for stainless steel fasteners.
Hardness Testing
Hardness measurements verify that heat treatment processes produced the required mechanical properties.
Typical methods include:
- Rockwell hardness testing
- Brinell hardness testing
Dimensional Inspection
Dimensional checks verify compliance with engineering drawings and thread standards.
Inspection includes:
- stud length measurement
- thread pitch verification
- straightness verification
- thread runout inspection
Thread Gauge Verification
Threads are checked using GO and NO-GO gauges to confirm compliance with specified thread tolerances.
This inspection ensures that studs will properly engage with standard nuts.
Third-Party Inspection
For project-critical equipment, inspection may be conducted by independent inspection agencies.
Third-party verification may include:
- dimensional inspection
- mechanical testing review
- material certification validation
EN 10204 Certification
Industrial fasteners supplied for international projects often require material certification according to EN 10204.
Common certification types include:
EN 10204 3.1
Manufacturer test certificate confirming compliance with material specifications.
EN 10204 3.2
Inspection certificate validated by an independent third-party inspector.
10. Industries Served
Fully Threaded Studs are used across a wide range of heavy industries where mechanical fastening systems must maintain structural integrity under operational loading conditions.
These fasteners are typically applied in assemblies requiring adjustable clamping configurations, long threaded engagement, or double-nut locking arrangements.
Upstream Oil & Gas
Upstream oil and gas installations involve equipment operating in demanding environments that include vibration, temperature variation, and structural loading.
Fully Threaded Studs are used in:
- equipment mounting frames
- instrumentation support assemblies
- skid-mounted process equipment
- drilling rig structural components
In these installations, the ability to adjust nut positions along the stud length allows technicians to compensate for variations in structural component thickness.
Petrochemical Processing Plants
Petrochemical facilities contain extensive mechanical infrastructure including reactors, pumps, heat exchangers, and piping networks.
Fully Threaded Studs are frequently used for:
- structural equipment supports
- pipe rack assemblies
- mechanical bracing structures
- process skid installations
The continuous thread design allows flexible nut positioning during plant construction and maintenance.
Oil Refineries
Refinery installations require reliable fastening systems capable of supporting heavy equipment and structural frameworks.
Typical refinery uses include:
- structural steel bracing
- platform and walkway supports
- equipment base frames
- maintenance structures
Fully Threaded Studs are particularly useful in assemblies requiring double-nut locking configurations to resist vibration.
Power Generation Facilities
Power plants rely on numerous mechanical assemblies requiring reliable threaded fasteners.
Applications include:
- turbine auxiliary structures
- generator support systems
- equipment mounting assemblies
- pipe support frameworks
Fully Threaded Studs are used where equipment alignment adjustments may be required during installation.
LNG & Cryogenic Installations
Liquefied natural gas facilities operate under low-temperature conditions that require materials with sufficient fracture toughness.
In such facilities, Fully Threaded Studs manufactured from appropriate materials such as low-temperature alloy steels are used in structural fastening systems and equipment supports.
Offshore Platforms
Offshore installations operate in highly corrosive marine environments and are subject to dynamic loading from wind and wave motion.
Fasteners used in these installations must provide:
- corrosion resistance
- vibration resistance
- reliable preload retention
Fully Threaded Studs made from corrosion-resistant materials are commonly used in:
- equipment mounting assemblies
- platform structural systems
- support frameworks.
Steel Manufacturing Plants
Heavy industrial equipment used in steel plants generates vibration and dynamic loads during operation.
Fully Threaded Studs are used in:
- furnace structural frames
- rolling mill equipment supports
- machinery alignment assemblies
- maintenance platform structures
These fasteners allow adjustments during equipment alignment procedures.
Heavy Industrial Equipment Manufacturing
Manufacturers of large industrial machines frequently require threaded rods for adjustable fastening configurations.
Typical applications include:
- machine base assemblies
- modular equipment frames
- adjustable mechanical brackets
- equipment alignment fixtures
Infrastructure Engineering
Infrastructure projects frequently involve structural fastening systems where adjustable threaded rods provide installation flexibility.
Applications include:
- structural steel frameworks
- mechanical equipment supports
- industrial building installations
- transport facility structures.
11. Export Capability & Global Supply
Super Industries manufactures Fully Threaded Studs for international supply to industrial clients involved in capital engineering projects.
Export supply requires adherence to international material standards, dimensional specifications, and project documentation requirements.
Global Supply Regions
Industrial fasteners are supplied to engineering contractors and project procurement teams operating in multiple geographic regions, including:
- United States
- Europe
- Middle East
- Southeast Asia
Each region may apply different regulatory standards and inspection requirements for industrial fastening components.
Export Packaging Standards
Export packaging must ensure that threaded fasteners arrive at the installation site without mechanical damage or corrosion.
Typical export packaging methods include:
- sealed wooden crates
- heavy-duty palletized cartons
- moisture-resistant protective wrapping
- corrosion protection coatings
Proper packaging prevents thread damage during long-distance transportation.
Shipping Documentation
International shipments of industrial fasteners typically include documentation required for customs clearance and project verification.
Typical documentation includes:
- commercial invoice
- packing list
- mill test certificates
- inspection reports
- certificate of origin
These documents allow procurement teams to verify compliance with project specifications.
Project Logistics Coordination
Large capital projects often require coordinated delivery of fastening components to match construction schedules.
Logistics coordination may involve:
- staged shipments
- project-specific packaging identification
- installation sequence planning
- coordination with third-party inspectors.
Such coordination ensures that fastening components are available when required during plant construction.
12.Procurement & Installation Practices
Correct installation practices are critical to achieving the designed performance of Fully Threaded Studs in industrial assemblies.
Improper installation can result in insufficient preload, joint loosening, or mechanical failure.
Stud Installation Practices
The installation sequence typically involves:
- positioning the stud through the joint components
- installing nuts on both sides of the assembly
- applying controlled torque to achieve the specified preload
Where studs are installed into tapped holes, the thread engagement must satisfy the minimum engagement length required by engineering specifications.
Nut Tightening Sequence
In assemblies containing multiple fasteners, tightening must follow a controlled sequence to ensure uniform load distribution.
Typical tightening methods include:
- star pattern tightening
- cross-pattern tightening
- incremental torque application
These methods help distribute preload evenly across the joint.
Cross-Tightening Method
Cross-tightening is commonly used when installing multiple fasteners around a joint.
This method involves tightening fasteners in a pattern that alternates across the joint rather than proceeding sequentially around the perimeter.
The objective is to prevent uneven compression of joint components.
Lubrication Recommendations
Lubrication is frequently applied to threaded fasteners to reduce friction during tightening.
Lubrication provides several benefits:
- more consistent preload generation
- reduced thread galling
- lower torque variation
Common lubricants include:
- molybdenum-based anti-seize compounds
- graphite-based lubricants
- PTFE-based thread lubricants
Lubrication selection depends on material type and operating temperature.
Field Inspection Checkpoints
During installation, field inspectors typically verify several aspects of the fastening process.
Inspection checkpoints include:
- confirmation of correct stud grade
- verification of thread condition
- confirmation of correct torque application
- verification of proper nut engagement
These inspections ensure that the installed fasteners meet project specifications.
Storage Discipline
Proper storage is necessary to maintain the integrity of threaded fasteners prior to installation.
Recommended storage practices include:
- storing fasteners in dry environments
- protecting threads from mechanical damage
- segregating materials by grade and heat number
- maintaining packaging until installation.
These practices help maintain material traceability and prevent corrosion.
13.Custom Engineering Capabilities
Industrial projects often require threaded fasteners that differ from standard catalog sizes or materials.
Custom manufacturing capabilities allow Fully Threaded Studs to be produced according to project-specific engineering requirements.
Non-Standard Stud Lengths
Certain installations require studs longer than standard commercially available sizes.
Manufacturing capability may include production of:
- extended length threaded rods
- special cut lengths according to project drawings.
Special Thread Pitches
Some engineering systems specify non-standard thread pitches to match existing equipment or specialized nuts.
Custom threading may include:
- fine pitch threads
- metric thread variations
- project-specific thread forms.
Large Diameter Studs
Heavy industrial equipment occasionally requires large-diameter threaded rods to support high load capacities.
Manufacturing may include studs exceeding common commercial diameters.
High-Temperature Materials
Certain installations operate at elevated temperatures requiring materials with improved heat resistance.
Possible materials include:
- chromium-molybdenum alloy steels
- high-temperature stainless steels
- specialized alloy materials.
Project-Specific Marking
Project procurement specifications may require specific marking practices for traceability.
Marking methods may include:
- grade identification
- heat number marking
- project identification numbers
These markings assist inspectors in verifying compliance with project documentation.
Engineering Summary
Fully Threaded Studs serve as versatile fastening components used in structural and mechanical assemblies where continuous thread engagement and adjustable clamping configurations are required.
Their mechanical performance depends on several factors:
- material selection
- thread geometry
- installation preload
- environmental exposure conditions.
When properly specified and installed, Fully Threaded Studs contribute to reliable load transfer within bolted joints used in industrial equipment and structural systems.
For engineering applications, careful consideration must be given to:
- applicable material standards
- mechanical property requirements
- corrosion resistance
- installation procedures
- inspection and quality verification.