
Elevator Bolts
Super Industries
“Global Manufacturer of Heavy & Custom Engineered Fasteners for Oil & Gas, Power & EPC Contractors.”
1. Industry Context & System Relevance
1.1 Role of Elevator Bolts in Bulk Material Handling Systems
Elevator Bolts are mechanical fastening components used for securing buckets to conveyor belts in bucket elevator systems. These systems transport bulk materials vertically or at steep inclines in industrial facilities handling large volumes of particulate or granular material.
Bucket elevators operate continuously under cyclic loading conditions, transporting materials such as:
- Cement clinker
- Coal
- Grain
- Fertilizer granules
- Limestone
- Iron ore fines
- Aggregates
- Industrial minerals
- Powdered chemicals
In these applications, the fastening system between the bucket body and the conveyor belt becomes a critical mechanical interface. Elevator bolts provide a fastening method that ensures:
- Stable bucket retention
- Uniform load transfer
- Minimal internal belt obstruction
- Reduced belt wear
- Reliable operation under vibration and cyclic mechanical stress
The geometry of elevator bolts differs significantly from standard hex bolts due to the specific functional requirements of conveyor belt installations.
Super Industries
Global Manufacturer of Heavy & Custom Engineered Fasteners & Flanges
1.2 Bucket Elevator System Overview
A typical bucket elevator consists of several primary mechanical elements:
- Drive pulley (head pulley)
- Tail pulley
- Conveyor belt or chain
- Elevator buckets
- Drive motor and gearbox
- Structural casing
- Fastening system (elevator bolts, nuts, washers)
Elevator buckets are mounted at regular intervals along a reinforced rubber or polymer conveyor belt. During operation:
- Buckets collect material at the boot section
- The belt carries the material vertically
- Material is discharged at the head section through centrifugal or gravity discharge
The fasteners used to secure the buckets must resist multiple forms of mechanical stress including:
- Tensile loading
- Shear forces
- Impact loading during filling
- Continuous vibration
- Cyclic fatigue
Elevator bolts are engineered specifically to withstand these mechanical conditions while protecting the conveyor belt from damage.
1.3 Why Elevator Bolts Are Preferred Over Standard Hex Bolts
Standard hex bolts are unsuitable for bucket elevator assemblies due to several operational constraints.
Flush Surface Requirement
Inside the bucket elevator casing, the conveyor belt interior must remain smooth to prevent material accumulation.
Elevator bolts feature flat or low-profile heads that sit flush against the bucket interior surface. This design prevents:
- Product buildup
- Flow obstruction
- Abrasion of moving material
Belt Protection
A hex bolt head can create concentrated pressure points against the belt surface. Over time this can lead to:
- Belt tearing
- Surface cracking
- Abrasive wear
Elevator bolts use large-diameter flat heads that distribute bearing pressure over a wider surface area, reducing stress concentration on the belt.
Reduced Material Buildup
Industrial bulk materials often include fine powders and granules that can accumulate around protruding fastener heads.
Elevator bolts minimize this risk by providing:
- Smooth head profiles
- Flush mounting surfaces
- Minimal internal projections
This improves operational efficiency in systems transporting materials such as:
- Cement powder
- Grain
- Fly ash
- Fertilizer dust
Resistance to High Vibration
Bucket elevators operate with continuous mechanical motion and periodic loading impacts. Fasteners must resist loosening under vibration.
Elevator bolts use square neck or ribbed neck configurations that lock into the bucket wall or belt material during installation, preventing rotation during tightening and operation.
1.4 Conveyor Belt Fastener Load Distribution
When buckets are attached to the conveyor belt, the load from the transported material must transfer through the fastening system.
The mechanical load path follows this sequence:
Material Load → Bucket Shell → Elevator Bolt Head → Bolt Shank → Washer → Nut → Belt Interface
The bolt head must provide adequate bearing area to prevent local deformation of the bucket or belt.
If load distribution is uneven, potential failures include:
- Belt tearing
- Bolt pull-through
- Bucket detachment
- Fastener fatigue fracture
The geometry of elevator bolts is specifically designed to maintain uniform load distribution across the bucket mounting interface.
2. Technical Definition of Elevator Bolts
2.1 What Are Elevator Bolts?
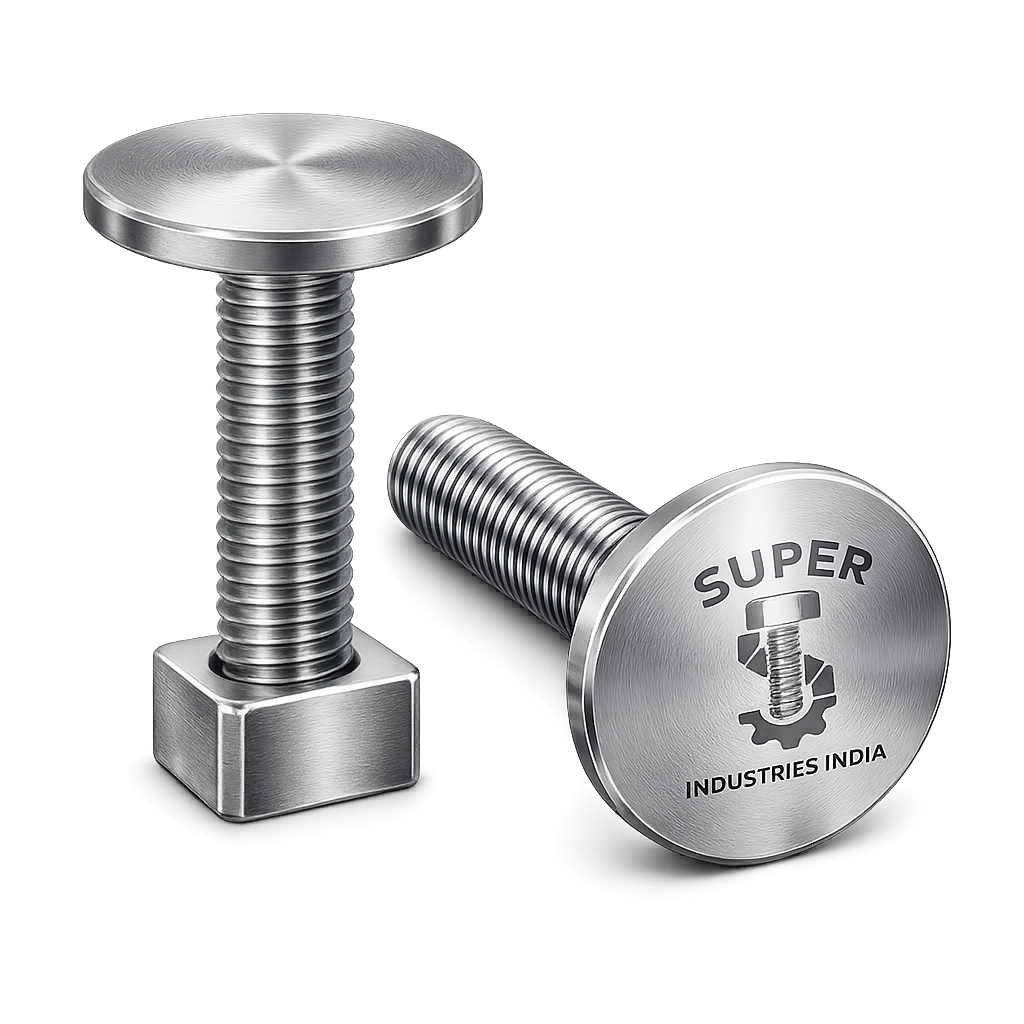
Elevator Bolts are specialized mechanical fasteners designed for attaching buckets to conveyor belts in bucket elevator systems used in bulk material handling applications.
They are characterized by:
- Large diameter flat head
- Low head profile
- Square or ribbed neck below the head
- Threaded shank for nut attachment
- Wide bearing surface for belt protection
Elevator bolts are typically installed from the inside of the bucket, with the threaded portion passing through:
- Bucket wall
- Conveyor belt
- Washer
- Locking nut
This configuration ensures the smooth interior surface necessary for material transport.
2.2 Structural Components of Elevator Bolts
An elevator bolt consists of several engineered components:
Bolt Head
The bolt head is typically large and flat to distribute pressure evenly across the bucket wall.
Design objectives include:
- Maximizing contact area
- Preventing pull-through
- Maintaining flush internal surface
Square Neck or Ribbed Neck
Directly beneath the head is a square or ribbed section.
This feature performs two functions:
- Prevents bolt rotation during tightening
- Locks the bolt into the bucket or belt material
The square neck engages with the punched hole in the bucket wall, forming a mechanical lock that stabilizes the fastener during installation.
Shank
The shank forms the main structural body of the fastener. It carries the tensile and shear loads generated during system operation.
The shank diameter determines:
- Tensile capacity
- Shear resistance
- Fatigue performance
Threaded Section
The threaded portion allows installation of:
- Hex nuts
- Lock nuts
- Self-locking nuts
Thread design typically follows metric or UNC/UNF thread profiles, depending on the system design specification.
2.3 Types of Elevator Bolts
Elevator bolts are manufactured in several standardized designs depending on bucket type and system requirements.
Flat Countersunk Head Elevator Bolts
This is the most common configuration used in bucket elevators.
Features:
- Flat circular head
- Large bearing diameter
- Square neck locking feature
Advantages include uniform load distribution and smooth bucket interior surface.
Euro Head Elevator Bolts
Euro head bolts feature a slightly domed head profile designed to improve mechanical engagement with the bucket surface.
Characteristics include:
- Reinforced head geometry
- Enhanced impact resistance
- Larger head diameter
These are commonly used in heavy-duty conveyor systems.
Fanged Elevator Bolts
Fanged bolts include radial protrusions beneath the head that embed into the bucket surface.
These features increase rotational resistance and improve fastening stability under vibration.
Ref70 Elevator Bolts
Ref70 elevator bolts are specialized designs used in high-capacity bucket elevators.
Key characteristics include:
- Extended head diameter
- High bearing surface
- Optimized head thickness
These are often used in mining and cement industry conveyors.
2.4 Functional Role in Bucket Retention
Elevator bolts perform several simultaneous mechanical functions:
- Secure bucket attachment to the conveyor belt
- Transfer material load from bucket to belt
- Prevent bucket movement during operation
- Protect belt from localized stress damage
The fastening system must maintain integrity even when exposed to:
- Continuous vibration
- Impact loads
- Abrasive material flow
- Temperature variation
- Dust and moisture exposure
2.5 Washer and Nut Interface
The nut and washer assembly provides the clamping force necessary to secure the bucket to the belt.
Typical components include:
- Heavy-duty flat washer
- Lock washer (optional)
- Hex nut or lock nut
The washer spreads the clamping load across the belt surface, preventing localized deformation or tearing.
Correct washer diameter is critical to maintaining long-term belt integrity.
Super Industries
Global Manufacturer of Heavy & Custom Engineered Fasteners & Flanges
3. Mechanical Load & Fastening Principle
3.1 Load Transfer Mechanism
In bucket elevator systems, the load acting on the fastening system originates from the weight of the transported material and the bucket itself.
The mechanical load path is as follows:
Material Weight → Bucket Shell → Bolt Head → Bolt Shank → Washer → Nut → Belt
The elevator bolt must transmit both tensile and shear forces while maintaining structural stability.
3.2 Shear Loading on Elevator Bolts
Shear forces occur when the bucket experiences resistance from the transported material or during acceleration of the conveyor belt.
Shear stress is calculated as:

Where:
- τ = shear stress
- F = applied force
- A = cross-sectional area of bolt shank
Elevator bolts must be sized so that shear stress remains well below the allowable material limit.
3.3 Tensile Loading During Operation
Tensile forces occur due to:
- Bucket weight
- Material load
- Centrifugal force during elevator rotation
The tensile stress on the bolt can be expressed as:

Where:
- σ = tensile stress
- F = axial load
- A = tensile stress area of the bolt
Proper bolt grade selection ensures adequate tensile capacity for system loads.
3.4 Dynamic Loading in Bucket Elevators
Bucket elevators experience continuous dynamic loading due to:
- Repeated bucket filling
- Centrifugal discharge
- Belt acceleration
- Mechanical vibration
These cyclic loads introduce fatigue stress in the fastening system.
Elevator bolts must therefore provide:
- High fatigue resistance
- Stable clamping force
- Reliable load distribution
3.5 Impact Loads During Bucket Filling
When buckets collect material at the elevator boot section, the incoming material may produce sudden impact loads.
These forces act primarily on:
- Bucket wall
- Bolt head
- Bolt shank
Proper head diameter and bolt grade selection help prevent:
- Head deformation
- Bolt bending
- Shank fatigue cracking
3.6 Anti-Loosening Mechanisms
Fastener loosening can occur due to vibration or cyclic loading.
Elevator bolt systems typically prevent loosening through several mechanisms:
Square Neck Locking
The square neck beneath the bolt head prevents bolt rotation during tightening and operation.
Frictional Clamping Force
The nut and washer assembly generates a clamping force that maintains joint stability.
Lock Nuts or Prevailing Torque Nuts
These nuts include mechanical features that resist loosening under vibration.
Proper Installation Torque
Correct tightening torque ensures sufficient preload in the bolt to resist dynamic loads.
4. Applicable Standards (ASTM / DIN / ISO)
Elevator bolts used in bulk material handling equipment are manufactured in accordance with internationally recognized mechanical fastener standards. These standards govern dimensional tolerances, thread geometry, mechanical strength, and material properties.
Compliance with recognized standards ensures that elevator bolts can be integrated into OEM equipment designs and EPC project specifications without dimensional or mechanical incompatibility.
4.1 DIN 15237 – Elevator Bolt Standard
DIN 15237 is the primary international standard governing elevator bolts used in bucket elevator systems.
The standard defines:
• Bolt head geometry
• Head diameter
• Head thickness
• Square neck dimensions
• Thread dimensions
• Standard length ranges
The design defined in DIN 15237 ensures that the bolt head provides sufficient bearing area to prevent pull-through when installed in bucket elevator assemblies.
Typical applications include:
- Grain elevators
- Cement conveyor systems
- Industrial bulk material elevators
- Fertilizer processing plants
DIN 15237 bolts are widely used in European-designed bucket elevator systems.
4.2 ISO Fastener Standards
International Organization for Standardization (ISO) standards govern general fastener design parameters used for elevator bolt threads and mechanical properties.
Relevant ISO specifications include:
ISO 898-1 — Mechanical Properties of Fasteners
This standard specifies mechanical properties for carbon steel and alloy steel fasteners including:
• Yield strength
• Tensile strength
• Elongation
• Hardness
Mechanical classes defined under ISO 898-1 include:
- Class 4.6
- Class 5.8
- Class 8.8
- Class 10.9
For elevator bolts, Class 4.6 or 8.8 are most commonly used depending on application load requirements.
ISO Thread Standards
Thread dimensions and tolerances typically follow:
• ISO Metric Thread Profile
• ISO 965 Tolerance Classes
Standard tolerance class used:
6g external thread
This ensures compatibility with standard industrial nuts.
4.3 ASTM Fastener Standards
In North American industrial projects, elevator bolts are often manufactured according to ASTM material specifications.
ASTM A307 – Carbon Steel Bolts
ASTM A307 bolts are widely used for general structural fastening applications.
Typical properties include:
• Moderate tensile strength
• Good ductility
• Reliable machinability
Elevator bolts manufactured under ASTM A307 are commonly used in:
- Grain handling equipment
- Agricultural conveyor systems
- Light industrial elevators
ASTM A449 – Medium Strength Carbon Steel Bolts
ASTM A449 provides higher strength than ASTM A307 and is suitable for heavier industrial conveyor loads.
Applications include:
- Mining conveyors
- Aggregate processing plants
- Cement manufacturing systems
ASTM A193 – Alloy Steel Fasteners
ASTM A193 covers alloy steel fasteners designed for high strength and elevated temperature service.
Relevant grades include:
ASTM A193 B7 – Alloy steel with quench and temper heat treatment.
These are used in high-load elevator systems operating under demanding mechanical conditions.
4.4 Influence of Standards on Elevator Bolt Design
International standards influence several aspects of elevator bolt engineering:
Mechanical Strength
Material specifications determine allowable tensile and shear loads.
Dimensional Accuracy
Standards define:
• Head geometry
• Shank diameter tolerances
• Thread pitch
These parameters ensure interchangeability in global equipment installations.
Material Traceability
Standards require documentation including:
• Heat numbers
• Material certificates
• Mechanical test records
This is essential for EPC project quality control and third-party inspection.
5. Material & Grade Options for Elevator Bolts
Material selection for elevator bolts depends on:
• Load requirements
• Operating environment
• Corrosion exposure
• Temperature range
• Industry application
The most commonly used materials include carbon steel, stainless steel, and alloy steel grades.
Carbon Steel Elevator Bolts
Carbon steel bolts are widely used for industrial conveyor systems where corrosion exposure is moderate.
Typical grades include:
ASTM A307
Properties include:
• Moderate tensile strength
• Good ductility
• Cost-effective manufacturing
Common applications:
- Grain elevators
- Agricultural conveyors
- Light industrial material handling
ASTM A449
ASTM A449 provides higher mechanical strength compared to A307.
Applications include:
- Cement plant conveyors
- Aggregate handling systems
- Mining material transport equipment
Stainless Steel Elevator Bolts
Stainless steel bolts are used in environments where corrosion resistance is required.
ASTM A193 B8 (Type 304 Stainless Steel)
Characteristics include:
• Good corrosion resistance
• Suitable for humid environments
• Moderate mechanical strength
Typical industries:
- Food processing plants
- Grain handling facilities
- Chemical processing units
ASTM A193 B8M (Type 316 Stainless Steel)
316 stainless steel provides improved resistance to:
• Chlorides
• Marine exposure
• Chemical corrosion
Applications include:
- Coastal grain terminals
- Fertilizer plants
- Chemical material conveyors
Alloy Steel Elevator Bolts
Alloy steel elevator bolts provide higher mechanical strength.
ASTM A193 B7
This grade is produced through quench and temper heat treatment.
Properties include:
• High tensile strength
• Improved fatigue resistance
• Better load capacity
Applications include:
- Mining bucket elevators
- Cement plant vertical conveyors
- High-capacity industrial material elevators
Material Comparison Table
| Grade | Yield Strength | Tensile Strength | Temperature Range | Corrosion Resistance | Typical Industry Use |
|---|---|---|---|---|---|
| ASTM A307 | ~240 MPa | ~415 MPa | −20°C to 200°C | Low | Grain elevators, agricultural conveyors |
| ASTM A449 | ~380 MPa | ~620 MPa | −40°C to 300°C | Low to Moderate | Mining conveyors, cement plants |
| ASTM A193 B7 | ~720 MPa | ~860 MPa | −40°C to 450°C | Moderate | High-load industrial conveyors |
| ASTM A193 B8 (304 SS) | ~205 MPa | ~515 MPa | −200°C to 400°C | High | Food processing, grain facilities |
| ASTM A193 B8M (316 SS) | ~205 MPa | ~515 MPa | −200°C to 450°C | Very High | Marine, chemical handling systems |
6. Heat Treatment of Elevator Bolts
Heat treatment is applied to elevator bolts to achieve required mechanical properties such as strength, hardness, and fatigue resistance.
6.1 Normalizing
Normalizing involves heating the steel above its critical temperature followed by air cooling.
Objectives include:
• Refining grain structure
• Improving mechanical uniformity
• Increasing toughness
Normalized bolts exhibit improved resistance to cyclic loading.
6.2 Quenching and Tempering
Quenching and tempering is applied to high-strength alloy steel bolts such as ASTM A193 B7.
Process steps include:
- Austenitizing at elevated temperature
- Rapid cooling (quenching)
- Tempering at controlled temperature
Benefits include:
• High tensile strength
• Improved fatigue resistance
• Controlled hardness
6.3 Stress Relieving
Stress relieving is applied after forming or machining to reduce residual stresses.
Advantages include:
• Improved dimensional stability
• Reduced risk of distortion
• Improved fatigue life
6.4 Hardness Control
Hardness levels depend on the material grade and heat treatment applied.
Typical hardness ranges:
| Material Grade | Hardness Range |
|---|---|
| ASTM A307 | 120–180 HB |
| ASTM A449 | 22–30 HRC |
| ASTM A193 B7 | 28–35 HRC |
| Stainless Steel B8 | 150–200 HB |
| Stainless Steel B8M | 150–200 HB |
Hardness testing ensures bolts maintain adequate strength while preventing brittleness.
6.5 Microstructure Control
Proper heat treatment ensures favorable microstructures such as:
• Ferrite-pearlite structures in carbon steels
• Tempered martensite in alloy steels
Microstructure influences:
• Fatigue life
• Crack resistance
• Impact performance
These characteristics are essential in bucket elevators where bolts undergo repeated loading cycles.
7. Manufacturing Process of Elevator Bolts
Manufacturing elevator bolts requires controlled forming, machining, and inspection to achieve dimensional precision and mechanical integrity.
7.1 Raw Material Inspection
Production begins with inspection of incoming steel wire rods or bars.
Verification includes:
• Chemical composition analysis
• Material grade confirmation
• Surface defect inspection
Material traceability is maintained through heat numbers.
7.2 Cold Heading or Hot Forging
Elevator bolt heads are formed using either:
Cold heading – suitable for smaller diameters and high production volumes.
Hot forging – used for larger bolt diameters or thicker head designs.
Forging improves:
• Material density
• Structural integrity
• Grain flow orientation
7.3 Head Forming
The bolt head is formed to precise dimensions including:
• Head diameter
• Head thickness
• Countersunk geometry (if required)
Tooling must maintain tight tolerances to ensure uniform bearing surfaces.
7.4 Square Neck Forming
The square neck section beneath the head is formed using precision dies.
This feature ensures:
• Mechanical locking during installation
• Prevention of bolt rotation during tightening
Dimensional accuracy is essential to ensure proper engagement with bucket holes.
7.5 Thread Rolling
Threads are produced using thread rolling machines rather than cutting.
Advantages include:
• Improved thread strength
• Better fatigue resistance
• Smooth surface finish
Rolled threads maintain continuous grain flow, increasing durability.
7.6 Heat Treatment
Depending on material grade, bolts undergo heat treatment processes such as:
• Normalizing
• Quenching and tempering
• Stress relieving
Controlled furnace operations ensure consistent mechanical properties.
7.7 Surface Coating
After heat treatment, bolts may receive protective coatings to improve corrosion resistance.
Common surface finishes include:
• Zinc plating
• Hot dip galvanizing
• Phosphate coating
• Black oxide finish
Surface treatments also influence friction characteristics during installation.
7.8 Dimensional Inspection
Dimensional inspection verifies compliance with standards.
Parameters checked include:
• Head diameter
• Neck dimensions
• Thread length
• Overall bolt length
Precision gauges and measuring instruments are used.
7.9 Marking & Traceability
Industrial fasteners require traceability for project documentation.
Markings may include:
• Manufacturer identification
• Material grade
• Heat number (batch traceability)
Traceability supports quality audits and third-party inspection requirements.
8.Engineering Tables, Torque Charts, Mechanical Calculations & Inspection Procedures
This section provides engineering reference tables and calculation guides for Elevator Bolts used in bucket elevator fastening systems within industrial bulk material handling equipment.
The information below supports:
- Mechanical design verification
- Fastener selection during system engineering
- EPC procurement specification preparation
- Installation torque guidance
- Inspection and quality verification
All values presented represent typical engineering reference data used in bucket elevator fastener design and must be validated against project specifications, applicable standards, and operating conditions.
A. Elevator Bolt Dimension Tables
Elevator bolts used in bucket elevator systems follow dimensional conventions defined primarily by DIN 15237 and related industrial fastener specifications.
Critical geometric parameters include:
- Bolt shank diameter
- Head diameter
- Head thickness
- Square neck dimensions
- Thread length
- Standard bolt length range
The head diameter is intentionally larger than conventional fasteners to distribute bearing pressure across the bucket wall surface.
Standard Elevator Bolt Dimensions
| Bolt Diameter | Head Diameter | Head Thickness | Square Neck Size | Thread Length | Standard Length Range |
|---|---|---|---|---|---|
| M6 | 16 mm | 3 mm | 6 mm | 12 mm | 20–60 mm |
| M8 | 22 mm | 4 mm | 8 mm | 16 mm | 25–80 mm |
| M10 | 28 mm | 5 mm | 10 mm | 20 mm | 30–100 mm |
| M12 | 35 mm | 6 mm | 12 mm | 25 mm | 40–120 mm |
| M16 | 45 mm | 8 mm | 16 mm | 35 mm | 50–160 mm |
| M20 | 55 mm | 10 mm | 20 mm | 45 mm | 70–200 mm |
Dimensional values may vary depending on:
- Bucket wall thickness
- Conveyor belt thickness
- Washer diameter requirements
- OEM design specifications
For heavy-duty bucket elevators used in mining and cement plants, larger diameters such as M16 and M20 are commonly used.
B. Mechanical Strength Table
The mechanical strength of elevator bolts depends on the material grade and heat treatment condition.
The table below presents typical mechanical property values used in industrial fastener engineering.
| Grade | Yield Strength | Tensile Strength | Approx. Shear Strength |
|---|---|---|---|
| ASTM A307 | 240 MPa | 415 MPa | ~250 MPa |
| ASTM A449 | 380 MPa | 620 MPa | ~370 MPa |
| ASTM A193 B7 | 720 MPa | 860 MPa | ~515 MPa |
| Stainless Steel B8 | 205 MPa | 515 MPa | ~300 MPa |
| Stainless Steel B8M | 205 MPa | 515 MPa | ~300 MPa |
Shear strength values are typically approximated as:
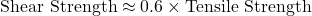
This approximation is commonly used for engineering design calculations involving bolt shear loads.
C. Torque Chart for Elevator Bolts
Correct tightening torque is essential for establishing proper bolt preload and preventing joint loosening under vibration.
Torque values depend on:
- Bolt diameter
- Material grade
- Surface condition
- Lubrication
The following table provides reference torque values for common elevator bolt sizes.
Torque Values for Metric Elevator Bolts
| Bolt Size | Grade | Dry Torque (Nm) | Lubricated Torque (Nm) |
|---|---|---|---|
| M8 | Class 4.6 | 18 | 14 |
| M8 | Class 8.8 | 32 | 24 |
| M10 | Class 4.6 | 36 | 27 |
| M10 | Class 8.8 | 65 | 49 |
| M12 | Class 4.6 | 62 | 46 |
| M12 | Class 8.8 | 110 | 82 |
| M16 | Class 4.6 | 150 | 112 |
| M16 | Class 8.8 | 270 | 200 |
| M20 | Class 4.6 | 300 | 225 |
| M20 | Class 8.8 | 520 | 390 |
| M20 | ASTM A193 B7 | 610 | 460 |
Actual installation torque must account for:
- Washer friction
- Surface coatings
- Nut type
- Lubrication condition
D. Preload Calculation Guide
Proper bolt preload ensures that the bucket and conveyor belt assembly remain securely clamped during operation.
Preload generates the clamping force required to prevent joint separation under dynamic loads.
Bolt Preload Formula
The approximate bolt preload is calculated using:

Where:
F = Bolt preload force
T = Applied torque
K = Torque coefficient (typically 0.18–0.25)
d = Bolt nominal diameter
This relationship provides an estimate of clamping force generated during tightening.
Bolt Stress Formula
The tensile stress in the bolt under axial loading is calculated as:
Where:
σ = Tensile stress
F = Axial force
A = Tensile stress area of bolt
Bolt stress must remain below the allowable material stress limit.
Shear Load Calculation
When buckets carry heavy material loads, bolts may experience shear forces.
Shear stress is calculated using:

Where:
τ = Shear stress
V = Applied shear force
A = Bolt cross-sectional area
Proper bolt sizing ensures that shear stress remains within acceptable limits.
Example Engineering Calculation
Consider the following system parameters:
Bucket load = 350 N
Number of bolts per bucket = 4
Bolt diameter = M10
Load per bolt:
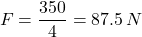
Cross-sectional area of M10 bolt ≈ 58 mm²
Tensile stress:


This stress is significantly below the allowable stress for typical fastener materials, providing adequate safety margin.
In real applications, engineers must also consider:
- Dynamic load amplification
- Impact loading during filling
- Fatigue cycles
Safety factors are therefore incorporated into system design.
E. Mechanical Property Table
The following table summarizes typical mechanical properties of materials used in elevator bolts.
| Material Grade | Yield Strength | Tensile Strength | Elongation | Hardness | Impact Resistance |
|---|---|---|---|---|---|
| ASTM A307 | 240 MPa | 415 MPa | 20% | 120–180 HB | Moderate |
| ASTM A449 | 380 MPa | 620 MPa | 18% | 22–30 HRC | Moderate |
| ASTM A193 B7 | 720 MPa | 860 MPa | 16% | 28–35 HRC | High |
| SS304 (B8) | 205 MPa | 515 MPa | 30% | 150–200 HB | High |
| SS316 (B8M) | 205 MPa | 515 MPa | 30% | 150–200 HB | High |
Mechanical properties determine the bolt’s suitability for specific operating environments.
F. Corrosion Resistance Comparison Table
Elevator bolts operating in industrial environments may be exposed to moisture, chemicals, or abrasive materials.
Material selection must therefore consider corrosion resistance.
Corrosion Performance Comparison
| Material | Marine Environment | High Humidity | Chemical Exposure | Fertilizer Handling | Grain Processing |
|---|---|---|---|---|---|
| Carbon Steel | Low | Low | Low | Low | Moderate |
| Carbon Steel (Galvanized) | Moderate | Moderate | Low | Moderate | Moderate |
| Stainless Steel 304 | High | High | Moderate | High | High |
| Stainless Steel 316 | Very High | Very High | High | Very High | High |
| Alloy Steel B7 | Moderate | Moderate | Low | Low | Moderate |
Surface coatings significantly improve corrosion resistance for carbon steel elevator bolts.
9.Inspection & Quality Control
Quality control ensures that elevator bolts meet dimensional, mechanical, and metallurgical requirements.
Inspection procedures are conducted during:
- Raw material verification
- Manufacturing stages
- Final product testing
9.1 Positive Material Identification (PMI)
PMI testing confirms the chemical composition of the fastener material.
Testing methods include:
- X-ray fluorescence (XRF)
- Optical emission spectroscopy
PMI ensures compliance with specified grades such as:
- ASTM A193 B7
- ASTM A193 B8
- ASTM A193 B8M
9.2 Hardness Testing
Hardness testing verifies proper heat treatment.
Common test methods include:
- Rockwell hardness testing
- Brinell hardness testing
Hardness values must remain within specified limits for the material grade.
9.3 Dimensional Inspection
Dimensional checks verify compliance with DIN or project specifications.
Inspection parameters include:
- Bolt length
- Head diameter
- Head thickness
- Square neck dimensions
- Thread length
Precision instruments used include:
- Vernier calipers
- Micrometers
- Optical comparators
9.4 Thread Gauge Inspection
Thread accuracy is verified using:
- Go gauges
- No-go gauges
This ensures proper fit with mating nuts.
9.5 Mechanical Testing
Mechanical testing verifies:
- Tensile strength
- Yield strength
- Elongation properties
Testing is performed using calibrated universal testing machines.
9.6 Coating Thickness Testing
Surface coatings such as galvanizing or zinc plating are verified using:
- Magnetic thickness gauges
- Coating adhesion tests
These tests ensure adequate corrosion protection.
9.7 Third-Party Inspection (TPI)
Industrial projects frequently require inspection by independent agencies.
Third-party inspectors verify:
- Manufacturing process compliance
- Dimensional accuracy
- Material traceability
- Mechanical test reports
Certification Documentation
Typical certification provided includes:
EN 10204 3.1 Material Test Certificate
This certificate includes:
- Material composition
- Mechanical test results
- Heat number traceability
- Inspection records
For critical projects, EN 10204 3.2 certification may be required with third-party validation.
10.Industrial Applications, Global Supply Capability, Procurement Guidance & Engineering Integration
This final section completes the engineering documentation for Elevator Bolts used in bucket elevator assemblies within industrial bulk material handling systems.
The following content covers:
- Industrial sectors utilizing bucket elevator fastening systems
- Integration within material transport infrastructure
- Global export and logistics capability
- Procurement and installation practices
- Inspection and maintenance guidance
- Custom engineering solutions for OEM and EPC projects
11. Industries Served
Bucket elevator systems are used in a wide range of industries requiring vertical transport of granular, powdered, or bulk solid materials.
In each of these systems, Elevator Bolts provide the primary mechanical interface between the bucket body and the conveyor belt, ensuring secure attachment during continuous material transport.
11.1 Grain Processing Facilities
Grain elevators are among the most common applications for elevator bolts.
These systems are used in:
- Wheat storage terminals
- Corn processing plants
- Rice milling operations
- Agricultural grain handling facilities
Grain handling systems typically operate at high capacity and continuous duty cycles. The fastening system must maintain integrity under:
- Repetitive loading cycles
- Dust exposure
- Vibration from rotating machinery
Elevator bolts used in grain systems typically utilize:
- Carbon steel fasteners with protective coatings
- Stainless steel variants in food-grade environments
11.2 Cement Manufacturing Plants
Cement plants require bucket elevators for vertical transport of materials such as:
- Limestone
- Clinker
- Raw meal
- Cement powder
These materials are highly abrasive and can generate significant wear within the conveyor system.
Elevator bolts used in cement plants must provide:
- High mechanical strength
- Abrasion resistance
- Secure bucket retention under heavy load conditions
Common bolt materials used include:
- ASTM A449 carbon steel
- Alloy steel grades such as ASTM A193 B7
Protective coatings may include galvanizing or phosphate coatings.
11.3 Mining Operations
Mining facilities use bucket elevators to transport materials such as:
- Iron ore fines
- Copper concentrate
- Coal
- Mineral aggregates
Mining conveyor systems operate under harsh mechanical conditions including:
- Impact loading
- High vibration
- Continuous operation
Elevator bolts used in mining environments require:
- High tensile strength
- Fatigue resistance
- Strong clamping capability
Alloy steel fasteners with heat treatment are commonly used.
11.4 Fertilizer Processing Plants
Fertilizer manufacturing facilities transport materials including:
- Ammonium nitrate
- Potash
- Phosphate granules
These materials may expose fasteners to chemical environments and moisture.
Elevator bolts used in fertilizer plants often require:
- Corrosion-resistant coatings
- Stainless steel construction
SS304 or SS316 bolts are commonly used when chemical exposure is significant.
11.5 Power Plant Coal Handling Systems
Coal-fired power plants rely on conveyor systems to move coal from storage yards to combustion units.
Bucket elevators in these systems transport coal vertically through enclosed casings.
Elevator bolts must withstand:
- Continuous vibration
- Abrasive coal dust
- Variable loading conditions
Carbon steel or alloy steel bolts with corrosion protection coatings are typically used.
11.6 Aggregate Processing Plants
Aggregate plants process materials such as:
- Crushed stone
- Sand
- Gravel
These systems involve abrasive materials that place high stress on conveyor components.
Elevator bolts must provide:
- Reliable fastening strength
- Resistance to wear and impact loads
- Long-term operational stability
11.7 Steel Industry Material Conveyors
Steel manufacturing plants utilize bucket elevators for transporting raw materials such as:
- Iron ore pellets
- Coke
- Limestone
These environments involve elevated temperatures and heavy mechanical loads.
Alloy steel elevator bolts are commonly selected due to their high strength and fatigue resistance.
12. System Integration in Bucket Elevators
Elevator bolts function as a structural interface between three components:
- Elevator bucket
- Conveyor belt
- Nut and washer assembly
The fastener system must maintain alignment and clamping force throughout continuous operational cycles.
Important design considerations include:
- Belt thickness compatibility
- Bucket wall thickness
- Bolt diameter selection
- Washer bearing surface area
Proper integration ensures that material loads are evenly distributed across the belt structure.
13. Export Capability & Global Supply
Super Industries supplies Elevator Bolts for industrial fastener requirements across international markets supporting EPC contractors, OEM equipment manufacturers, and project procurement teams.
Export operations support bulk fastener supply for large-scale infrastructure and industrial installations.
13.1 Regions Served
Industrial fasteners are supplied to projects across multiple geographic regions including:
- United States
- Europe
- Middle East
- Southeast Asia
- Africa
These markets include large-scale projects in sectors such as:
- Cement manufacturing
- Mining infrastructure
- Grain storage terminals
- Power generation facilities
13.2 Export Packaging
Industrial fasteners for international shipment are packaged to ensure protection against corrosion, contamination, and mechanical damage during transit.
Packaging methods include:
- Wooden export crates
- Industrial palletized packaging
- Moisture-resistant bagging
- Corrosion protection liners
Packaging specifications are prepared according to project documentation and export logistics requirements.
13.3 Container Loading & Logistics
Bulk shipments of elevator bolts are typically transported using standard shipping containers.
Logistics planning considers:
- Weight distribution
- Pallet stacking configuration
- Container capacity utilization
Documentation for export shipments typically includes:
- Commercial invoice
- Packing list
- Material test certificates
- Certificate of origin
These documents support customs clearance and project procurement verification.
14. Procurement & Installation Guidance
Proper installation of elevator bolts is essential to ensure reliable bucket elevator operation.
The fastening system must provide sufficient clamping force to prevent bucket movement while avoiding excessive stress on the conveyor belt.
14.1 Bucket Installation Sequence
Typical bucket installation steps include:
- Position bucket against conveyor belt
- Align bolt holes in bucket and belt
- Insert elevator bolts from inside bucket
- Install washer on belt side
- Thread nut onto bolt
- Apply specified tightening torque
Correct alignment ensures proper load distribution across the bucket mounting interface.
14.2 Washer Placement
Washers perform several mechanical functions:
- Distribute clamping force across belt surface
- Prevent local deformation of belt material
- Reduce friction between nut and belt
Washers used with elevator bolts typically have larger diameters than standard washers to increase load distribution.
14.3 Nut Locking Methods
To prevent loosening during operation, several locking methods may be used:
- Nylon insert lock nuts
- Prevailing torque lock nuts
- Double nut configurations
- Thread locking compounds
Selection depends on system vibration levels and maintenance requirements.
14.4 Tightening Procedure
Bolts should be tightened using calibrated torque tools.
Important considerations include:
- Uniform torque application across all bolts
- Avoiding over-tightening which may damage the belt
- Ensuring sufficient preload to prevent joint separation
Torque values should follow engineering specifications or the reference torque charts provided earlier.
15. Inspection & Maintenance Practices
Regular inspection of elevator bolt assemblies ensures long-term operational reliability.
15.1 Inspection Checkpoints
Routine inspection should include verification of:
- Bolt head condition
- Nut tightness
- Washer integrity
- Belt surface condition around fasteners
Any signs of bolt loosening or deformation should be addressed immediately.
15.2 Replacement Guidelines
Elevator bolts should be replaced if any of the following conditions are observed:
- Visible corrosion damage
- Thread wear or deformation
- Head cracking or deformation
- Loss of clamping force
Replacement bolts must match original specifications including:
- Diameter
- Length
- Material grade
- Surface coating
15.3 Maintenance Intervals
Inspection frequency depends on operating conditions.
Typical intervals include:
- Monthly inspection for heavy-duty mining conveyors
- Quarterly inspection for grain elevators
- Scheduled maintenance during plant shutdowns
Preventive maintenance helps avoid unexpected conveyor failures.
16. Custom Engineering Capabilities
Industrial bucket elevator systems often require fasteners with dimensions or performance characteristics outside standard specifications.
Super Industries manufactures custom-engineered elevator bolts to meet project-specific requirements.
16.1 Non-Standard Head Diameters
Certain bucket designs require larger head diameters to improve bearing surface area.
Custom head dimensions may be produced to match OEM bucket specifications.
16.2 Custom Bolt Lengths
Bucket elevators may use belts of varying thicknesses.
Custom bolt lengths ensure correct thread engagement when accounting for:
- Bucket wall thickness
- Conveyor belt thickness
- Washer thickness
16.3 High-Strength Fastener Variants
High-capacity bucket elevators used in mining or cement plants may require fasteners with increased tensile strength.
Alloy steel materials with controlled heat treatment may be used to meet these requirements.
16.4 Specialized Surface Coatings
For installations exposed to corrosive environments, specialized coatings may be applied including:
- Hot dip galvanizing
- PTFE coatings
- Phosphate coatings
- Mechanical galvanizing
These coatings improve corrosion resistance and extend fastener service life.
Conclusion
Elevator bolts are specialized fasteners designed specifically for bucket elevator fastening systems used in industrial bulk material handling applications.
Their design differs from conventional bolts due to the operational requirements of conveyor systems, including:
- Flush internal bucket surfaces
- Wide bearing surfaces for load distribution
- Resistance to vibration and cyclic loading
- Protection of conveyor belts from localized stress damage
Proper selection of bolt diameter, material grade, heat treatment, and surface coating ensures reliable performance in environments such as grain elevators, cement plants, mining facilities, and power plant material handling systems.
Through adherence to international standards, controlled manufacturing processes, dimensional inspection, and mechanical testing, elevator bolts can meet the technical requirements expected in EPC contractor specifications and industrial equipment installations.