SPADE BLANK SPACERS
“Global Manufacturer of Heavy & Custom Engineered Fasteners for Oil & Gas, Power & EPC Contractors.”
1. Industry Context & System Relevance
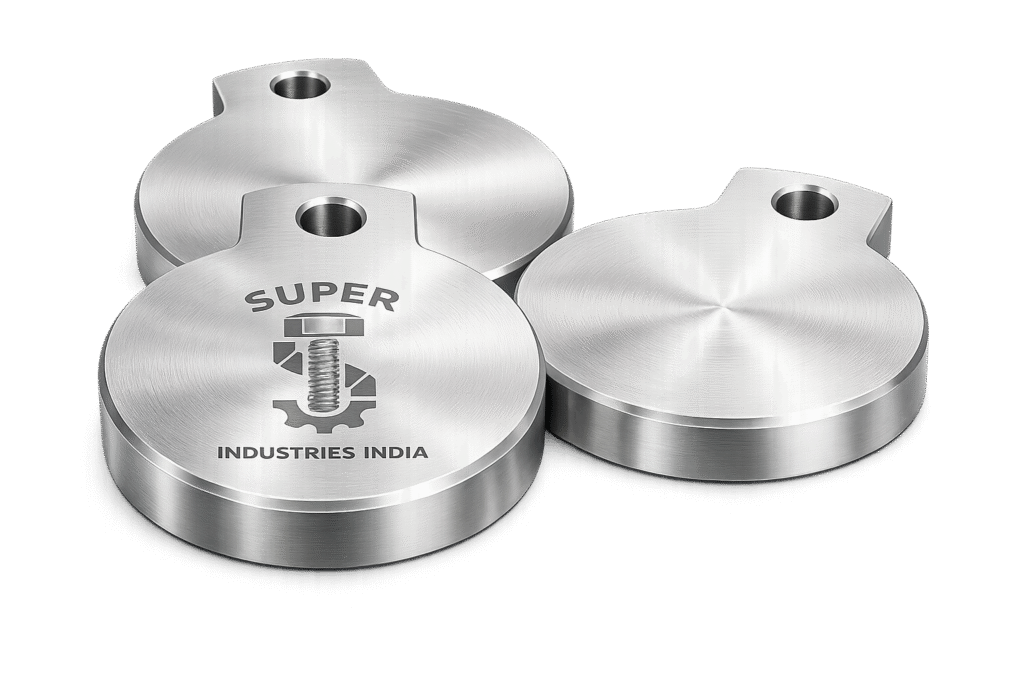
Spade Blank Spacers are critical components within pipeline isolation systems, engineered to provide positive, verifiable, and fail-safe isolation in pressurized piping networks. Their role becomes particularly significant in shutdown, turnaround (TAR), and maintenance operations, where process integrity and personnel safety depend on absolute flow isolation.
In complex process facilities, reliance on valve isolation alone introduces uncertainty due to:
- Potential internal leakage (passing valves)
- Seal degradation over time
- Mechanical failure or incomplete closure
- Absence of visual confirmation
For this reason, positive isolation using physical barriers—such as spade blanks—is mandated in many operating procedures and international safety standards.
Functional Role in Pipeline Systems
Spade Blank Spacers are deployed to:
- Physically block fluid flow in pipelines
- Enable safe maintenance and inspection activities
- Provide double-block assurance when used alongside valves
- Ensure zero-energy state conditions in hazardous systems
They are typically installed between flanged joints, replacing or supplementing gaskets depending on the operational requirement.
Application Across Industrial Sectors
Spade Blank Spacers are used extensively in the following sectors:
Oil & Gas (Upstream & Midstream)
- Wellhead isolation
- Pipeline maintenance
- Pigging operations
Refineries
- Unit shutdown isolation
- Reactor inlet/outlet blocking
- Heat exchanger maintenance
Petrochemical Plants
- Process line isolation
- Batch system segregation
- Hazardous chemical containment
Power Generation
- Steam line isolation
- Boiler maintenance
- Turbine system shutdown
LNG Terminals
- Cryogenic pipeline isolation
- Transfer line shutdowns
- Storage tank safety isolation
Offshore Installations
- Compact piping system isolation
- Maintenance under constrained environments
- Safety-critical hydrocarbon containment
Chemical Processing
- Corrosive media isolation
- Process changeover
- Cleaning and flushing operations
Why Positive Isolation is Mandatory
Positive isolation using Spade Blank Spacers is required over valve isolation due to:
| Isolation Method | Risk Level | Verification | Leakage Potential |
|---|---|---|---|
| Valve Isolation | Medium to High | Indirect | Possible |
| Double Valve + Bleed | Reduced | Moderate | Possible |
| Spade Blank Isolation | Zero (Design Basis) | Direct Visual | None |
Key Engineering Justifications:
- Provides absolute mechanical separation of process fluid
- Eliminates dependence on valve sealing integrity
- Enables visual confirmation of isolation status
- Meets lock-out/tag-out (LOTO) safety procedures
- Required in hazardous service lines (toxic, flammable, high-pressure)
2. Technical Definition
A Spade Blank Spacer is a line isolation device designed to be installed between flanged joints to either:
- Completely block flow (Spade)
- Allow unrestricted flow (Spacer)
It forms part of a broader assembly known as a Spectacle Blind System, widely used in piping systems governed by ASME B16.48.
Core Components
Spade (Solid Plate)
- A solid circular plate
- Installed between flanges to block flow completely
- Designed to withstand full line pressure
- Functions as a positive isolation barrier
Spacer (Ring Type)
- A ring-shaped plate with central opening
- Matches pipe internal diameter
- Allows normal process flow
- Used when the line is in operational condition
Spectacle Blind Configuration
A spectacle blind integrates both spade and spacer into a single unit, connected by a metal ligament.
Configuration Features:
- One side: Solid disc (spade)
- Other side: Open ring (spacer)
- Connected via handle/bridge section
- Rotated to switch between isolation and flow
Paddle Blinds (Alternative Configuration)
In larger sizes or higher pressure classes, separate paddle blinds are used:
- Independent spade and spacer plates
- Installed individually as required
- Require complete flange separation for changeover
Functional Classification
| Type | Function | Usage |
|---|---|---|
| Spade | Blocks flow | Maintenance / shutdown |
| Spacer | Allows flow | Normal operation |
| Spectacle Blind | Dual function | Frequent switching |
| Paddle Blind | Separate units | Large size / heavy-duty systems |
Temporary vs Permanent Isolation
Temporary Isolation
- Used during maintenance or inspection
- Removed after completion
- Most common application
Semi-Permanent / Operational Isolation
- Installed for extended shutdowns
- Used in commissioning or decommissioning phases
Visual Verification Advantage
One of the defining engineering advantages:
- The handle orientation provides clear visual indication:
- Handle aligned with pipe → Spacer (flow open)
- Handle perpendicular → Spade (flow blocked)
This eliminates ambiguity and supports:
- Operational safety audits
- Shift handover verification
- Regulatory compliance inspections
Super Industries
Global Manufacturer of Heavy & Custom Engineered Fasteners & Flanges
3. Engineering & Sealing Principle
The performance of Spade Blank Spacers is governed by flange mechanics, bolt preload, and gasket compression behavior under pressure.
Flange Bolting Load Transfer
When installed, the assembly consists of:
- Two flanges
- Bolting system (studs/nuts)
- Gasket (in most cases)
- Spade or spacer
Upon tightening:
- Bolts are tensioned → generating axial preload force
- This preload compresses the gasket and clamps the spade/spacer
- Load is distributed across the flange faces
Gasket Compression Interaction
In both configurations:
With Spacer (Flow Condition)
- Gasket seals against flange faces
- Spacer maintains internal diameter continuity
- Minimal disturbance to flow
With Spade (Isolation Condition)
- Gasket seals against:
- Flange face
- Flat surface of spade
- Entire pressure load is resisted by:
- Spade plate
- Bolt preload
- Gasket sealing stress
Sealing Interface Behavior
Key interfaces:
- Flange face ↔ Gasket
- Gasket ↔ Spade/Spacer surface
Engineering considerations:
- Surface flatness
- Surface finish (Ra value)
- Gasket type compatibility (spiral wound, RTJ, etc.)
- Bolt preload uniformity
Pressure Containment with Spade
When the spade is installed:
- Internal pressure acts on the full area of the blind plate
- Generates:
- Axial force
- Bending stress in the plate
The spade must:
- Resist deformation under pressure
- Maintain seal integrity
- Prevent leakage or blowout
Bolt Preload Interaction
Bolt preload must satisfy:
- Seating stress requirement of gasket
- Opposition to internal pressure force
- Maintenance of contact pressure under operating conditions
If preload is insufficient:
- Gasket relaxation → leakage
- Joint separation under pressure
If excessive:
- Bolt yielding
- Gasket crushing
Load Distribution Across Blind
Load path:
- Internal pressure → acts on spade surface
- Force transferred to flange faces
- Bolts resist separation
Uniform load distribution depends on:
- Bolt pattern symmetry
- Controlled tightening sequence
- Proper lubrication
Effect of Thickness on Sealing
Spade thickness directly influences:
- Flexural rigidity
- Deflection under pressure
- Contact pressure retention
Thin plates:
- Higher deflection
- Risk of leakage
Thick plates:
- Improved stiffness
- Higher safety margin
- Increased weight and handling requirements
Leak-Tight Isolation vs Flow Condition
| Condition | Component Installed | Engineering Behavior |
|---|---|---|
| Flow Mode | Spacer | Hydraulic continuity, minimal disturbance |
| Isolation Mode | Spade | Full pressure retention, zero flow |
Critical Requirement:
Spade Blank Spacers must ensure:
Zero-leak, full-pressure isolation under design conditions
Summary of Engineering Behavior
Spade Blank Spacers operate based on:
- Mechanical blocking (solid plate)
- Controlled sealing (gasket + bolt preload)
- Structural resistance (plate thickness + material strength)
- System compatibility (flange standards)
4. Applicable Standards (ASTM / ASME / DIN / EN / ISO)
The design, manufacture, and application of Spade Blank Spacers are governed by a structured framework of international standards to ensure dimensional compatibility, pressure integrity, and material reliability.
Primary Standard: ASME B16.48
ASME B16.48 is the governing specification for:
- Line blanks (spades and spacers)
- Spectacle blinds
- Paddle blinds
It defines:
- Dimensional requirements (OD, thickness, handle dimensions)
- Pressure class ratings (Class 150 to 2500)
- Tolerance limits
- Facing requirements (RF / RTJ compatibility)
Engineering Significance:
- Ensures interchangeability with standard flanges
- Provides minimum thickness requirements based on pressure class
- Defines safe handling geometry (handles, ligaments)
Flange Compatibility Standard: ASME B16.5
Spade Blank Spacers are installed between flanges conforming to ASME B16.5 (for sizes up to 24″) and ASME B16.47 (for larger diameters).
Defines:
- Flange dimensions
- Bolt circle diameter (BCD)
- Number and size of bolts
- Facing types
Engineering Relevance:
- Ensures perfect alignment and sealing interface compatibility
- Determines bolt load distribution pattern
Material Standards (ASTM)
Material selection is governed by ASTM specifications to ensure:
- Mechanical strength
- Temperature resistance
- Corrosion performance
Common applicable standards:
- ASTM A516 – Pressure vessel quality carbon steel plates
- ASTM A105 – Forged carbon steel
- ASTM A240 – Stainless steel plates (304 / 316)
- ASTM A182 – Alloy steel forgings (F11, F22)
DIN / EN Equivalents
For European and international projects:
- EN 1092-1 – Flange standard compatibility
- EN 10028 – Pressure vessel steels
- DIN 2527 – Blind flange references (dimensional correlation)
ISO References
Used in documentation alignment and export compliance:
- ISO 9001 – Quality management systems
- ISO 15649 – Piping systems (industrial applications)
Standard Mapping to Service Conditions
| Standard | Governs | Application |
|---|---|---|
| ASME B16.48 | Dimensions & pressure rating | Primary design |
| ASME B16.5 | Flange interface | Installation compatibility |
| ASTM | Material properties | Strength & durability |
| EN / DIN | European compliance | Export & EPC projects |
| ISO | Quality & documentation | Certification |
5. Material & Grade Options
Material selection for Spade Blank Spacers is driven by:
- Pressure class
- Operating temperature
- Corrosive environment
- Fluid type
Carbon Steel Grades
ASTM A516 Gr.60 / Gr.70
- Pressure vessel quality steel
- High notch toughness
- Suitable for moderate to high pressure systems
ASTM A105
- Forged carbon steel
- Used for high-pressure applications
- Better grain structure compared to plate
Stainless Steel Grades
ASTM A240 Type 304
- General corrosion resistance
- Suitable for non-chloride environments
ASTM A240 Type 316
- Enhanced corrosion resistance
- Suitable for:
- Marine environments
- Chloride exposure
- Chemical processing
Alloy Steel Grades
ASTM A182 F11
- Chromium-molybdenum alloy
- Suitable for elevated temperature service
ASTM A182 F22
- Higher strength and temperature resistance
- Used in power plants and refineries
Duplex / Super Duplex Stainless Steel
- High strength-to-weight ratio
- Excellent resistance to:
- Stress corrosion cracking
- Chloride attack
- Suitable for:
- Offshore platforms
- Seawater systems
Material Comparison Table
| Grade | Yield Strength (MPa) | Tensile Strength (MPa) | Temperature Range (°C) | Corrosion Resistance | Typical Application |
|---|---|---|---|---|---|
| ASTM A516 Gr.70 | ~260 | 485–620 | -29 to 425 | Moderate | Refineries, pressure lines |
| ASTM A105 | ~250 | 485–620 | -29 to 425 | Moderate | High-pressure piping |
| SS 304 | ~215 | 505–750 | -196 to 870 | Good | General chemical service |
| SS 316 | ~205 | 515–750 | -196 to 870 | Excellent | Marine, chemical plants |
| F11 | ~275 | 415–585 | Up to 540 | Moderate | Power plants |
| F22 | ~415 | 585–760 | Up to 600 | Moderate | High-temp systems |
| Duplex SS | ~450 | 620–880 | -50 to 300 | Very High | Offshore, seawater |
Material Selection Logic
| Condition | Recommended Material |
|---|---|
| High pressure, non-corrosive | A105 / A516 |
| High temperature | F11 / F22 |
| Marine / chloride | SS316 / Duplex |
| Cryogenic | SS304 / SS316 |
| Corrosive chemicals | SS316 / Duplex |
6. Heat Treatment Information
Heat treatment is applied to ensure:
- Mechanical strength
- Microstructural stability
- Resistance to cracking and deformation
Normalizing
- Applied to carbon steel
- Refines grain structure
- Improves uniformity
Quenching & Tempering (Q&T)
- Increases strength and toughness
- Used for:
- Alloy steels (F11, F22)
- Ensures resistance to:
- High pressure
- Cyclic loading
Solution Annealing (Stainless Steel)
- Dissolves carbides
- Improves corrosion resistance
- Prevents sensitization
Stress Relieving
- Removes residual stresses from machining or forming
- Reduces risk of distortion during service
Mechanical Property Control
Heat treatment ensures:
- Controlled hardness
- Improved ductility
- Impact resistance
Impact Testing (Charpy V-Notch)
Required for:
- Low-temperature service
- Critical applications
Measures:
- Energy absorption capacity
- Resistance to brittle fracture
Microstructure Importance
- Uniform grain structure → consistent strength
- Avoidance of:
- Carbide precipitation
- Grain boundary weakness
7. Manufacturing Process
The manufacturing of Spade Blank Spacers follows a controlled, inspection-driven workflow to ensure dimensional accuracy and pressure integrity.
Raw Material Inspection
- Verification against MTC
- Chemical composition analysis
- Visual inspection for defects
Plate Cutting / Forging
Depending on size and class:
- Plate cutting (laser / plasma / waterjet)
- Closed-die forging (for high-pressure classes)
CNC Machining
Operations include:
- OD/ID machining
- Thickness control
- Edge finishing
- Handle shaping
Ensures:
- Dimensional precision
- Surface uniformity
Edge Preparation
- Deburring
- Chamfering
- Smooth edge finishing
Prevents:
- Stress concentration
- Handling injuries
Thickness Calibration
- Precision measurement
- Compliance with ASME B16.48 tolerances
Heat Treatment (If Required)
Applied as per:
- Material grade
- Project specification
Surface Finishing
- Shot blasting
- Coating application
- Passivation (SS)
Final Inspection
Includes:
- Dimensional verification
- Surface quality check
- Marking validation
Marking & Traceability
Each Spade Blank Spacer is marked with:
- Size
- Class rating
- Material grade
- Heat number
- Manufacturer identification
Ensures:
- Full traceability
- Compliance with EPC documentation
Surface Finish Options
Surface finishing is applied based on:
- Environmental exposure
- Storage duration
- Corrosion risk
Shot Blasting
- Removes mill scale
- Improves surface uniformity
Anti-Rust Oil Coating
- Temporary corrosion protection
- Suitable for short-term storage
Industrial Painting
- Long-term protection
- Color coding possible
PTFE Coating
- Chemical resistance
- Low friction surface
Galvanizing
- Zinc coating for corrosion protection
- Suitable for outdoor environments
Passivation (Stainless Steel)
- Removes free iron
- Enhances corrosion resistance
Surface Roughness Considerations
Surface finish affects:
- Gasket seating
- Sealing integrity
Typical requirement:
- Smooth, flat contact surface
- Controlled roughness (Ra value as per gasket type)
A. Dimensional Table (Reference — ASME B16.48 Aligned)
The following table provides indicative dimensions for Spade Blank Spacers. Final values must be confirmed against ASME B16.48 and project specifications.
Units: mm (unless specified)
| Nominal Size (NPS) | Class | Thickness (t) | OD (Spade) | ID (Spacer) | Approx Weight (kg) |
|---|---|---|---|---|---|
| 2″ | 150 | 6.4 | 165 | 52 | 1.2 |
| 2″ | 300 | 9.5 | 165 | 52 | 1.8 |
| 4″ | 150 | 6.4 | 229 | 102 | 2.8 |
| 4″ | 600 | 19.0 | 229 | 102 | 7.5 |
| 6″ | 300 | 12.7 | 279 | 154 | 6.5 |
| 6″ | 900 | 31.8 | 279 | 154 | 16.8 |
| 8″ | 300 | 15.9 | 343 | 202 | 11.2 |
| 8″ | 1500 | 47.8 | 343 | 202 | 32.5 |
| 10″ | 600 | 25.4 | 406 | 254 | 21.5 |
| 12″ | 600 | 28.6 | 483 | 304 | 32.0 |
| 16″ | 300 | 31.8 | 597 | 406 | 48.5 |
| 20″ | 150 | 25.4 | 711 | 508 | 52.0 |
Engineering Notes:
- Thickness increases with pressure class
- OD corresponds to flange OD compatibility
- Spacer ID aligns with pipe bore
- Weight impacts handling and lifting requirements
B. Pressure Rating Table (ASME Class vs Pressure vs Temperature)
Indicative pressure ratings for carbon steel (ASTM A516 Gr.70):
| ASME Class | Pressure @ 38°C (bar) | Pressure @ 200°C (bar) | Pressure @ 400°C (bar) |
|---|---|---|---|
| 150 | 19.6 | 15.3 | 10.2 |
| 300 | 51.1 | 40.0 | 26.7 |
| 600 | 102.1 | 80.1 | 53.4 |
| 900 | 153.1 | 120.2 | 80.1 |
| 1500 | 255.2 | 200.3 | 133.5 |
| 2500 | 425.4 | 333.8 | 222.5 |
Engineering Interpretation:
- Pressure capacity reduces with temperature increase
- Spade must be designed for maximum design pressure
- Governs minimum thickness requirement
C. Torque Chart
Torque values for flange bolting during installation of Spade Blank Spacers.
Units: Torque in Nm (approximate, based on lubricated vs dry conditions)
| Bolt Size | Grade | Lubricated Torque (Nm) | Dry Torque (Nm) |
|---|---|---|---|
| M16 | 8.8 | 110 | 150 |
| M16 | B7 | 120 | 160 |
| M20 | 8.8 | 220 | 300 |
| M20 | B7 | 240 | 320 |
| M24 | 8.8 | 380 | 520 |
| M24 | B7 | 420 | 560 |
| M27 | 8.8 | 560 | 750 |
| M27 | B7 | 600 | 800 |
| M30 | 8.8 | 760 | 1020 |
| M30 | B7 | 820 | 1100 |
| M36 | 8.8 | 1300 | 1750 |
| M36 | B7 | 1400 | 1850 |
Torque Application Guidelines:
- Use calibrated torque wrench
- Apply cross-tightening sequence
- Perform multi-stage tightening (30% → 60% → 100%)
- Re-torque after initial pressurization
D. Preload & Stress Calculation Guide
Bolt Stress Formula
\[
\sigma_b = \frac{F_b}{A_b}
\]
Where:
- ( \sigma_b ) = Bolt stress (MPa)
- ( F_b ) = Bolt preload force (N)
- ( A_b ) = Bolt cross-sectional area (mm²)
Force on Blind Due to Internal Pressure
\[
F_p = P \times A
\]
Where:
- ( F_p ) = Force acting on spade (N)
- ( P ) = Internal pressure (MPa)
- ( A ) = Internal pipe area (mm²)
Bending Stress in Spade (Conceptual)
\[
\sigma = \frac{P \cdot D^2}{t^2}
\]
Where:
- ( D ) = Effective diameter
- ( t ) = Thickness
Sample Calculation
Given:
- Pipe Size: 6″ (ID ≈ 154 mm)
- Pressure: 10 MPa
- Area:
\[
A = \frac{\pi D^2}{4} = \frac{3.14 \times (154)^2}{4} \approx 18600 \, \text{mm}^2
\]
\[
F_p = 10 \times 18600 = 186000 \, \text{N}
\]
Interpretation:
- Spade must withstand ~186 kN force
- Bolt preload must exceed this force with safety margin
Safety Margin Philosophy
Design ensures:
- Bolt preload ≥ 1.5 × pressure force
- Plate stress < allowable stress (material dependent)
- No permanent deformation
E. Mechanical Properties Table
| Material | Yield Strength (MPa) | Tensile Strength (MPa) | Hardness (HB) | Elongation (%) | Impact (J) |
|---|---|---|---|---|---|
| A516 Gr.70 | 260 | 485–620 | 140–180 | 21 | 27 |
| A105 | 250 | 485–620 | 120–170 | 22 | 27 |
| SS304 | 215 | 505–750 | 150–200 | 40 | 50 |
| SS316 | 205 | 515–750 | 150–200 | 40 | 50 |
| F11 | 275 | 415–585 | 130–180 | 20 | 27 |
| Duplex | 450 | 620–880 | 250–300 | 25 | 60 |
F. Corrosion Resistance Comparison Table
| Material | Marine | Acidic | Hydrocarbon | High Humidity |
|---|---|---|---|---|
| Carbon Steel | Low | Low | Good | Low |
| SS304 | Moderate | Moderate | Excellent | Good |
| SS316 | Excellent | Good | Excellent | Excellent |
| Duplex SS | Excellent | Excellent | Excellent | Excellent |
| Alloy Steel (F11/F22) | Low | Low | Good | Moderate |
Engineering Interpretation:
- SS316 / Duplex preferred for aggressive environments
- Carbon steel requires coating or protection
- Alloy steel selected for temperature, not corrosion
8. Inspection & Quality Control
Inspection of Spade Blank Spacers is mandatory to ensure pressure integrity, dimensional accuracy, and material compliance.
Positive Material Identification (PMI)
- Confirms material grade
- Verifies alloy composition
Used for:
- Stainless steel
- Alloy steel
Ultrasonic Testing (UT)
- Detects internal defects
- Ensures material homogeneity
Applicable for:
- Thick plates
- High-pressure classes
Dye Penetrant Inspection (DPI)
- Surface crack detection
- Applied after machining
Magnetic Particle Inspection (MPI)
- Surface and near-surface defect detection
- Used for ferromagnetic materials
Dimensional Inspection
Checks:
- Thickness
- OD / ID
- Flatness
- Handle geometry
Tools:
- Vernier calipers
- Micrometers
- Height gauges
Hardness Testing
- Ensures compliance with material standards
- Detects improper heat treatment
Hydro Testing (Conditional)
- Not always mandatory
- Applied in critical applications
Certification
EN 10204 3.1
- Manufacturer-certified test report
EN 10204 3.2
- Third-party verified certification
Third-Party Inspection (TPI)
Conducted by:
- Client representatives
- Independent inspection agencies
Scope includes:
- Material verification
- Dimensional checks
- Documentation review
Traceability System
Each Spade Blank Spacer is traceable via:
- Heat number
- Batch number
- Material certificate
- Inspection records
9. Industries Served
Spade Blank Spacers are deployed across process industries where positive isolation, pressure containment, and maintenance safety are mandatory engineering requirements.
Upstream Oil & Gas
Applications include:
- Wellhead isolation during intervention
- Flowline shutdown for inspection
- Separation unit maintenance
Engineering Requirements:
- High-pressure resistance (Class 900–2500)
- Sour service compatibility (as applicable)
- Reliability under cyclic operations
Refineries
Used in:
- Crude distillation units (CDU)
- Hydrocrackers and reformers
- Heat exchanger isolation
Key Considerations:
- High temperature + pressure combination
- Hydrocarbon containment
- Compliance with shutdown procedures
Petrochemical Plants
Typical usage:
- Process unit isolation
- Batch line segregation
- Chemical containment during maintenance
Material selection driven by:
- Corrosion resistance
- Chemical compatibility
Power Generation Plants
Applications:
- Steam line isolation
- Boiler maintenance
- Turbine shutdown
Engineering requirements:
- High-temperature alloy steels (F11 / F22)
- Resistance to thermal expansion stress
LNG Terminals
Usage:
- Cryogenic pipeline isolation
- Transfer line shutdown
- Storage system maintenance
Material requirements:
- Low-temperature toughness
- Stainless steel or duplex grades
Offshore Platforms
Constraints:
- Limited space
- Corrosive marine environment
Applications:
- Process piping isolation
- Safety shutdown systems
Material preference:
- Duplex / Super Duplex stainless steel
Chemical Processing Industries
Used for:
- Acidic and corrosive fluid isolation
- Cleaning and flushing operations
- Process changeover
Material selection:
- SS316 / Duplex based on chemical compatibility
10. Export Capability & Global Supply
Super Industries
“Global Manufacturer of Heavy & Custom Engineered Fasteners for Oil & Gas, Power & EPC Contractors.”
Operates as a manufacturer and global exporter of Spade Blank Spacers, aligned with EPC procurement, inspection, and documentation protocols.
Export Regions
Supply capability includes:
- United States (ASME compliance)
- European Union (EN / PED alignment)
- Middle East (project-driven EPC supply)
- Southeast Asia (process industry demand)
Export Packaging Standards
Packaging is designed to ensure:
- Protection against corrosion
- Mechanical damage prevention
- Ease of handling at project sites
Typical methods:
- Wooden boxes (ISPM-15 compliant)
- Palletized packing
- Moisture barrier wrapping
- Rust preventive coatings
Documentation Package
Each shipment includes:
Material Test Certificates (MTC)
- Chemical composition
- Mechanical properties
Inspection Reports
- Dimensional verification
- NDT results
Compliance Certificates
- ASME / ASTM conformity
- Heat treatment records
Additional Documentation (Project-Specific)
- Third-party inspection reports
- Packing lists
- Traceability records
Project Logistics Capability
Capability includes:
- Bulk order handling
- Mixed-size shipment consolidation
- Project-wise tagging and identification
- Coordination with EPC contractors and logistics teams
11. PROCUREMENT & INSTALLATION VIEW
Installation Procedure for Spade Blank Spacers
Installation must follow controlled mechanical procedures to ensure sealing integrity and operational safety.
Pre-Installation Checks
- Verify:
- Size (NPS)
- Pressure class
- Material grade
- Inspect:
- Surface condition
- Flatness
- Markings and traceability
Flange Disassembly Procedure
- Depressurize and drain line
- Loosen bolts in cross pattern
- Separate flange faces using controlled methods
- Ensure no residual pressure remains
Spade / Spacer Insertion
- Insert spade or spacer between flanges
- Align with:
- Bolt holes
- Gasket seating area
Ensure:
- Proper gasket placement
- No misalignment
Follow cross-tightening pattern:
- Initial tightening (30%)
- Intermediate tightening (60%)
- Final torque (100%)
Use:
- Calibrated torque wrench
- Lubricated threads (if specified)
Re-Torque Practice
- Perform after:
- Initial pressurization
- Thermal stabilization
Ensures:
- Compensation for gasket relaxation
- Long-term sealing performance
Safety Precautions
- Confirm zero pressure condition before installation
- Use appropriate lifting equipment for large sizes
- Avoid manual handling for heavy spades
- Follow plant LOTO procedures
Tagging & Identification
Each installed unit should be:
- Tagged with:
- Isolation status (OPEN / CLOSED)
- Date of installation
- Responsible personnel
Ensures:
- Operational clarity
- Audit traceability
12. Custom Engineering Capabilities
Spade Blank Spacers can be engineered beyond standard specifications to meet project-specific requirements.
Non-Standard Sizes
- Large diameters beyond ASME range
- Custom OD/ID combinations
Increased Thickness Designs
- For:
- Higher pressure applications
- Additional safety margin
Special Handle Designs
- Reinforced handles
- Extended handles for accessibility
- Weight-reduced configurations
Exotic Material Grades
- Super Duplex (UNS S32750 / S32760)
- Nickel alloys (Inconel, Monel)
- Titanium (for specialized chemical service)
Project-Specific Marking
- Client tagging systems
- Barcode / QR traceability
- Heat number stamping
13. Engineering Compliance Summary
Spade Blank Spacers manufactured in accordance with:
- ASME B16.48 → Dimensional & pressure compliance
- ASME B16.5 → Flange compatibility
- ASTM standards → Material integrity
- EN / DIN → International project compliance
Ensure:
- Pressure containment capability
- Dimensional accuracy
- Material traceability
- Inspection readiness
Final Engineering Conclusion
Spade Blank Spacers function as critical safety components within pressurized piping systems. Their engineering significance is defined by:
- Positive isolation capability
- Zero-leak pressure containment
- Direct visual verification of line status
- Compatibility with global piping standards
They are not auxiliary accessories but pressure-retaining isolation devices that must be:
- Properly designed
- Precisely manufactured
- Correctly installed
- Fully traceable
From an EPC evaluation perspective, acceptance depends on:
- Compliance with ASME B16.48 dimensional requirements
- Verified material properties and heat treatment
- Documented inspection and testing records
- Capability to meet project-specific technical specifications
Final Technical Position
A correctly engineered and manufactured Spade Blank Spacer ensures:
Mechanical isolation independent of valve integrity, enabling safe maintenance and operational control in high-pressure piping systems.
latexpage]