BS 4504 Flanges
Super Industries
“Global Manufacturer of Heavy & Custom Engineered Fasteners for Oil & Gas, Power & EPC Contractors.”
1. Industry Context & System Relevance
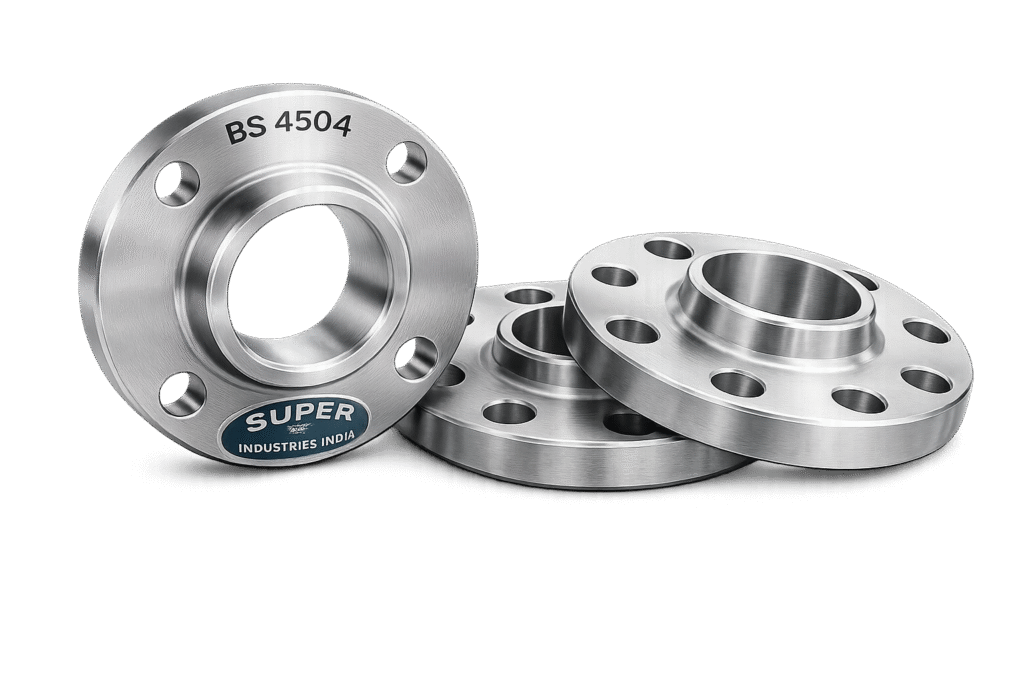
Role of BS 4504 Flanges in Pressure Piping Systems
BS 4504 Flanges are integral components within pressure-retaining piping systems, enabling mechanically bolted connections between pipes, valves, pumps, and process equipment. These flanges provide a detachable joint that maintains system integrity under internal pressure, temperature variation, and mechanical loading.
Within engineered piping systems, flanges serve three primary functional roles:
- Pressure containment interface
- Mechanical alignment and support
- Maintenance access point
Unlike permanent welded joints, flanged connections introduce controlled separability, allowing dismantling without structural damage to adjoining components.
Application Across Industrial Sectors
BS 4504 Flanges are deployed across multiple high-dependency industrial sectors:
Oil & Gas
- Upstream gathering lines
- Refinery process units
- Offshore modules
- LNG transfer systems
Refineries & Petrochemicals
- Reactor inlet/outlet lines
- Heat exchanger connections
- Storage tank nozzles
Power Generation
- Boiler feedwater systems
- Steam distribution lines
- Cooling water circuits
Water & Wastewater
- Pumping stations
- Treatment plant manifolds
- Transmission pipelines
Chemical Processing
- Corrosive fluid handling systems
- High-temperature reaction loops
Infrastructure Pipelines
- Municipal water supply
- Industrial utility corridors
Why Flanged Joints Are Preferred
In engineered systems, flanged joints are selected over welded or threaded alternatives due to:
1. Maintenance Accessibility
- Enables non-destructive disassembly
- Facilitates inspection of internal components
- Supports periodic gasket replacement
2. Alignment Flexibility
- Allows minor angular and axial adjustments
- Reduces installation stress during field fit-up
3. Equipment Interface Compatibility
- Standardized interface for pumps, valves, and vessels
- Enables modular system construction
4. Inspection & Compliance
- Visual inspection of sealing surfaces
- Ease of NDT access for bolting components
5. Replacement Efficiency
- Rapid replacement of damaged components
- Minimizes downtime in critical systems
2. Technical Definition of BS 4504 Flanges
Standardized Pressure-Retaining Components
BS 4504 Flanges are circular metallic components manufactured in accordance with the British Standard BS 4504, designed to:
- Withstand internal pressure loads
- Provide bolted mechanical connections
- Enable gasket-based sealing between mating surfaces
Core Structural Elements
A typical BS 4504 flange consists of:
- Flange ring (body)
- Bolt holes (equally spaced)
- Sealing face (FF or RF)
- Hub (for weld neck type)
- Raised or flat contact surface
PN Pressure Rating System
BS 4504 flanges are classified using the PN (Pressure Nominal) system:
| PN Rating | Pressure (Bar) | Typical Application |
|---|---|---|
| PN6 | 6 bar | Low-pressure water systems |
| PN10 | 10 bar | Utility pipelines |
| PN16 | 16 bar | General industrial service |
| PN25 | 25 bar | Process piping |
| PN40 | 40 bar | High-pressure applications |
Key Engineering Note:
PN rating represents maximum allowable pressure at ambient temperature, subject to derating at elevated temperatures.
Flange Face Types
Flat Face (FF)
- Entire flange surface is planar
- Used with full-face gaskets
- Preferred for:
- Cast iron systems
- Low-pressure applications
Raised Face (RF)
- Elevated sealing surface
- Concentrates gasket load within a defined area
- Preferred for:
- Higher pressure services
- Improved sealing efficiency
Flange Types under BS 4504
Slip-On Flange
- Pipe inserted into bore
- Fillet welded internally and externally
- Suitable for moderate pressure systems
Weld Neck Flange
- Long tapered hub
- Butt-welded to pipe
- Superior for:
- High pressure
- Cyclic loading
- Thermal expansion environments
Blind Flange
- Solid disc without bore
- Used for:
- Line termination
- Pressure testing
Plate Flange
- Flat plate machined with bolt holes
- Economical for low-pressure applications
BS 4504 vs EN 1092-1
| Parameter | BS 4504 | EN 1092-1 |
|---|---|---|
| Status | Legacy British Standard | Current European Standard |
| Dimensional Basis | Metric PN system | Metric PN system |
| Global Usage | Existing installations, legacy projects | New EPC projects |
| Interchangeability | Limited | Preferred modern standard |
Engineering Clarification:
Although EN 1092-1 has largely replaced BS 4504, BS 4504 Flanges remain relevant in:
- Brownfield upgrades
- Maintenance of legacy systems
- Projects specifying British standards
Non-Interchangeability with ASME Standards
BS 4504 flanges are not dimensionally interchangeable with ASME standards such as:
- Bolt circle diameter differences
- Bolt hole count variation
- Facing geometry mismatch
Mixing standards introduces:
- Misalignment
- Uneven gasket compression
- Potential leakage or failure
Super Industries
Global Manufacturer of Heavy & Custom Engineered Fasteners & Flanges
3. Engineering & Sealing Principle
Fundamental Sealing Mechanism
The sealing capability of BS 4504 Flanges is governed by:
Bolt-induced compressive force acting on a deformable gasket to create a pressure-tight seal
Bolt Preload Mechanics
When bolts are tightened:
- Tensile force is induced in the bolt
- Compressive force is transferred across flange faces
- Gasket is compressed between mating surfaces
This preload must:
- Exceed internal pressure forces
- Maintain sealing under operating conditions
Gasket Compression Behavior
Gaskets function by:
- Filling microscopic surface irregularities
- Creating a fluid-tight barrier
Critical parameters:
- Seating stress (initial compression)
- Operating stress retention
- Elastic recovery
Sealing Stress Requirement
To maintain sealing:
\[
\sigma_g \geq \frac{P \cdot A_i}{A_g}
\]
Where:
- ( \sigma_g ) = gasket stress
- ( P ) = internal pressure
- ( A_i ) = internal pressure area
- ( A_g ) = gasket contact area
Flange Face Finish Impact
Surface roughness directly affects sealing:
| Surface Finish (Ra) | Application |
|---|---|
| 3.2 – 6.3 µm | Soft gaskets |
| 1.6 – 3.2 µm | Metallic gaskets |
| Serrated finish | Improved grip and sealing |
Excessively smooth surfaces reduce gasket grip, while rough surfaces cause leakage paths.
Pressure Containment Theory
Internal pressure generates:
- Axial force attempting to separate flanges
- Radial stress on gasket
Bolting system must counteract:
\[
F_{bolt} \geq F_{pressure}
\]
Where:
\[
F_{pressure} = P \times A
\]
Leakage Prevention Mechanism
Leakage is prevented by:
- Maintaining sufficient gasket stress
- Preventing flange rotation
- Ensuring uniform bolt preload
- Controlling surface finish
Failure occurs when:
- Gasket stress falls below sealing threshold
- Uneven bolt tightening introduces distortion
- Thermal or cyclic loads relax preload
4. Pressure & Load Engineering
PN Rating Engineering Framework
The PN system provides a pressure classification, but actual allowable pressure depends on:
- Material strength
- Temperature
- Flange geometry
Static vs Cyclic Loading
Static Loads
- Constant pressure systems
- Predictable stress behavior
Cyclic Loads
- Pressure fluctuations
- Thermal expansion cycles
- Cause:
- Bolt fatigue
- Gasket creep relaxation
Thermal Expansion Effects
Temperature variation leads to:
- Differential expansion between:
- Pipe
- Flange
- Bolts
Consequences:
- Loss of preload
- Flange distortion
- Leakage risk
Pipeline Vibration Impact
Vibration introduces:
- Dynamic loading
- Bolt loosening risk
- Micro-movement at gasket interface
Mitigation:
- Proper torqueing
- Locking mechanisms
- Periodic inspection
Safety Factor Philosophy
Design incorporates safety factors to account for:
- Material variability
- Installation inaccuracies
- Operational uncertainties
Typical approach:
- Bolt stress below yield limit
- Gasket stress within allowable range
Gasket Seating Stress
Initial bolt tightening must achieve:
- Minimum seating stress
- Uniform compression
Insufficient seating leads to:
- Immediate leakage
- Poor long-term performance
Flange Rotation Consideration
Under load:
- Flanges tend to rotate about gasket centerline
- Causes:
- Uneven gasket stress
- Edge leakage
Design controls:
- Flange thickness
- Bolt spacing
- Hub reinforcement (for weld neck)
Dimensional & Design Logic
Critical Dimensional Parameters
Bolt Circle Diameter (BCD)
- Defines bolt positioning
- Ensures uniform load distribution
Number of Bolt Holes
- Increases with diameter and pressure rating
- Balances load per bolt
Flange Thickness
- Controls resistance to bending and rotation
Hub Dimensions (Weld Neck)
- Provides stress transition
- Reduces fatigue concentration
Face Geometry
- Flatness tolerance critical for sealing
- Parallelism between mating faces required
Tolerance & Geometric Controls
| Parameter | Control Requirement |
|---|---|
| Flatness | Within specified microns |
| Concentricity | Bore aligned with bolt circle |
| Parallelism | Uniform face alignment |
| Bolt hole alignment | Accurate spacing |
Engineering Outcome
Proper dimensional control ensures:
- Uniform bolt preload
- Stable gasket compression
- Long-term sealing reliability
5. Applicable Standards (CRITICAL SECTION)
Primary Standard — BS 4504
BS 4504 Flanges are manufactured in accordance with British Standard BS 4504, which defines:
- PN pressure rating classification (PN6 to PN40)
- Dimensional requirements:
- Outside diameter
- Bolt circle diameter (BCD)
- Number and size of bolt holes
- Flange thickness
- Facing types (Flat Face / Raised Face)
- Tolerance limits for machining and geometry
This standard establishes dimensional uniformity and interchangeability within systems designed under British engineering practice.
EN 1092-1 (Modern Equivalent)
EN 1092-1 represents the current European standard replacing BS 4504 in most new EPC projects.
| Parameter | BS 4504 | EN 1092-1 |
|---|---|---|
| Standard Origin | British | European (EN) |
| Dimensional Structure | Metric PN | Metric PN |
| Usage | Legacy / existing systems | New design & EPC projects |
| Interchangeability | Limited | Preferred |
Engineering Note:
While dimensions are often similar, full interchangeability is not guaranteed due to:
- Facing differences
- Tolerance variations
- Updated material requirements
DIN Flange Standards
DIN standards (e.g., DIN 2501, now largely superseded by EN 1092-1) historically align with:
- Metric PN classification
- Similar dimensional philosophy
BS 4504 flanges may interface with DIN systems only after dimensional verification.
ASTM Material Standards
Material compliance for BS 4504 Flanges is governed by ASTM specifications:
- ASTM A105 — Carbon steel forgings
- ASTM A350 LF2 — Low-temperature carbon steel
- ASTM A182 F304 / F316 — Stainless steel
- ASTM A182 F11 / F22 — Alloy steel
- Duplex grades — As per ASTM A182 / A240
These standards define:
- Mechanical properties
- Chemical composition
- Heat treatment conditions
- Testing requirements
Comparison with ASME B16.5
| Parameter | BS 4504 | ASME B16.5 |
|---|---|---|
| Pressure System | PN (metric) | Class (150–2500) |
| Dimensions | Metric | Inch-based |
| Bolt Patterns | Different | Different |
| Interchangeability | Not compatible | Not compatible |
Critical Engineering Statement:
BS 4504 flanges must not be interchanged with ASME B16.5 flanges due to:
- Bolt misalignment
- Sealing failure risk
- Non-uniform load distribution
Standards Mapping for Engineering Selection
| Requirement | Applicable Standard |
|---|---|
| Dimensional control | BS 4504 |
| Modern compliance | EN 1092-1 |
| Material specification | ASTM |
| Pressure system reference | PN rating |
| Inspection certification | EN 10204 |
6. Material & Grade Options
Material selection for BS 4504 Flanges is governed by:
- Pressure rating (PN class)
- Operating temperature
- Corrosive environment
- Mechanical loading conditions
Carbon Steel Grades
ASTM A105
- Standard forging grade
- Suitable for:
- Ambient to moderate temperatures
- Non-corrosive environments
- High strength and machinability
ASTM A350 LF2
- Low-temperature carbon steel
- Improved notch toughness
- Suitable for:
- Sub-zero service
- Cryogenic-adjacent applications
Stainless Steel Grades
ASTM A182 F304
- General-purpose stainless steel
- Good corrosion resistance
- Suitable for:
- Water systems
- Mild chemical exposure
ASTM A182 F316
- Molybdenum-enhanced stainless steel
- Improved resistance to:
- Chlorides
- Marine environments
- Preferred in:
- Offshore systems
- Chemical processing
Alloy Steel Grades
ASTM A182 F11 / F22
- Chromium-molybdenum alloy steels
- High-temperature strength
- Used in:
- Power plants
- Steam systems
Duplex & Super Duplex Stainless Steel
- Dual-phase microstructure (austenitic + ferritic)
- High strength and corrosion resistance
- Excellent for:
- Seawater exposure
- Aggressive chemical environments
Material Comparison Table)
| Grade | Yield Strength (MPa) | Tensile Strength (MPa) | Temperature Range | Corrosion Resistance | Typical Industry Use |
|---|---|---|---|---|---|
| ASTM A105 | ~250 | 485–620 | -20°C to 425°C | Low | Oil & gas, general piping |
| ASTM A350 LF2 | ~250 | 485–620 | -46°C to 400°C | Low | Low-temperature service |
| F304 | ~205 | 515–720 | -196°C to 870°C | Moderate | Water, chemicals |
| F316 | ~205 | 515–720 | -196°C to 870°C | High | Marine, chemical |
| F11 | ~275 | 415–585 | Up to 550°C | Moderate | Power plants |
| F22 | ~415 | 585–760 | Up to 600°C | Moderate | High-temp service |
| Duplex | ~450 | 620–880 | -50°C to 300°C | Very High | Offshore, desalination |
7. Heat Treatment Information
Heat treatment is applied to achieve:
- Required mechanical properties
- Microstructural stability
- Residual stress reduction
Common Heat Treatment Processes
Normalizing
- Heating above critical temperature
- Air cooling
- Refines grain structure
- Improves uniformity
Quenching & Tempering
- Rapid cooling (quenching)
- Followed by reheating (tempering)
- Enhances:
- Strength
- Toughness
- Used for alloy steels
Solution Annealing (Stainless Steel)
- Heating to high temperature
- Rapid cooling
- Restores corrosion resistance
- Dissolves carbides
Stress Relieving
- Low-temperature heat treatment
- Reduces residual stresses from:
- Forging
- Machining
Mechanical Property Control
| Property | Controlled By |
|---|---|
| Hardness | Heat treatment cycle |
| Grain size | Cooling rate |
| Toughness | Tempering |
| Ductility | Annealing |
Hardness Ranges (Typical)
- Carbon steel: 120–200 HB
- Alloy steel: 150–250 HB
- Stainless steel: 150–220 HB
Impact Testing (Charpy V-Notch)
Applied for:
- Low-temperature applications
- Critical pressure systems
Ensures:
- Resistance to brittle fracture
- Compliance with project specifications
8. Manufacturing Process
Manufacturing of BS 4504 Flanges follows a controlled, traceable sequence to ensure dimensional accuracy and mechanical integrity.
Step-by-Step Process Flow
1. Raw Material Inspection
- Verification of:
- Mill Test Certificates (MTC)
- Chemical composition
- Identification marking for traceability
2. Forging / Plate Cutting
Forged Flanges:
- Billet heating
- Closed-die or open-die forging
- Grain flow aligned with geometry
Plate Flanges:
- CNC profile cutting from plate
- Used for lower pressure classes
3. Heat Treatment (Initial)
- Applied post-forging
- Ensures uniform structure
4. CNC Machining
- Turning operations:
- Outer diameter
- Bore diameter
- Machining tolerances maintained
5. Drilling
- Bolt holes drilled using CNC indexing
- Ensures:
- Accurate pitch circle
- Angular spacing
6. Facing Operation
- Machining of sealing surface:
- Flat Face or Raised Face
- Surface finish controlled (Ra values)
7. Secondary Heat Treatment
- As per material specification
- Final mechanical property adjustment
8. Surface Coating / Treatment
- Application based on material and environment
9. Final Inspection
- Dimensional verification
- NDT testing (as required)
10. Marking & Traceability
- Heat number
- Material grade
- Size and PN rating
- Manufacturer identification
Surface Finish Options
Surface finish impacts:
- Corrosion resistance
- Gasket sealing performance
Available Surface Treatments
Anti-Rust Oil Coating
- Temporary protection
- Used for carbon steel during storage
Black Coating
- Oxide layer formation
- Moderate corrosion resistance
Zinc Plating
- Electroplated zinc layer
- Protection in humid environments
Hot-Dip Galvanizing
- Thick zinc coating
- Suitable for:
- Outdoor exposure
- Water systems
Passivation (Stainless Steel)
- Chemical treatment
- Removes free iron
- Enhances corrosion resistance
Surface Roughness (Ra Values)
| Finish Type | Ra Value | Application |
|---|---|---|
| Smooth finish | 1.6–3.2 µm | Metallic gaskets |
| Serrated finish | 3.2–6.3 µm | Soft gaskets |
| Rough finish | >6.3 µm | Limited use |
Gasket Seating Implications
- Lower Ra → better for metallic gaskets
- Higher Ra → better grip for soft gaskets
- Incorrect finish → leakage risk
A. Technical Dimension Tables — BS 4504 Flanges
The following table provides representative dimensional data for BS 4504 Flanges across common DN sizes and PN ratings. Final dimensions must always be verified against project specifications and approved drawings.
Table A1 — Dimensional Reference (PN16 Series)
| DN (mm) | Outside Diameter (mm) | BCD (mm) | Bolt Holes | Bolt Size | Flange Thickness (mm) |
|---|---|---|---|---|---|
| 15 | 95 | 65 | 4 | M12 | 12 |
| 25 | 115 | 85 | 4 | M12 | 14 |
| 50 | 165 | 125 | 4 | M16 | 16 |
| 80 | 200 | 160 | 8 | M16 | 18 |
| 100 | 220 | 180 | 8 | M16 | 18 |
| 150 | 285 | 240 | 8 | M20 | 20 |
| 200 | 340 | 295 | 12 | M20 | 22 |
| 300 | 455 | 410 | 12 | M24 | 28 |
| 400 | 580 | 525 | 16 | M27 | 32 |
| 600 | 840 | 770 | 20 | M33 | 36 |
Engineering Observations
- Increase in bolt count and diameter ensures uniform load distribution
- Flange thickness increases to resist bending and rotation
- BCD growth maintains bolt stress within allowable limits
B. Pressure Rating Table (PN System)
Table B1 — PN Rating vs Pressure
| PN Rating | Pressure (bar) | Pressure (MPa) | Typical Service |
|---|---|---|---|
| PN6 | 6 | 0.6 | Water pipelines |
| PN10 | 10 | 1.0 | Utility systems |
| PN16 | 16 | 1.6 | General industrial |
| PN25 | 25 | 2.5 | Process piping |
| PN40 | 40 | 4.0 | High-pressure systems |
Temperature Derating Consideration
Actual allowable pressure reduces with temperature due to:
- Reduction in material yield strength
- Increased creep effects (at elevated temperature)
C. Torque Chart
Bolt torque values are influenced by:
- Bolt material grade
- Lubrication condition
- Desired preload
Table C1 — Recommended Torque Values
| Bolt Size | Grade 8.8 (Dry) Nm | Grade 8.8 (Lubricated) Nm | Grade 10.9 (Dry) Nm | ASTM B7 (Lubricated) Nm |
|---|---|---|---|---|
| M12 | 80 | 60 | 110 | 95 |
| M16 | 200 | 150 | 280 | 240 |
| M20 | 400 | 300 | 550 | 480 |
| M24 | 700 | 520 | 950 | 820 |
| M27 | 1000 | 750 | 1350 | 1150 |
| M30 | 1350 | 1000 | 1800 | 1550 |
| M33 | 1800 | 1350 | 2400 | 2100 |
Engineering Notes
- Lubrication reduces friction → increases preload consistency
- Torque scatter must be considered (±10–15%)
- Final torque values should align with project specifications
D. Preload Calculation Guide
1. Fundamental Bolt Load Equation
F = P \times A
Where:
- ( F ) = force due to internal pressure
- ( P ) = internal pressure
- ( A ) = internal cross-sectional area
2. Bolt Stress Equation
\[
\sigma_b = \frac{F_b}{A_b}
\]
Where:
- ( \sigma_b ) = bolt stress
- ( F_b ) = bolt preload force
- ( A_b ) = tensile stress area of bolt
3. Torque–Preload Relationship
\[
T = K \times F \times d
\]
Where:
- ( T ) = torque
- ( K ) = friction factor (0.15–0.25)
- ( F ) = preload force
- ( d ) = bolt diameter
4. Sample Calculation
Given:
- Pressure = 16 bar (1.6 MPa)
- Pipe ID = 200 mm
- Bolt size = M20
- Number of bolts = 12
Step 1: Calculate Area
\[
A = \frac{\pi D^2}{4} = \frac{3.14 \times (0.2)^2}{4} = 0.0314 \, m^2
\]
Step 2: Force Due to Pressure
\[
F = P \times A = 1.6 \times 10^6 \times 0.0314 = 50{,}240 \, N
\]
Step 3: Load Per Bolt
\[
F_{bolt} = \frac{50{,}240}{12} \approx 4{,}187 \, N
\]
Step 4: Apply Safety Factor (×2 to ×3)
\[
F_{design} \approx 10{,}000 \, N \text{ per bolt}
\]
Step 5: Torque Estimation
\[
T = 0.2 \times 10{,}000 \times 0.02 = 40 \, \text{Nm}
\]
Engineering Conclusion
- Preload must exceed pressure-induced separation force
- Actual torque values must align with gasket requirements
E. Mechanical Property Table
Table E1 — Mechanical Properties
| Material | Yield Strength (MPa) | Tensile Strength (MPa) | Elongation (%) | Hardness (HB) | Impact Value |
|---|---|---|---|---|---|
| A105 | 250 | 485–620 | 20 | 120–180 | Moderate |
| LF2 | 250 | 485–620 | 22 | 120–180 | High (low temp) |
| F304 | 205 | 515–720 | 40 | 150–200 | High |
| F316 | 205 | 515–720 | 40 | 150–220 | High |
| F11 | 275 | 415–585 | 18 | 140–200 | Moderate |
| F22 | 415 | 585–760 | 16 | 160–220 | Moderate |
F. Corrosion Resistance Comparison Table
Table F1 — Environmental Suitability
| Material | Marine | Acidic | Humid | Hydrocarbon |
|---|---|---|---|---|
| Carbon Steel | Poor | Poor | Moderate | Good |
| SS304 | Moderate | Moderate | Good | Good |
| SS316 | Good | Good | Excellent | Good |
| Alloy Steel | Moderate | Poor | Moderate | Excellent |
| Duplex | Excellent | Excellent | Excellent | Excellent |
9. Inspection & Quality Control
Inspection of BS 4504 Flanges ensures compliance with dimensional, mechanical, and material requirements.
Non-Destructive Testing (NDT)
Positive Material Identification (PMI)
- Verifies alloy composition
- Ensures correct material grade
Ultrasonic Testing (UT)
- Detects internal defects
- Applicable for forged flanges
Magnetic Particle Inspection (MPI)
- Detects surface/subsurface cracks
- Used for carbon and alloy steel
Dye Penetrant Inspection (DPI)
- Detects surface defects
- Used for stainless steel
Hydrostatic Testing
- Validates pressure containment capability
- Conducted as per project requirements
Dimensional Inspection
Verification of:
- Outer diameter
- Bore diameter
- Bolt circle diameter
- Hole alignment
- Face flatness
Certification
EN 10204 3.1
- Manufacturer certification
- Chemical & mechanical test results
EN 10204 3.2
- Third-party inspection validation
- Independent verification body
Traceability System
Each flange is marked with:
- Heat number
- Material grade
- Size and PN rating
- Manufacturer identification
Ensures:
- Full traceability from raw material to dispatch
10. Industries Served
BS 4504 Flanges are deployed across sectors where pressure containment, system reliability, and maintainability are critical. Selection is driven by PN rating, material compatibility, and service conditions.
Oil & Gas (Upstream, Midstream, Downstream)
Applications
- Wellhead flowlines
- Gathering and transmission pipelines
- Refinery process units
- Tank farm connections
Engineering Requirements
- Resistance to hydrocarbons and sour service (when specified)
- Compatibility with process piping standards
- Controlled bolt preload for leak-tight joints
Material Preference
- Carbon steel (A105) for general service
- Stainless steel / Duplex for corrosive environments
Refineries & Petrochemical Plants
Applications
- Heat exchangers
- Distillation columns
- Reactor piping
- Utility manifolds
Engineering Considerations
- Elevated temperature performance
- Chemical compatibility
- Cyclic loading resistance
Power Generation (Thermal / Combined Cycle)
Applications
- Boiler feedwater systems
- Steam pipelines
- Cooling water circuits
Engineering Considerations
- Thermal expansion management
- High-temperature alloy steel usage (F11 / F22)
- Long-term creep resistance
Chemical Processing Plants
Applications
- Acid handling systems
- Solvent transfer lines
- Reaction loops
Engineering Considerations
- Corrosion resistance
- Gasket compatibility
- Material stability under chemical exposure
Water & Wastewater Systems
Applications
- Pump stations
- Treatment plant piping
- Municipal transmission lines
Engineering Considerations
- Corrosion protection (coatings / galvanizing)
- Long-term exposure to moisture
- Ease of maintenance
Infrastructure & Utility Pipelines
Applications
- District cooling systems
- Industrial utility corridors
- Firewater systems
Engineering Considerations
- Reliability under continuous service
- Standardization for maintenance efficiency
11. Export Capability & Global Supply
Super Industries manufactures and supplies BS 4504 Flanges for international EPC projects with structured export execution aligned to project documentation requirements.
Export Regions
- United States
- European Union
- Middle East (GCC countries)
- Southeast Asia
- Africa (project-based supply)
Packaging Standards
- Wooden crates (ISPM-15 compliant)
- Palletized loads with moisture protection
- Individual flange protection for sealing faces
- Rust preventive application for carbon steel
Documentation Package
Supplied documentation typically includes:
- Commercial invoice
- Packing list
- Mill Test Certificates (EN 10204 3.1 / 3.2)
- Inspection reports
- Dimensional inspection records
- NDT reports (if applicable)
- Certificate of origin
Logistics Coordination
- Coordination with EPC procurement schedules
- Port handling and containerization
- Marking aligned with project tagging systems
- Support for multi-location dispatches
Project Supply Capability
- Bulk supply aligned with project timelines
- Lot traceability for each batch
- Capability to support shutdown and maintenance schedules
- Integration with EPC vendor documentation systems
12. PROCUREMENT & INSTALLATION VIEW
Bolt Tightening Sequence (Cross Pattern)
Proper tightening sequence ensures:
- Uniform gasket compression
- Prevention of flange distortion
Recommended Method
- Initial hand tightening
- Star (cross) pattern tightening
- Incremental torque application (30% → 60% → 100%)
Torque Application Stages
| Stage | Torque Level | Purpose |
|---|---|---|
| Stage 1 | 30% | Initial seating |
| Stage 2 | 60% | Intermediate alignment |
| Stage 3 | 100% | Final preload |
| Stage 4 | Circular pass | Uniform stress distribution |
Re-Torque Practice
- Conducted after initial pressurization or thermal cycling
- Compensates for:
- Gasket creep
- Bolt relaxation
Gasket Selection & Replacement
Selection Criteria
- Pressure class (PN rating)
- Temperature range
- Chemical compatibility
Common Gasket Types
- Non-asbestos fiber
- Spiral wound
- PTFE-based
Replacement Guidelines
- Replace after disassembly
- Inspect flange face for damage
- Verify surface finish before installation
Field Inspection Checklist
Before commissioning:
- Verify flange alignment
- Confirm bolt grade and size
- Check torque values
- Inspect gasket installation
- Ensure no visible flange distortion
Storage Practices
- Store in dry, covered environment
- Protect flange faces with covers
- Avoid direct ground contact
- Maintain traceability markings
13. CUSTOM ENGINEERING CAPABILITIES
Super Industries supports project-specific requirements for BS 4504 Flanges within defined engineering and manufacturing limits.
Non-Standard Sizes
- Custom DN beyond standard range
- Adaptation for project-specific piping systems
Special Drilling Patterns
- Non-standard bolt hole configurations
- Matching with legacy equipment
High-Thickness Flanges
- Designed for:
- High-pressure applications
- Structural reinforcement
Coating Customization
- Project-specific coating systems
- Compliance with environmental exposure conditions
Project-Specific Marking
- Tag numbers
- Heat numbers
- Client-specific identification formats
ENGINEERING SUMMARY
BS 4504 Flanges provide a standardized, pressure-rated, bolted connection system suitable for:
- Controlled disassembly
- Reliable gasket-based sealing
- Compatibility with legacy British-standard piping systems
Their continued application in global projects is driven by:
- Installed base requirements
- Maintenance of existing systems
- Project specifications referencing BS standards
FINAL ENGINEERING CONCLUSION
From an EPC evaluation perspective, BS 4504 Flanges must be assessed on:
- Compliance with dimensional standards
- Material traceability and certification
- Manufacturing control and inspection protocols
- Suitability for pressure, temperature, and environmental conditions
Super Industries manufactures these flanges in alignment with:
- BS dimensional requirements
- ASTM material standards
- EN inspection and certification practices
This ensures that supplied components are suitable for:
- Integration into pressure piping systems
- Third-party inspection acceptance
- Global project procurement environments
[latexcode]