
PLOW BOLTS
Super Industries
“Global Manufacturer of Heavy & Custom Engineered Fasteners for Oil & Gas, Power & EPC Contractors.”
Plow bolts are structural fastening components used in heavy-duty equipment where bolt heads must remain flush with the working surface. These fasteners are primarily installed in ground-engaging systems and wear-plate assemblies exposed to abrasion, impact loading, and cyclic vibration.
1. Industry Context & Equipment Relevance
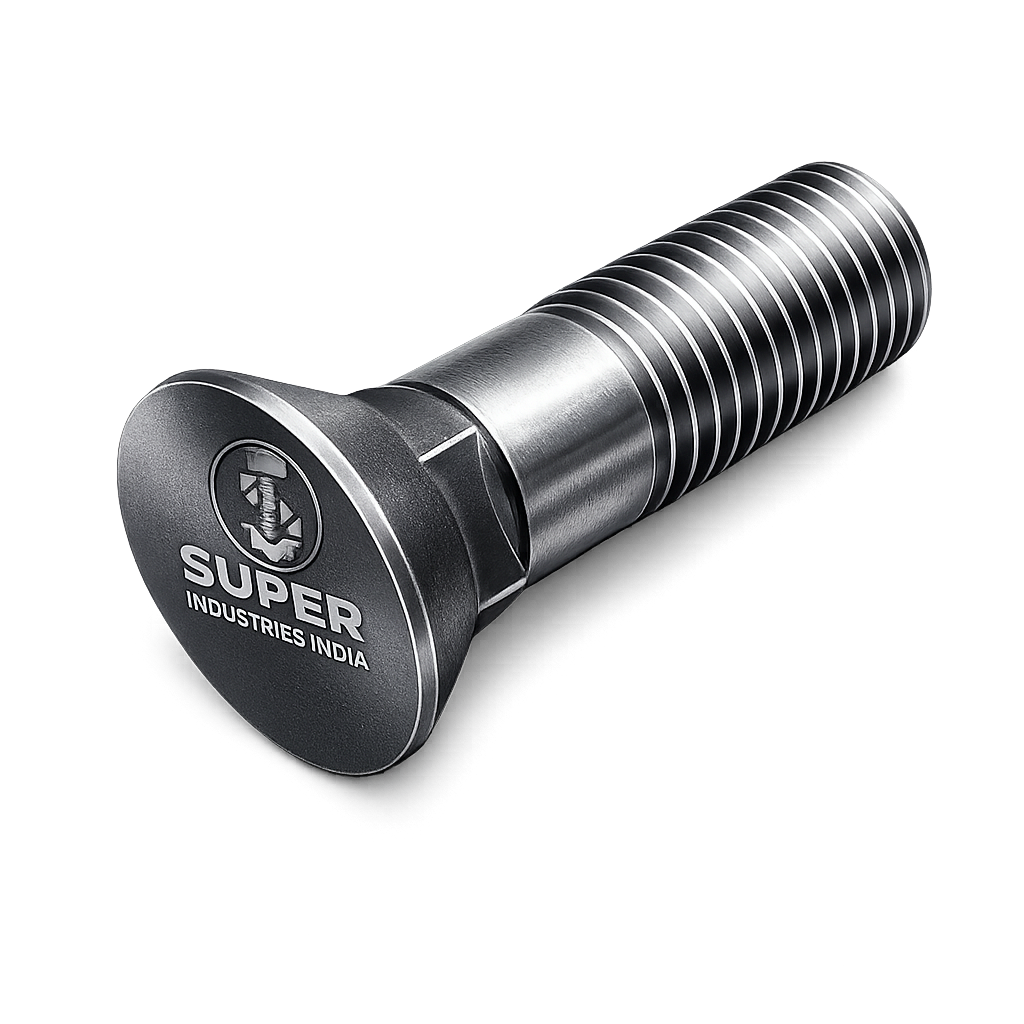
Heavy equipment operating in mining, construction, agriculture, and infrastructure environments relies on ground-engaging components that experience severe abrasion and impact loads. The structural fastening systems used to secure these components must maintain both mechanical integrity and a smooth working surface.
Plow bolts are specifically engineered for this requirement.
Unlike conventional hex head bolts, which protrude above the mounting surface, plow bolts incorporate countersunk or flat heads that seat flush within prepared holes. This configuration eliminates head exposure to abrasive materials such as rock fragments, compacted soil, or aggregate particles.
Typical heavy machinery applications include:
Earthmoving Equipment
Earthmoving machinery uses plow bolts to secure wear plates and blade edges. Bulldozer blades, scrapers, and graders operate in direct contact with abrasive soil and rock surfaces. Flush mounting prevents bolt head erosion while maintaining blade geometry.
Bulldozers
Blade cutting edges and end bits are typically attached using plow bolts because exposed bolt heads would wear rapidly against soil and aggregate. Flush installation ensures that the blade maintains a continuous contact surface with the ground.
Excavators
Excavator buckets incorporate wear liners and ground-engaging plates attached using countersunk fastening systems. Plow bolts maintain structural retention while protecting the bolt head from mechanical wear.
Motor Graders
Grader moldboards use plow bolts to secure replaceable cutting edges. The flush head configuration prevents interference with material flow along the blade surface during grading operations.
Agricultural Plows
Traditional agricultural plow blades rely on plow bolts for the same reason that construction equipment does: soil must flow smoothly across the blade without obstruction. A protruding fastener head would disrupt soil movement and accelerate wear.
Mining Loaders
Underground mining loaders operate in environments containing high-abrasion rock fragments. Wear liners and replaceable ground-contact plates are typically mounted using heavy-duty plow bolts to maintain flush surfaces under continuous abrasion.
Scrapers and Trenching Machines
Large trenching machines and earth scrapers utilize replaceable cutting edges and structural wear plates. Plow bolts secure these components without creating protrusions that could interfere with trench geometry or soil displacement.
Construction Blade Assemblies
Construction equipment blade assemblies depend on plow bolts to maintain a uniform cutting surface. The flush head design ensures the blade edge remains continuous across the entire width of the assembly.
Ground-Engaging Tool (GET) Systems
Ground-engaging tool systems include components such as:
- Bucket teeth
- Cutting edges
- Side cutters
- Wear liners
- Moldboard plates
These systems require fastening solutions capable of sustaining high shear loads while preventing surface irregularities that could alter equipment performance.
Why Plow Bolts Are Selected Over Conventional Hex Bolts
Standard hex bolts are unsuitable for high-wear surface applications due to the geometry of the bolt head.
A hex head bolt protrudes above the mounting surface. When installed in ground-contact environments, the head becomes a point of concentrated abrasion. Over time, the head may wear away, leading to loosening of the joint and eventual failure of the fastening system.
Plow bolts solve this problem through several design characteristics.
Flush Head Requirement
The countersunk head allows the bolt to sit completely within a conical seat machined into the wear plate or blade component. Once installed, the bolt head becomes flush with the surface.
This configuration prevents:
- Direct abrasion against the bolt head
- Soil flow disruption
- Localized wear acceleration
- Bolt head rounding or deformation
Abrasion Resistance
The flush mounting configuration reduces exposure of the bolt head to abrasive material flow. Wear occurs primarily on the equipment surface rather than on the fastener head itself.
As a result, plow bolts maintain structural engagement with the fastening system even under continuous abrasive loading conditions.
Structural Shear Performance
In many ground-engaging systems, loads acting on the bolt are primarily shear loads rather than tensile loads. The shank of the plow bolt carries these shear forces across the joint interface between wear plates and equipment structures.
Properly installed plow bolts maintain clamp force that helps distribute shear loads across the joint surface, reducing localized stress concentrations.
2. Technical Definition of Plow Bolts
Plow bolts are structural fasteners characterized by a countersunk or flat head configuration designed to sit flush within a conical seat in the mounting surface.
They are specifically engineered for applications where protruding bolt heads would interfere with material flow or experience accelerated wear.
Core Characteristics
Plow bolts typically incorporate the following structural elements:
- Flat or countersunk bolt head
- Square or ribbed neck section beneath the head
- Cylindrical shank
- Threaded end for nut engagement
The geometry of the bolt head is designed to match countersunk holes in equipment components such as blades, liners, and wear plates.
Countersunk Head Geometry
The defining characteristic of a plow bolt is the countersunk head.
The underside of the head forms a conical surface designed to seat within a matching countersink in the equipment component. This seating configuration distributes compressive forces around the circumference of the head.
The advantages include:
- Uniform load transfer into the wear plate
- Elimination of protruding surfaces
- Reduced stress concentration in the plate material
Countersunk seating also helps stabilize the bolt under dynamic loading conditions.
Square Neck Locking Mechanism
Many plow bolts incorporate a square neck section located immediately beneath the head.
When inserted into a square hole or into a slightly undersized round hole, this square section prevents rotation of the bolt during tightening. The anti-rotation mechanism allows installation from one side of the equipment structure while the nut is tightened from the opposite side.
This feature is particularly important in heavy machinery where access to both sides of the joint may be limited.
Rib Neck Design
In some plow bolt configurations, the square neck is replaced by a ribbed neck. The ribs create frictional engagement with the surrounding material when the bolt is installed.
This friction prevents bolt rotation during torque application.
Shear Load Distribution
Plow bolts are commonly used in joints where shear loads dominate.
The cylindrical shank transmits shear forces across the interface between wear components and structural members. Maintaining correct shank diameter tolerance is critical because excessive clearance between the bolt shank and hole can increase joint slip and fatigue loading.
In heavy equipment design, engineers typically size the bolt diameter to ensure adequate shear capacity relative to expected operational loads.
Anti-Rotation Design
The square neck or ribbed neck configuration provides an anti-rotation mechanism during installation. Without this feature, tightening the nut would cause the entire bolt to rotate within the countersunk hole.
Preventing rotation is essential because:
- It preserves seating contact between the head and countersunk surface.
- It prevents damage to the wear plate hole geometry.
- It ensures proper torque transfer to the nut.
Common Head Types Used in Plow Bolts
Although the general function remains consistent, plow bolts are manufactured in several head configurations depending on equipment design requirements.
Flat Countersunk Head Plow Bolts
These are the most common configuration used in heavy equipment. The flat countersunk head sits flush with the surface and provides broad seating contact within the countersink.
Typical applications include:
- Bulldozer cutting edges
- Motor grader blades
- Scraper wear plates
Oval Head Plow Bolts
Oval head plow bolts feature a slightly rounded upper surface rather than a completely flat profile.
This design is sometimes used in agricultural equipment where minor surface curvature does not interfere with soil flow.
Rib Neck Plow Bolts
Rib neck plow bolts use radial ribs beneath the head instead of a square section. These ribs embed into the surrounding material when the bolt is installed, providing rotational resistance.
Square Neck Plow Bolts
Square neck plow bolts incorporate a square cross-section immediately beneath the head. This section locks into a matching square hole or slightly deforms the surrounding material to prevent rotation.
Square neck designs are commonly used in heavy earthmoving equipment.
Nut Pairing Systems
Plow bolts are typically installed using heavy-duty hex nuts.
Depending on equipment requirements, the following nut configurations may be used:
- Standard hex nuts
- Heavy hex nuts
- Lock nuts
- Nylon insert lock nuts (limited use in high-temperature environments)
- Prevailing torque nuts
Washers may also be used depending on joint design, although in many plow bolt applications the nut bears directly against the structural surface.
Correct nut selection is essential to maintain preload under vibration and impact loading conditions.
3. Structural Load & Fastening Mechanics
Plow bolt performance depends on the interaction between clamp force, shear loading, and countersunk seating geometry.
The joint created by a plow bolt must resist multiple mechanical forces simultaneously:
- Shear loads generated by equipment operation
- Tensile forces generated during tightening
- Dynamic vibration from machinery movement
- Impact loads from contact with rock or soil
Understanding the mechanics of these forces is essential for proper fastener selection.
Bolt Preload Mechanics
During installation, torque applied to the nut creates tensile stress within the bolt. This tension generates clamp force between the joined components.
The clamp force compresses the wear plate against the equipment structure.
Maintaining sufficient preload is critical because it:
- Prevents joint separation
- Reduces joint slip under shear loading
- Minimizes fatigue stress in the bolt shank
Shear Load Transfer
When the equipment experiences external loads, shear forces act across the joint interface.
Two mechanisms resist these forces:
- Friction generated by clamp force
- Direct shear resistance of the bolt shank
If the frictional resistance between the surfaces exceeds the applied load, the bolt itself experiences minimal shear stress. If the load exceeds the friction capacity, the bolt shank begins carrying shear.
Proper bolt sizing ensures the shank can safely withstand this load.
Clamp Force vs Surface Wear Interaction
In wear-plate applications, abrasion gradually reduces surface thickness around the bolt head. If wear becomes excessive, the countersunk seat may lose full contact with the bolt head.
When this occurs:
- Clamp force decreases
- Joint slip may increase
- Shear load shifts to the bolt shank
Regular inspection of wear plates helps prevent loss of preload due to material erosion.
Countersunk Seat Load Distribution
The countersunk interface between the bolt head and the plate distributes compressive forces along the conical seating surface.
This distribution reduces localized stress concentrations compared with flat-bearing surfaces.
However, the countersunk seat must be precisely machined. Improper seat angles can create uneven contact, which increases stress on one portion of the bolt head.
Maintaining correct seat geometry is therefore an important part of equipment fabrication.
Super Industries
Global Manufacturer of Heavy & Custom Engineered Fasteners & Flanges.
4. Load & Mechanical Engineering Considerations
Plow bolts operate in environments where loads vary widely in magnitude and direction.
Heavy machinery design must account for several types of mechanical loading.
Static Structural Loading
Static loads occur when the equipment supports weight or resists steady forces during operation. For example, when a bulldozer blade pushes soil, the cutting edge experiences continuous resistance.
Plow bolts must maintain clamp force and structural stability under these conditions.
Impact Loading from Rock Contact
Mining equipment frequently encounters sudden impacts when contacting rock formations. These impacts produce short-duration high-magnitude loads that propagate through the equipment structure.
Plow bolts must possess sufficient toughness to withstand these impacts without brittle fracture.
Cyclic Fatigue Loading
Equipment vibration and repeated loading cycles create fatigue stresses in fasteners.
Over time, fluctuating stress levels may initiate microscopic cracks within the bolt material. Fatigue-resistant materials and correct preload levels help prevent crack propagation.
Abrasion Environment Stresses
Abrasion does not act directly on the bolt shank in most cases, but it affects the surrounding wear plate and countersunk seat.
As material wears away, seating geometry changes, which may alter load distribution on the bolt head.
Equipment Vibration
Continuous vibration from engines, hydraulic systems, and ground contact can gradually reduce bolt preload if improper tightening procedures are used.
Use of correct torque values and appropriate nut types helps maintain preload under these conditions.
Safety Factors in Heavy Machinery
Heavy equipment design typically incorporates safety factors when selecting structural fasteners.
These safety factors account for:
- Material variability
- Unexpected loading conditions
- Environmental degradation
- Installation variability
Engineers select bolt grades and diameters that provide sufficient strength margins relative to expected loads.
Shear vs Tensile Loading Conditions
Plow bolts primarily experience shear loading in ground-engaging equipment, but tensile loads still occur due to tightening torque and structural deflection.
Proper design ensures that both shear capacity and tensile strength are adequate.
Bolt Head Seating Stresses
The countersunk head introduces compressive stress between the bolt head and the plate.
If the countersink angle or surface finish is incorrect, uneven seating may cause localized deformation of the bolt head or surrounding plate material.
Accurate machining and dimensional control are therefore required to ensure uniform load distribution.
Below is Part 2 of the engineering documentation page, continuing from Part 1 with materials engineering, international standards, heat treatment metallurgy, manufacturing discipline, and surface finishing systems for Plow Bolts.
The structure maintains EPC documentation quality, engineering precision, and OEM technical clarity.
5. Applicable Standards for Plow Bolts
Structural fasteners used in heavy equipment must conform to internationally recognized mechanical property standards. These standards define minimum strength requirements, material chemistry limits, hardness ranges, and inspection procedures.
For plow bolts used in mining equipment, earthmoving machinery, and structural wear systems, several ASTM, SAE, DIN, and ISO standards are typically referenced during equipment design and procurement evaluation.
Standards are selected based on:
- Required tensile strength
- Yield strength
- Fatigue resistance
- Impact toughness
- Service environment conditions
The following standards are commonly referenced when specifying plow bolts for heavy equipment.
ASTM Standards
ASTM A307 — Carbon Steel Bolts
ASTM A307 specifies carbon steel bolts and studs intended for general structural use.
Key characteristics include:
- Moderate tensile strength
- Good machinability
- Suitable for light-to-medium structural applications
Although ASTM A307 bolts are sometimes used in agricultural equipment, they are generally not preferred for high-impact mining equipment due to lower strength compared with alloy steel grades.
Typical applications:
- Agricultural plow blades
- Light construction machinery
- Low-stress equipment assemblies
ASTM A325 — High Strength Structural Bolts (Limited Application)
ASTM A325 bolts are commonly used in structural steel construction. While not specifically designed for plow bolt geometry, their mechanical strength characteristics are sometimes referenced for heavy structural fastening systems.
Characteristics include:
- High tensile strength
- Controlled heat treatment
- Suitable for high-load structural joints
However, most earthmoving equipment manufacturers prefer SAE J429 or ASTM A449 grade materials for plow bolts due to compatibility with equipment design practices.
ASTM A449 — Medium Carbon Alloy Steel Bolts
ASTM A449 bolts provide higher strength than A307 bolts and are suitable for structural machinery applications requiring increased tensile capacity.
Key features:
- Higher yield strength
- Improved fatigue resistance
- Greater shear load capacity
A449 grade materials are commonly used for heavy equipment plow bolts where higher mechanical strength is required without transitioning to specialty alloy fasteners.
SAE Standards
SAE J429 — Mechanical Properties of External Threaded Fasteners
SAE J429 is one of the most widely used standards for automotive and heavy equipment fasteners in North America.
The standard defines mechanical property classes such as:
- SAE Grade 5
- SAE Grade 8
These grades are frequently used for plow bolts due to their well-defined mechanical performance and compatibility with earthmoving equipment design.
SAE Grade 5
Typical characteristics:
- Medium carbon steel
- Heat treated for strength
- Good balance between toughness and hardness
Applications include:
- Construction equipment wear plates
- Agricultural plow systems
- Medium-duty earthmoving machinery
SAE Grade 8
SAE Grade 8 bolts provide significantly higher strength compared with Grade 5.
Characteristics include:
- Quenched and tempered alloy steel
- Higher tensile strength
- Higher yield strength
- Greater resistance to deformation under heavy load
These bolts are commonly used in mining equipment, bulldozer cutting edges, and high-load ground-engaging tool systems.
DIN Standards
DIN 604 — Flat Countersunk Head Bolts
DIN 604 defines bolts with flat countersunk heads and square necks. This configuration closely matches the design used in many plow bolt applications.
Key dimensional characteristics defined by DIN 604 include:
- Head diameter
- Countersunk head angle
- Square neck dimensions
- Thread length
DIN 604 bolts are widely used in European agricultural and machinery equipment.
DIN 605 — Countersunk Head Bolts with Ribbed Neck
DIN 605 defines bolts featuring a countersunk head and ribbed neck configuration designed to prevent rotation during tightening.
This design is commonly used when the mating hole is round rather than square.
ISO Structural Fastener References
ISO standards provide dimensional and mechanical property references used in international procurement documentation.
Relevant ISO references include:
- ISO property classes for fasteners
- Thread tolerances
- Surface coating requirements
- Mechanical property verification
ISO alignment is often required for equipment exported to international markets.
Standards and Equipment Load Requirements
Fastener standards are selected based on expected service loads.
Typical engineering considerations include:
- Shear loading on blade assemblies
- Impact loading from rock contact
- Cyclic fatigue loading during operation
- Temperature variation in outdoor equipment
Equipment manufacturers evaluate these parameters when selecting plow bolt grades.
6. Material & Grade Options for Plow Bolts
Material selection determines the mechanical performance, fatigue life, and environmental durability of plow bolts.
The most common materials used for plow bolt manufacturing include carbon steels, alloy steels, and stainless steels for specialized environments.
Carbon Steel Plow Bolts
Carbon steel remains the most widely used material for plow bolts due to its cost efficiency and adequate strength for many applications.
ASTM A307 Carbon Steel
Properties include:
- Moderate yield strength
- Good machinability
- Suitable for low to moderate loads
Typical use:
- Agricultural equipment
- Light construction machinery
SAE Grade 5 Carbon Steel
SAE Grade 5 bolts are manufactured from medium carbon steel and undergo heat treatment to achieve improved strength.
Advantages:
- Balanced strength and toughness
- Suitable for moderate-to-heavy equipment
- Widely available for OEM production
Applications:
- Motor grader blades
- Scraper cutting edges
- Agricultural machinery
SAE Grade 8 Carbon Alloy Steel
SAE Grade 8 plow bolts are used in high-load environments.
Characteristics:
- High tensile strength
- Increased hardness
- Greater resistance to plastic deformation
Typical equipment:
- Bulldozers
- Mining loaders
- Quarry equipment
Alloy Steel Plow Bolts
ASTM A449 Alloy Steel
ASTM A449 bolts are manufactured from medium carbon alloy steel and heat treated to achieve higher strength levels.
Advantages include:
- Higher yield strength
- Improved fatigue resistance
- Enhanced shear performance
These bolts are often specified for:
- Mining equipment
- Heavy construction machinery
- High-impact structural joints
Stainless Steel Plow Bolts
In environments where corrosion resistance is required, stainless steel materials may be used.
AISI 304 Stainless Steel
Characteristics:
- Austenitic stainless structure
- Good corrosion resistance
- Moderate strength
Typical environments:
- Agricultural machinery exposed to moisture
- Food processing equipment
AISI 316 Stainless Steel
AISI 316 contains molybdenum, which improves corrosion resistance in aggressive environments.
Characteristics:
- High resistance to chloride corrosion
- Good resistance to chemical exposure
- Stable mechanical properties at moderate temperatures
Applications include:
- Coastal infrastructure equipment
- Chemical processing machinery
Material Comparison Table for Plow Bolts
| Grade | Yield Strength | Tensile Strength | Hardness Range | Temperature Range | Corrosion Resistance | Typical Equipment Application |
|---|---|---|---|---|---|---|
| ASTM A307 | ~250 MPa | ~400 MPa | HRB 60–100 | −20°C to 200°C | Low | Agricultural plows |
| SAE Grade 5 | ~635 MPa | ~830 MPa | HRC 25–34 | −40°C to 300°C | Moderate | Construction equipment |
| SAE Grade 8 | ~940 MPa | ~1040 MPa | HRC 33–39 | −40°C to 300°C | Moderate | Mining equipment |
| ASTM A449 | ~860 MPa | ~1030 MPa | HRC 24–36 | −40°C to 350°C | Moderate | Heavy earthmoving machinery |
| AISI 304 | ~215 MPa | ~505 MPa | HRB 70–90 | −200°C to 870°C | High | Wet agricultural environments |
| AISI 316 | ~205 MPa | ~515 MPa | HRB 70–90 | −200°C to 870°C | Very High | Marine environments |
7. Heat Treatment Engineering
Heat treatment significantly influences the mechanical performance of plow bolts. Proper heat treatment ensures that the bolt achieves the required balance between strength, hardness, and toughness.
Several processes are commonly used.
Normalizing
Normalizing involves heating the steel above its critical temperature followed by controlled air cooling.
Benefits include:
- Grain structure refinement
- Improved uniformity in mechanical properties
- Reduced internal stresses from forging
Normalizing is often used as a preliminary treatment before further heat treatment.
Quenching and Tempering
High-strength plow bolts such as SAE Grade 8 and ASTM A449 typically undergo quenching and tempering.
The process involves:
- Heating the bolt above the austenitizing temperature
- Rapid cooling (quenching) in oil or water
- Reheating at a lower temperature (tempering)
This process produces:
- High tensile strength
- Controlled hardness
- Improved fatigue resistance
Tempering also reduces brittleness introduced during quenching.
Stress Relieving
Stress relieving reduces residual stresses created during forging, machining, or heat treatment.
The bolts are heated to a moderate temperature and held for a specified period before cooling.
Benefits include:
- Improved dimensional stability
- Reduced distortion during service
- Increased fatigue life
Hardness Control
Hardness testing ensures that the heat treatment process achieved the specified mechanical property range.
Excessive hardness may lead to brittle fracture, while insufficient hardness reduces load-bearing capacity.
Typical hardness ranges are defined by the material grade standard.
Grain Structure and Toughness
Heat treatment controls the microstructure of the steel.
Fine grain structures improve:
- Impact resistance
- Fatigue performance
- Crack propagation resistance
For heavy equipment plow bolts, maintaining appropriate toughness is critical because bolts are exposed to impact loading from rock and soil contact.
Charpy Impact Testing
In high-load environments, impact toughness may be evaluated using Charpy impact testing.
This test measures the energy absorbed during fracture of a notched specimen.
Higher impact values indicate better resistance to sudden shock loading.
Mining equipment manufacturers often require impact testing when bolts are used in cold environments or high-impact applications.
8. Manufacturing Process of Plow Bolts
Manufacturing plow bolts requires strict dimensional control to ensure proper seating in countersunk holes and correct engagement with equipment components.
The production sequence typically follows several controlled stages.
1. Raw Material Inspection
Steel bars or wire rods are inspected upon arrival.
Verification includes:
- Chemical composition analysis
- Mechanical property verification
- Surface defect inspection
Only materials meeting specification requirements proceed to production.
2. Hot Forging of Bolt Head
The bolt head is formed through hot forging.
The material is heated to forging temperature and pressed into a die that forms the countersunk head geometry.
Hot forging improves grain flow and mechanical strength in the head region.
3. Shank Forming
After forging, the bolt shank is formed to the required diameter and length.
Dimensional tolerances are carefully controlled to ensure compatibility with equipment mounting holes.
4. Square Neck Formation
For square neck plow bolts, a secondary forming process creates the anti-rotation square section beneath the head.
This section must match the equipment hole geometry to prevent bolt rotation during installation.
5. CNC Machining (When Required)
Certain plow bolt designs require machining operations to achieve precise head angles or dimensional tolerances.
Machining may also be used for special OEM designs.
6. Thread Rolling
Threads are typically produced through thread rolling rather than cutting.
Thread rolling provides several advantages:
- Improved fatigue strength
- Better surface finish
- Higher dimensional accuracy
The rolling process cold-forms the thread profile, improving grain structure along the thread.
7. Heat Treatment
Heat treatment is performed according to the specified material grade.
Processes may include:
- Quenching and tempering
- Normalizing
- Stress relieving
8. Surface Finishing
Surface treatments are applied to improve corrosion resistance and surface durability.
9. Final Inspection
Inspection includes:
- Dimensional verification
- Thread gauge testing
- Hardness testing
- Surface finish inspection
10. Marking and Traceability
Bolts are marked according to grade and manufacturer identification requirements.
Traceability allows material batches to be tracked through the production and inspection process.
9. Surface Finish Options for Plow Bolts
Surface treatments improve corrosion resistance and service life.
The selected finish depends on equipment operating environment.
Black Oxide Coating
Black oxide is a conversion coating applied through chemical treatment.
Characteristics:
- Minimal dimensional change
- Moderate corrosion protection
- Improved surface appearance
Used primarily for indoor or controlled environments.
Zinc Plating
Electroplated zinc coatings provide corrosion resistance through sacrificial protection.
Typical coating thickness:
- 5–25 microns
Zinc plating is commonly used for construction and agricultural equipment.
Hot-Dip Galvanizing
Hot-dip galvanizing provides thicker zinc coatings than electroplating.
Coating thickness typically ranges between:
- 40–100 microns
Advantages include improved corrosion protection in outdoor environments.
Phosphate Coating
Phosphate coatings improve lubrication during installation and enhance paint adhesion.
Often used in conjunction with oil coatings.
PTFE Coating
Polytetrafluoroethylene (PTFE) coatings reduce friction during tightening and improve corrosion resistance.
These coatings are used where controlled torque installation is required.
Mechanical Galvanizing
Mechanical galvanizing applies zinc coatings through a cold process that avoids hydrogen embrittlement risks associated with electroplating.
This process is used for high-strength bolts where hydrogen embrittlement must be avoided.
A. Plow Bolt Dimension Reference Table
The geometry of plow bolts must match the countersunk holes prepared in equipment components such as cutting edges, wear liners, moldboards, and ground-engaging plates. Correct dimensional alignment ensures flush seating, adequate load distribution, and reliable anti-rotation engagement.
Typical dimensional parameters include:
- Bolt diameter
- Head diameter
- Countersunk head angle
- Square neck dimension
- Thread length
- Overall bolt length
Typical Plow Bolt Dimensions
| Bolt Diameter | Head Diameter | Countersunk Angle | Square Neck Size | Thread Length | Overall Length |
|---|---|---|---|---|---|
| M10 / 3⁄8″ | 22 mm | 90° | 10 mm | 25 mm | 40–80 mm |
| M12 / 1⁄2″ | 26 mm | 90° | 12 mm | 30 mm | 50–100 mm |
| M16 / 5⁄8″ | 34 mm | 90° | 16 mm | 38 mm | 60–120 mm |
| M20 / 3⁄4″ | 42 mm | 90° | 20 mm | 45 mm | 70–150 mm |
| M24 / 7⁄8″ | 50 mm | 90° | 24 mm | 55 mm | 90–180 mm |
| M30 / 1-1⁄8″ | 62 mm | 90° | 30 mm | 65 mm | 120–220 mm |
Engineering notes:
- Head diameter must provide adequate seating surface within the countersunk hole.
- Square neck dimensions must match the hole tolerance to prevent bolt rotation during installation.
- Thread length is selected based on grip length and nut engagement requirements.
B. Strength Class Reference Table
Mechanical strength is determined by the fastener grade. Engineers select the grade according to expected loads, fatigue conditions, and environmental factors.
Strength Class Comparison
| Grade | Yield Strength | Tensile Strength | Hardness Range |
|---|---|---|---|
| ASTM A307 | ~250 MPa | ~400 MPa | HRB 60–100 |
| SAE Grade 5 | ~635 MPa | ~830 MPa | HRC 25–34 |
| SAE Grade 8 | ~940 MPa | ~1040 MPa | HRC 33–39 |
| ASTM A449 | ~860 MPa | ~1030 MPa | HRC 24–36 |
| AISI 304 Stainless | ~215 MPa | ~505 MPa | HRB 70–90 |
| AISI 316 Stainless | ~205 MPa | ~515 MPa | HRB 70–90 |
Engineering observations:
- SAE Grade 8 bolts provide the highest strength among commonly used plow bolt materials.
- Carbon steel grades provide higher structural capacity than stainless steel but lower corrosion resistance.
- Stainless steels are typically selected for corrosion environments rather than high-load mining systems.
C. Recommended Torque Values for Plow Bolts
Torque application during installation determines the preload generated within the bolt. Proper torque ensures sufficient clamp force between equipment components and prevents joint separation during operation.
Torque requirements depend on:
- Bolt diameter
- Material grade
- Surface condition (dry or lubricated)
Torque Chart for Plow Bolts
| Bolt Diameter | SAE Grade 5 Dry Torque | SAE Grade 5 Lubricated | SAE Grade 8 Dry Torque | SAE Grade 8 Lubricated |
|---|---|---|---|---|
| 3⁄8″ | 45 Nm | 35 Nm | 65 Nm | 50 Nm |
| 1⁄2″ | 95 Nm | 75 Nm | 135 Nm | 105 Nm |
| 5⁄8″ | 190 Nm | 150 Nm | 270 Nm | 210 Nm |
| 3⁄4″ | 330 Nm | 260 Nm | 470 Nm | 370 Nm |
| 7⁄8″ | 520 Nm | 410 Nm | 720 Nm | 570 Nm |
| 1″ | 780 Nm | 620 Nm | 1080 Nm | 860 Nm |
Engineering considerations:
- Lubrication reduces friction during tightening and therefore reduces required torque.
- Excessive torque can exceed yield strength and lead to bolt failure.
- Insufficient torque results in reduced preload and increased risk of joint slip.
Torque control methods typically include calibrated torque wrenches or hydraulic torque tools for large diameter fasteners.
D. Preload Calculation Guide
Understanding preload is essential for engineers designing structural joints using plow bolts. Preload determines the clamp force that holds equipment components together during operation.
Two fundamental relationships are used to evaluate bolt loading.
Bolt Stress Formula
The normal stress within a bolt is determined by:

Where:
- σ = tensile stress in the bolt
- F = applied tensile force
- A = cross-sectional area of the bolt shank
This relationship allows engineers to determine whether the stress within the bolt remains below the material yield strength.
Preload and Torque Relationship
The preload generated by tightening torque is commonly estimated using:

Where:
- F = bolt preload force
- T = applied torque
- K = friction coefficient (nut factor)
- D = bolt nominal diameter
Typical nut factor values range from 0.15 to 0.25 depending on lubrication and surface condition.
Example Engineering Calculation
Consider a 5⁄8-inch SAE Grade 8 plow bolt tightened to 270 Nm with a nut factor of 0.20.
Given:
- T = 270 Nm
- K = 0.20
- D = 0.625 inches (≈ 0.016 m)
The calculated preload force can be estimated using the preload equation above.
This preload creates clamp force between the wear plate and equipment structure, improving resistance to shear loads during operation.
E. Mechanical Property Reference Table
Mechanical properties influence bolt behavior under tensile loading, impact forces, and fatigue cycles.
Mechanical Property Data
| Material Grade | Yield Strength | Tensile Strength | Hardness | Elongation | Impact Toughness |
|---|---|---|---|---|---|
| ASTM A307 | 250 MPa | 400 MPa | HRB 60–100 | 18% | Moderate |
| SAE Grade 5 | 635 MPa | 830 MPa | HRC 25–34 | 12–16% | Good |
| SAE Grade 8 | 940 MPa | 1040 MPa | HRC 33–39 | 10–12% | Moderate |
| ASTM A449 | 860 MPa | 1030 MPa | HRC 24–36 | 12–14% | Good |
| AISI 304 | 215 MPa | 505 MPa | HRB 70–90 | 40% | High |
| AISI 316 | 205 MPa | 515 MPa | HRB 70–90 | 40% | High |
Engineering implications:
- Higher tensile strength materials support greater preload levels.
- Higher elongation values improve resistance to brittle fracture.
- Impact toughness becomes critical in mining and cold-climate equipment.
F. Corrosion Resistance Comparison
Equipment operating environments vary widely depending on industry sector. Corrosion resistance therefore influences material and coating selection for plow bolts.
Corrosion Resistance Comparison Table
| Material / Coating | Corrosion Resistance | Typical Service Environment |
|---|---|---|
| Carbon Steel (Black) | Low | Dry mining environments |
| Zinc Plated Steel | Moderate | Agricultural machinery |
| Hot-Dip Galvanized | High | Outdoor construction equipment |
| Stainless Steel 304 | High | Wet agricultural environments |
| Stainless Steel 316 | Very High | Coastal and chemical exposure |
Environmental mapping:
- Mining operations often use carbon steel bolts with protective coatings.
- Agricultural equipment frequently uses zinc-plated fasteners.
- Infrastructure and coastal equipment may require stainless steel or galvanized fasteners.
10. Inspection & Quality Control Procedures
Quality control for plow bolts involves multiple inspection stages during manufacturing and prior to shipment. These procedures ensure that the fasteners meet dimensional accuracy, mechanical property requirements, and surface finish specifications.
Positive Material Identification (PMI)
PMI testing verifies the chemical composition of the raw material.
Methods include:
- Optical emission spectroscopy
- X-ray fluorescence analysis
PMI ensures the steel grade matches the material specification.
Hardness Testing
Hardness testing confirms that heat treatment achieved the required mechanical properties.
Common methods include:
- Rockwell hardness testing
- Brinell hardness testing
Hardness values must fall within the range defined by the material standard.
Dimensional Inspection
Dimensional verification ensures compatibility with equipment mounting holes and countersunk seats.
Inspection parameters include:
- Head diameter
- Countersunk angle
- Square neck size
- Thread pitch and length
- Shank diameter tolerance
Precision gauges and coordinate measuring instruments are commonly used.
Thread Gauge Verification
Thread quality is checked using standard gauges.
Verification methods include:
- Go / No-Go thread gauges
- Pitch diameter measurement
Thread accuracy ensures proper nut engagement and reliable preload generation.
Surface Finish Inspection
Surface coatings are inspected to confirm:
- Coating thickness
- Uniform coverage
- Absence of defects such as blistering or flaking
Coating thickness may be measured using magnetic or electronic thickness gauges.
Load Testing
Mechanical testing may include:
- Tensile testing
- Proof load testing
- Shear testing (for application validation)
These tests confirm that the bolts meet specified mechanical performance criteria.
Third-Party Inspection (TPI)
Large infrastructure projects and mining equipment procurement programs often require third-party inspection before shipment.
Independent inspection agencies may verify:
- Material certification
- Dimensional compliance
- Mechanical test results
- Coating inspection
Certification Documentation
Plow bolts supplied for international projects may include certification according to European inspection standards.
EN 10204 Certification
Two common certification levels include:
EN 10204 3.1
Material test certificates issued by the manufacturer confirming compliance with specified mechanical and chemical properties.
EN 10204 3.2
Certification verified by an independent third-party inspection authority in addition to the manufacturer.
11. Industries Served
Plow bolts are used across multiple heavy equipment sectors where structural components are exposed to direct contact with abrasive materials such as soil, gravel, rock fragments, and construction debris.
These environments require fasteners capable of maintaining preload and structural integrity while remaining flush with the equipment surface.
Mining Industry
Mining equipment operates under some of the most demanding mechanical conditions encountered in industrial machinery.
Typical mining applications include:
- Bucket wear liners
- Loader cutting edges
- Dragline ground-contact plates
- Underground mining loader components
- Scraper blade edges
Mining equipment is frequently exposed to:
- High impact loads from rock contact
- Abrasive mineral particles
- Continuous vibration from heavy machinery
Plow bolts are used to secure replaceable wear plates and structural edges while maintaining flush surfaces that minimize abrasion damage to the fastener head.
Construction Equipment Manufacturing
Construction equipment manufacturers rely on plow bolts to secure wear components used in earthmoving machinery.
Typical equipment includes:
- Bulldozers
- Motor graders
- Scrapers
- Backhoe loaders
- Excavator buckets
Cutting edges and moldboards must maintain smooth working surfaces to allow soil and aggregate material to flow along the blade during operation.
Countersunk plow bolts prevent interference with this material flow.
Agricultural Machinery
Agricultural equipment uses plow bolts for fastening components exposed to soil movement.
Typical agricultural applications include:
- Moldboard plows
- Soil cultivators
- Field tillage equipment
- Seedbed preparation machines
In agricultural systems, soil movement across the blade surface requires smooth surfaces free of protruding fastener heads.
Plow bolts provide the required flush mounting geometry.
Earthmoving Equipment
Large earthmoving equipment used in infrastructure development depends on replaceable ground-engaging components.
Examples include:
- Bulldozer blade cutting edges
- Side cutters on excavator buckets
- Scraper edge systems
- Trenching machine cutting systems
Plow bolts allow these components to be replaced during maintenance cycles without altering the structural geometry of the equipment.
Infrastructure Development Equipment
Infrastructure projects rely heavily on earthmoving and excavation machinery. Plow bolts are commonly found in equipment used for:
- Highway construction
- Dam construction
- Pipeline trenching
- Rail infrastructure projects
Fasteners used in these machines must remain structurally reliable while operating in outdoor environments with variable temperature and moisture conditions.
Quarry Operations
Quarry operations involve crushing and moving large volumes of rock and aggregate material.
Equipment such as loaders and scrapers used in quarry operations rely on wear plates and replaceable edges secured by plow bolts.
Abrasion resistance and structural reliability are essential for fasteners operating in these environments.
Road Construction Machinery
Motor graders and asphalt preparation equipment incorporate blade systems used for surface leveling and grading.
Plow bolts secure cutting edges and moldboard components while maintaining smooth surfaces required for precise grading operations.
Heavy Industrial Equipment
In addition to earthmoving equipment, plow bolts may be used in specialized industrial machinery where flush fasteners are required.
Examples include:
- Conveyor wear plates
- Bulk material handling equipment
- Industrial scraper systems
These applications benefit from the same flush-head geometry used in earthmoving equipment.
12. Export Capability & Global Supply
Heavy equipment manufacturers and infrastructure contractors often require international sourcing for structural fasteners.
Plow bolts supplied for global equipment production must comply with international material standards, dimensional tolerances, and inspection documentation requirements.
Super Industries manufactures plow bolts for export to multiple industrial markets.
Export Regions
Typical export destinations include:
United States
Equipment manufacturers in the United States frequently specify fasteners according to SAE and ASTM standards.
Common grade requirements include:
- SAE Grade 5
- SAE Grade 8
- ASTM A449
Documentation requirements may include mechanical property reports and material traceability records.
Europe
European equipment manufacturers typically reference DIN or ISO fastener standards.
Compliance may involve:
- DIN dimensional specifications
- ISO property classes
- European material certification documentation
Middle East
Infrastructure development and mining operations in the Middle East require heavy equipment operating in high-temperature desert environments.
Fasteners used in these applications must maintain mechanical properties under elevated temperatures and abrasive conditions.
Southeast Asia
Rapid infrastructure development in Southeast Asia has increased demand for heavy construction equipment and related structural fasteners.
Applications include:
- Highway construction machinery
- Mining equipment
- Agricultural machinery
Africa
Mining operations in several African regions require robust fastening systems for earthmoving and mineral extraction equipment.
Plow bolts are commonly used for wear components in loaders, bulldozers, and excavators operating in mining environments.
Export Packaging Standards
Structural fasteners exported internationally must be packaged to prevent mechanical damage and corrosion during transit.
Typical export packaging methods include:
- Wooden crates with internal segregation
- Palletized steel containers
- Moisture-resistant wrapping materials
Packaging systems must maintain fastener integrity during extended shipping durations.
Container Loading Discipline
Large orders for plow bolts are typically shipped using standardized freight containers.
Loading procedures consider:
- Weight distribution across pallets
- Protection against movement during transport
- Separation of different bolt sizes or grades
Proper container loading prevents mechanical damage to threads and bolt heads.
Export Documentation
Global equipment procurement requires documentation supporting material compliance and traceability.
Typical documentation may include:
- Material test certificates
- Mechanical property reports
- Inspection records
- Heat treatment documentation
- Packing lists and commercial invoices
These records support procurement verification for equipment manufacturers and EPC contractors.
Procurement & Installation Guidelines
Correct installation practices are essential to ensure that plow bolts perform reliably within heavy equipment assemblies.
The following guidelines are commonly referenced during equipment assembly and maintenance.
Countersunk Hole Preparation
Equipment components must include countersunk holes that match the bolt head angle.
Proper hole preparation ensures:
- Full seating contact between the bolt head and the plate
- Uniform load distribution
- Prevention of localized deformation
Incorrect countersink geometry may cause uneven stress distribution.
Bolt Insertion Orientation
Plow bolts are typically inserted from the wear surface side so that the head sits flush within the countersunk hole.
The threaded portion extends through the structural component where the nut is installed.
This orientation protects the bolt head from abrasion.
Nut Tightening Practices
Nuts should be tightened using calibrated torque tools to achieve the specified preload.
Torque values depend on:
- Bolt diameter
- Material grade
- Lubrication condition
Uniform torque application across multiple bolts ensures even load distribution across the joint.
Torque Control Methods
Common torque control tools include:
- Manual torque wrenches
- Pneumatic torque tools
- Hydraulic torque multipliers
Large diameter plow bolts used in mining equipment may require hydraulic tightening systems.
Periodic Inspection
Equipment maintenance programs typically include periodic inspection of plow bolt joints.
Inspection may include:
- Checking for loosened nuts
- Inspecting wear plate condition
- Verifying that bolt heads remain flush with the surface
If excessive wear occurs around the countersunk seat, the plate may require replacement.
Replacement Guidelines
Plow bolts should be replaced when:
- Threads are damaged
- Bolt heads show significant wear
- Bolt preload cannot be maintained
Replacement ensures continued structural integrity of wear plate assemblies.
Custom Engineering Capabilities
Heavy equipment manufacturers often require fasteners with non-standard dimensions to match proprietary equipment designs.
Custom engineering capabilities may include the following.
Non-Standard Head Dimensions
Equipment manufacturers sometimes specify head diameters larger than standard sizes to increase seating area within the countersunk hole.
Custom forging dies can produce these configurations.
Custom Square Neck Dimensions
Square neck geometry may be modified to match equipment hole tolerances or anti-rotation requirements.
High-Strength Plow Bolts
For heavy mining equipment, plow bolts may be manufactured using higher-strength alloy steels with controlled heat treatment.
This increases shear capacity and fatigue resistance.
Specialized Surface Coatings
Certain environments require enhanced corrosion protection.
Examples include:
- PTFE coatings for reduced friction
- Hot-dip galvanizing for outdoor infrastructure equipment
- Phosphate coatings for improved lubrication
OEM Identification Marking
Equipment manufacturers may require proprietary head markings or identification codes.
These markings support traceability during equipment service and maintenance.
Technical Conclusion
Plow bolts serve a specialized role in heavy equipment fastening systems where flush mounting, abrasion resistance, and structural load capacity are required.
Their countersunk head geometry allows them to operate within ground-contact environments without creating protrusions that would accelerate wear or interfere with equipment operation.
Proper design and manufacturing of plow bolts require attention to:
- Material grade selection
- Heat treatment control
- Dimensional accuracy
- Surface coating requirements
- Mechanical property verification
When correctly specified and installed, plow bolts provide reliable fastening performance for ground-engaging components in mining, construction, agricultural, and infrastructure equipment.
Manufacturers supplying plow bolts to international equipment markets must maintain consistent dimensional control, material traceability, and inspection documentation to support OEM production requirements and global procurement standards.