
STUD BOLTS
Super Industries
“Global Manufacturer of Heavy & Custom Engineered Fasteners for Oil & Gas, Power & EPC Contractors.”
1. Industry Context & System Relevance
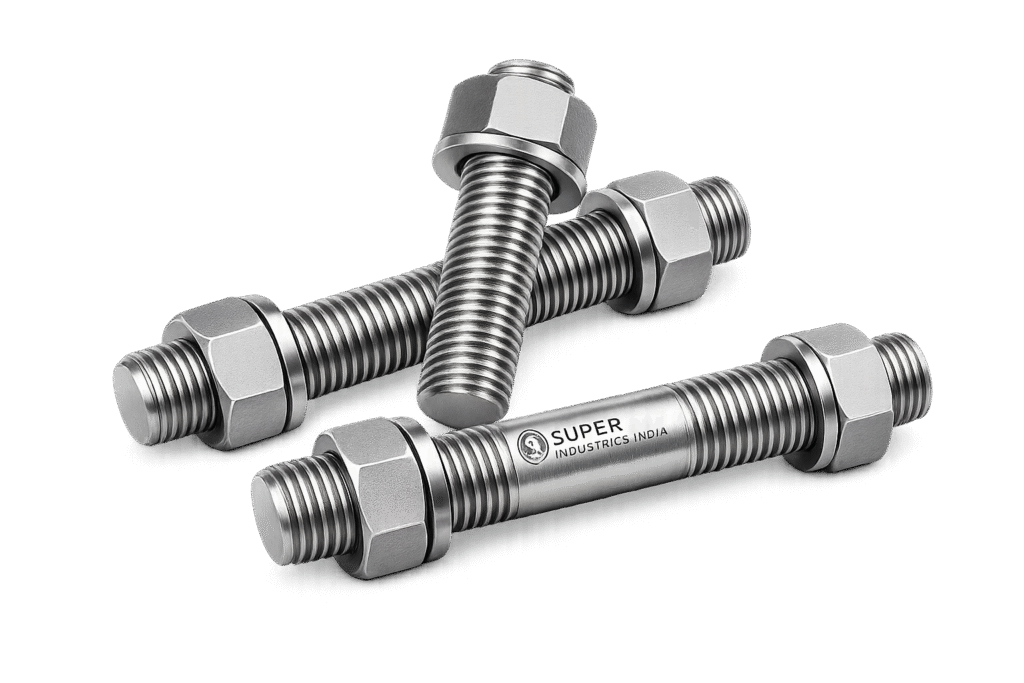
Bolted flange joints represent one of the most critical mechanical sealing systems used across pressure-retaining industrial equipment. In piping systems operating under high internal pressure, temperature variation, and cyclic loading conditions, the reliability of the bolting assembly directly influences the structural integrity and leak-tight performance of the joint.
Within these systems, Stud Bolts serve as the primary mechanical fasteners used to generate the clamping force required to compress a gasket between mating flanges. These fasteners are widely specified in accordance with internationally recognized piping and pressure equipment standards, particularly in applications governed by ASME piping codes.
Typical industrial installations where stud bolts are used include:
• Oil and gas transmission pipelines
• Petroleum refineries
• Petrochemical processing plants
• LNG liquefaction and regasification terminals
• Offshore production platforms
• Thermal and combined-cycle power plants
• Pressure vessel assemblies
• Shell-and-tube heat exchangers
• Process valves and pipeline isolation equipment
In these environments, flange joints are subjected to multiple operating stresses including internal pressure, thermal expansion, vibration, and mechanical loading from connected equipment. The bolting system must therefore maintain consistent clamping force across the gasket interface throughout the entire service cycle.
Stud bolts are selected in these applications because they provide more consistent preload distribution compared with conventional bolt configurations. Their geometry and installation method allow the joint to maintain controlled stress across the flange faces, which directly influences sealing reliability.
Advantages of Stud Bolts in Flange Joints
When compared with conventional hex bolts, stud bolts provide several engineering advantages in pressure-retaining systems:
Uniform Load Distribution
Because the stud is threaded along its entire length and engages two separate heavy hex nuts, the load applied to the flange joint is distributed symmetrically across the stud. This minimizes localized stress concentrations and promotes balanced bolt loading.
Improved Gasket Compression Control
Gasket sealing performance is directly dependent on the uniformity of compressive load applied across the flange interface. Stud bolts allow controlled tightening from both sides of the joint, enabling technicians to achieve more consistent gasket seating stress.
Enhanced Maintenance Accessibility
During equipment maintenance, the stud typically remains installed in one flange while the nuts are removed. This allows easier disassembly of piping systems without removing the entire fastener from the joint.
Reduced Thread Wear on Flanges
In many systems, flanges are manufactured from corrosion-resistant alloys or specialized steels. By using studs with separate nuts, the threads in the flange body are not subjected to repeated tightening cycles.
Improved Reliability in High-Pressure Service
High-pressure piping systems require predictable bolt tension behavior. Stud bolts provide greater control of preload and are therefore widely specified in pressure vessel and piping design codes.
For these reasons, stud bolts have become the standard fastening solution in bolted flange joints governed by ASME piping and pressure equipment standards.
2. Technical Definition
A Stud Bolt is a fully threaded mechanical fastener designed to be used in combination with two heavy hex nuts to produce clamping force in bolted flange assemblies.
The stud is inserted through aligned bolt holes of mating flanges, and nuts are tightened from both ends to generate tensile load within the stud. This tensile load translates into compressive force across the gasketed flange interface.
From a mechanical standpoint, the stud bolt operates as a tension member within the bolted joint. When torque is applied to the nuts, the stud experiences elastic elongation while the flange faces compress the gasket material between them.
Basic Characteristics
A typical stud bolt used in pressure flange systems exhibits the following characteristics:
• Continuous threading along the full length
• Use with two heavy hex nuts
• High tensile strength material grades
• Controlled heat treatment condition
• Standardized thread form and pitch
Stud bolts are commonly manufactured according to specifications defined in international standards for mechanical fasteners used in pressure equipment.
Types of Stud Bolts
Different configurations of stud bolts are used depending on installation requirements and equipment design.
Double-End Stud Bolts
Double-end studs have threaded ends with an unthreaded shank section in the center.
Characteristics:
• Threads at both ends
• Center section without threads
• Typically used where permanent installation in equipment is required
These are often used in equipment such as pump casings or pressure vessel covers.
Fully Threaded Stud Bolts
Fully threaded studs contain threads across their entire length.
Characteristics:
• Continuous threading
• Uniform load distribution along the length
• Commonly used in flange joints
This configuration is widely used in pipeline flange connections governed by ASME flange standards.
Tap-End Studs
Tap-end studs contain one short threaded section intended to be permanently installed in a tapped hole, while the opposite end receives a nut.
Applications include:
• Engine blocks
• Turbine housings
• Pump casings
Continuous Threaded Rods
Threaded rods resemble stud bolts but are typically supplied in longer lengths.
Characteristics:
• Fully threaded bars
• Often supplied in meter lengths
• Cut to required dimensions during installation
Threaded rods are generally used in structural applications rather than critical flange sealing systems.
Stud Bolts vs Hex Bolts
The functional differences between stud bolts and hex bolts become significant in pressure-retaining flange joints.
| Feature | Stud Bolts | Hex Bolts |
|---|---|---|
| Thread Configuration | Fully threaded | Partial threading |
| Nuts Used | Two heavy hex nuts | One nut |
| Load Distribution | Symmetrical | Non-symmetrical |
| Installation | Through flange holes | Inserted from one side |
| Maintenance | Easier flange separation | Bolt removal required |
Because stud bolts allow controlled tightening from both sides of the joint, they are generally preferred in piping systems governed by ASME flange standards.
Stud Bolts vs Threaded Rods
Although stud bolts and threaded rods may appear similar, their intended applications differ significantly.
| Parameter | Stud Bolts | Threaded Rods |
|---|---|---|
| Application | Pressure flange joints | Structural fastening |
| Mechanical strength | High tensile grades | Variable |
| Manufacturing control | Tight tolerance | Less strict |
| Certification | Pressure system standards | General fastener standards |
Stud bolts used in industrial piping systems are manufactured to stricter quality requirements to ensure predictable mechanical performance under high loads.
Super Industries
Global Manufacturer of Heavy & Custom Engineered Fasteners & Flanges
3. Engineering & Clamping Principle
The reliability of a bolted flange joint depends on the controlled application of tensile load in the stud bolts.
When a nut is tightened, torque applied to the nut is converted into axial tensile force in the stud. This tensile force stretches the stud elastically and generates compressive force across the flange faces.
The stud behaves similarly to a tension spring within the joint.
Bolt Preload Mechanics
Preload refers to the initial tensile load applied to a fastener during tightening.
This preload is critical because it determines the clamping force available to maintain gasket compression during operation.
The relationship between bolt preload and stress is expressed by the following equation:

Where:
σ = Bolt stress
F = Applied bolt force
A = Tensile stress area of the stud
Proper preload ensures that the joint remains sealed even when internal pressure attempts to separate the flanges.
Elastic Elongation of Stud Bolts
During tightening, the stud bolt elongates elastically. This elongation creates stored energy within the fastener, which acts as the clamping force holding the joint together.
Elastic elongation is essential because it allows the bolt to maintain tension even if small amounts of joint relaxation occur.
The amount of elongation depends on:
• Stud length
• Material modulus of elasticity
• Applied preload
Longer studs provide greater elastic stretch and therefore better preload stability.
Gasket Compression Mechanics
The primary function of stud bolts in a flange joint is to compress the gasket material between two flange faces.
Gasket compression must be sufficient to:
• Fill surface irregularities in the flange faces
• Create a pressure-tight seal
• Resist internal fluid pressure
The clamping force produced by the stud bolts must exceed the force generated by internal pressure attempting to separate the flanges.
Torque–Tension Relationship
The tightening torque applied to the nut produces preload in the stud bolt.
The relationship between torque and preload is expressed by the following equation:
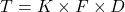
Where:
T = Applied torque
K = Nut factor (friction coefficient)
F = Bolt preload force
D = Nominal bolt diameter
This relationship illustrates that friction conditions significantly influence the final bolt preload achieved during tightening.
Joint Integrity
A properly designed flange joint must maintain sufficient clamping force under all operating conditions.
Loss of bolt tension may result from:
• Thermal expansion
• Gasket creep
• Bolt relaxation
• External mechanical loads
Stud bolts are selected and sized so that the preload remains above the minimum required gasket seating load throughout the service life of the joint.
Load Sharing Between Studs
In multi-bolt flange joints, the total load required to seal the gasket is shared among all installed studs.
Uniform tightening is essential to ensure that all studs carry approximately equal load.
Uneven tightening can lead to:
• Localized gasket overstress
• Flange distortion
• Leakage paths
Proper tightening sequences are therefore critical during installation.
Prevention of Flange Separation
Internal pressure within a piping system creates a separating force on the flange joint.
Stud bolts must provide sufficient tensile resistance to counteract this force.
The required bolt load is calculated based on:
• Internal pressure
• Flange diameter
• Gasket seating area
Engineering design standards define the minimum number and size of stud bolts required for each flange rating.
Bolt Stress vs Gasket Seating Load
The design of flange joints requires balancing two factors:
- Bolt stress must remain within allowable limits of the fastener material.
- Gasket seating load must be sufficient to achieve leak-tight sealing.
Stud bolt materials and dimensions are therefore selected to ensure that the bolts can sustain the required preload without yielding.
Elastic Strain Theory
The mechanical behavior of stud bolts during tightening follows principles of elastic strain.
Within the elastic range of the material:
• Stress is proportional to strain
• The bolt returns to its original length when unloaded
If the bolt is tightened beyond its yield strength, permanent deformation occurs and the fastener may lose its ability to maintain clamping force.
Therefore, torque values and tightening procedures must be carefully controlled to keep bolt stress within allowable limits.
4. Applicable Standards (ASTM / ASME / DIN / ISO)
The design, manufacture, inspection, and application of Stud Bolts in pressure-retaining flange joints are governed by internationally recognized engineering standards. These standards define dimensional tolerances, mechanical properties, material grades, heat treatment requirements, and testing procedures required to ensure consistent performance in industrial bolting systems.
For EPC projects and pressure piping installations, stud bolts must comply with specifications referenced in piping codes and flange design standards.
The most commonly applied standards for stud bolts are listed below.
ASTM A193 — Alloy Steel Bolting for High Temperature Service
ASTM A193 is one of the primary specifications governing high-strength alloy steel bolting used in pressure vessels, piping systems, and high-temperature applications.
Typical grades include:
• ASTM A193 B7
• ASTM A193 B7M
• ASTM A193 B16
These grades are produced from alloy steels subjected to controlled heat treatment to achieve the required strength and hardness levels.
Typical applications include:
• High-pressure refinery piping
• Petrochemical reactors
• Steam systems
• High-temperature pipeline flanges
ASTM A193 also specifies:
• Mechanical properties
• Heat treatment requirements
• Chemical composition limits
• Hardness testing criteria
ASTM A320 — Low Temperature Bolting
ASTM A320 covers alloy steel and stainless steel bolting materials intended for low-temperature service conditions.
Common grades include:
• ASTM A320 L7
• ASTM A320 L7M
These materials are designed to retain toughness and ductility under sub-zero temperatures where conventional alloy steels may become brittle.
Typical applications include:
• LNG facilities
• Cryogenic processing systems
• Low-temperature hydrocarbon pipelines
• Arctic oil and gas installations
ASTM A320 materials must meet additional requirements such as:
• Charpy impact testing
• Heat treatment verification
• Toughness testing at specified temperatures
ASTM A307 — Carbon Steel Bolting
ASTM A307 specifies carbon steel bolts and studs used in general engineering applications.
The specification includes several grades, typically used in:
• Structural steel assemblies
• Low-pressure piping systems
• Non-critical industrial equipment
Compared with ASTM A193 materials, ASTM A307 bolts have lower strength and are generally not used in high-pressure or high-temperature service.
ASTM A194 — Heavy Hex Nuts
Stud bolts are typically used with heavy hex nuts manufactured in accordance with ASTM A194.
Common nut grades include:
• ASTM A194 2H
• ASTM A194 7
• ASTM A194 8
These nuts are designed to match the strength and temperature requirements of the corresponding stud bolt materials.
Proper pairing of studs and nuts is essential to prevent thread stripping or joint failure during tightening.
ASME B16.5 — Pipe Flanges and Flanged Fittings
ASME B16.5 is the primary standard governing pipe flanges used in piping systems up to NPS 24.
The standard defines:
• Flange dimensions
• Bolt hole patterns
• Number of studs required per flange
• Stud bolt diameters
• Flange pressure classes
Typical pressure classes include:
• Class 150
• Class 300
• Class 600
• Class 900
• Class 1500
• Class 2500
Stud bolt lengths and quantities used in flange joints are determined directly from ASME B16.5 dimensional tables.
ASME B18.31.2 — Stud Bolts and Threaded Rods
ASME B18.31.2 defines dimensional and mechanical requirements for stud bolts and threaded rods.
The standard includes:
• Thread dimensions
• Tolerance limits
• Length requirements
• Thread class definitions
This standard ensures compatibility between studs and nuts used in pressure bolting systems.
DIN 976 — Threaded Rods
DIN 976 is a widely used European standard covering continuously threaded rods.
Although threaded rods may resemble stud bolts, DIN 976 rods are generally used for structural applications rather than pressure-retaining flange systems.
ISO Metric Thread Standards
Thread geometry used in stud bolts is typically defined according to ISO metric thread standards or Unified Thread Standards (UTS) depending on project specification.
These standards define:
• Thread pitch
• Thread angle
• Thread tolerance class
• Major and minor diameter limits
Proper thread compatibility between stud bolts and nuts ensures uniform load transfer and reduces the risk of galling or thread failure.
5. Material & Grade Options
The material selected for stud bolts depends primarily on operating conditions such as pressure, temperature, corrosion environment, and mechanical loading.
In EPC projects, material grades are specified according to ASTM standards to ensure consistent mechanical performance.
The most common categories of stud bolt materials are described below.
Carbon Steel Stud Bolts
Carbon steel studs are used in moderate temperature applications where corrosion resistance is not a primary concern.
Typical grades include:
• ASTM A193 B7
• ASTM A193 B7M
ASTM A193 B7
ASTM A193 B7 is one of the most widely used stud bolt materials in refinery and petrochemical industries.
Characteristics include:
• High tensile strength
• Good fatigue resistance
• Suitable for elevated temperature service
Typical applications:
• Refinery process piping
• Petrochemical plants
• Steam pipelines
ASTM A193 B7M
B7M is a modified version of B7 with controlled hardness levels.
Advantages include:
• Reduced susceptibility to stress corrosion cracking
• Improved resistance in sour service environments
B7M is commonly specified in hydrogen sulfide (H₂S) environments governed by sour service requirements.
Stainless Steel Stud Bolts
Stainless steel stud bolts are used where corrosion resistance is required.
Common grades include:
• ASTM A193 B8
• ASTM A193 B8M
ASTM A193 B8
B8 studs are manufactured from austenitic stainless steel equivalent to Type 304.
Characteristics include:
• Corrosion resistance in atmospheric conditions
• Resistance to oxidation at moderate temperatures
Applications include:
• Chemical processing plants
• Water treatment systems
• Food processing equipment
ASTM A193 B8M
B8M studs are equivalent to stainless steel Type 316.
Advantages include:
• Improved resistance to chlorides
• Enhanced corrosion resistance in marine environments
These studs are widely used in offshore installations and marine piping systems.
Alloy Steel Stud Bolts
High-temperature and high-pressure applications require alloy steel grades with enhanced strength.
ASTM A193 B16
B16 stud bolts are manufactured from chromium-molybdenum alloy steels.
Characteristics include:
• High temperature strength
• Resistance to creep deformation
• Good fatigue resistance
Typical applications include:
• Steam turbines
• Boiler systems
• High-temperature pressure vessels
Low Temperature Service Bolting
For cryogenic and sub-zero applications, stud bolts must maintain toughness at low temperatures.
ASTM A320 L7
L7 studs are produced from alloy steels designed for low-temperature service.
Characteristics:
• Excellent toughness at low temperatures
• Resistance to brittle fracture
Applications include:
• LNG plants
• Cryogenic storage tanks
• Low-temperature pipelines
ASTM A320 L7M
L7M studs are similar to L7 but include hardness limitations to reduce susceptibility to stress corrosion cracking.
Special Alloy Stud Bolts
In highly corrosive or high-temperature environments, special alloy materials are used.
Examples include:
• Duplex stainless steel
• Super duplex stainless steel
• Nickel-based alloys
• Inconel alloys
These materials are typically used in specialized process environments such as offshore subsea systems or chemical processing reactors.
Material Comparison Table
| Grade | Yield Strength | Tensile Strength | Temperature Range | Corrosion Resistance | Typical Industry Use |
|---|---|---|---|---|---|
| ASTM A193 B7 | ~720 MPa | ~860 MPa | -29°C to 450°C | Moderate | Oil & Gas piping |
| ASTM A193 B7M | ~620 MPa | ~760 MPa | -29°C to 450°C | Improved SCC resistance | Sour service pipelines |
| ASTM A193 B8 | ~205 MPa | ~515 MPa | -196°C to 425°C | Good | Chemical plants |
| ASTM A193 B8M | ~205 MPa | ~515 MPa | -196°C to 425°C | High | Marine installations |
| ASTM A193 B16 | ~760 MPa | ~860 MPa | Up to 550°C | Moderate | High-temp steam |
| ASTM A320 L7 | ~720 MPa | ~860 MPa | Down to -101°C | Moderate | LNG facilities |
6. Heat Treatment of Stud Bolts
Heat treatment is a critical manufacturing stage used to achieve the required mechanical properties in stud bolt materials.
The heat treatment process influences:
• Strength
• Hardness
• Ductility
• Impact toughness
Different material grades require specific heat treatment procedures.
Quenching and Tempering
Quenching and tempering is commonly applied to alloy steel stud bolts such as ASTM A193 B7.
Process sequence:
- Heating steel to the austenitizing temperature
- Rapid cooling (quenching)
- Controlled reheating (tempering)
This process produces a tempered martensitic microstructure with high strength and good toughness.
Normalizing
Normalizing is applied to some carbon steel materials to refine the grain structure.
The process involves:
• Heating above the critical temperature
• Air cooling
Normalizing improves uniformity in mechanical properties.
Solution Annealing for Stainless Steel
Austenitic stainless steel stud bolts such as ASTM A193 B8 and B8M undergo solution annealing.
This process:
• Dissolves chromium carbides
• Restores corrosion resistance
• Improves ductility
The material is heated to high temperature and rapidly cooled.
Stress Relieving
Stress relieving may be performed after thread rolling or machining operations.
The objective is to:
• Reduce residual stresses
• Improve dimensional stability
Stress relieving is particularly important for large diameter studs used in heavy industrial equipment.
Hardness Control
Hardness levels must remain within specified limits to prevent issues such as:
• Hydrogen embrittlement
• Stress corrosion cracking
• Reduced ductility
Hardness testing is performed according to ASTM specifications for each material grade.
Charpy Impact Testing
For low-temperature service materials such as ASTM A320 L7, Charpy impact testing is required to verify material toughness.
The test measures the energy absorbed during fracture at specified temperatures.
Adequate impact toughness ensures the stud bolt will not experience brittle failure during service.
7. Manufacturing Process for Stud Bolts
The manufacturing of stud bolts involves a controlled sequence of operations designed to ensure dimensional accuracy and consistent mechanical performance.
1. Raw Material Inspection
Manufacturing begins with certified steel bars supplied with mill test certificates.
Incoming inspection includes:
• Chemical composition verification
• Visual inspection
• Dimensional verification
2. Bar Cutting
Steel bars are cut into required lengths using automated cutting equipment.
The cut length corresponds to the final stud bolt length plus machining allowances.
3. Thread Rolling or Thread Cutting
Threads are produced either by:
• Thread rolling
• Thread cutting
Thread rolling is preferred for high-strength studs because it improves fatigue strength.
4. Heat Treatment
Studs are heat treated according to material grade requirements.
This stage establishes the required mechanical properties of the fastener.
5. Straightening
After heat treatment, studs may undergo straightening to ensure proper alignment and dimensional accuracy.
6. Surface Treatment
Surface finishes may be applied depending on corrosion protection requirements.
7. Marking
Stud bolts are marked according to material grade and manufacturer identification requirements defined in ASTM specifications.
8. Dimensional Inspection
Inspection includes:
• Length verification
• Thread pitch measurement
• Straightness check
Thread gauges are used to confirm thread tolerance compliance.
9. Final Packing
Stud bolts are packed according to project or export requirements, typically including protective coatings and corrosion-prevention packaging.
Thread Rolling vs Thread Cutting
Thread rolling offers several advantages compared with thread cutting.
Thread Rolling
• Produces stronger threads due to cold working
• Improves fatigue resistance
• Provides smoother surface finish
Thread Cutting
• Suitable for large diameters or special threads
• Lower tooling force requirements
8. Stud Bolt Dimensional Framework
In pressure-retaining flange assemblies, the dimensional configuration of Stud Bolts must correspond precisely with flange geometry, bolt-hole spacing, gasket thickness, and nut dimensions. These parameters are primarily derived from flange standards used in piping systems.
The dimensional logic governing stud bolt sizing typically references flange dimensions specified in flange design standards used in piping engineering practice.
Key dimensional parameters include:
• Nominal stud diameter
• Thread pitch
• Stud length
• Nut height
• Washer thickness (if specified)
• Required thread projection beyond nut
Stud bolt length must be selected to allow adequate thread engagement in the nuts while maintaining appropriate projection beyond the outer face of the nut after tightening.
Stud Bolt Length Determination
Stud length used in flange joints is typically calculated based on:
• Flange thickness of both flanges
• Gasket thickness
• Height of two heavy hex nuts
• Required thread projection
A simplified engineering expression for stud length is:
Stud Length ≈
(Flange thickness 1) +
(Flange thickness 2) +
(Gasket thickness) +
(2 × Nut height) +
(Thread projection allowance)
Thread projection typically ranges from 1 to 3 threads beyond the nut to allow visual confirmation of proper engagement.
Stud Bolt Dimension Table
Typical dimensional ranges for stud bolts used in industrial flange systems are summarized below.
| Nominal Diameter | Thread Pitch | Standard Length Range | Nut Size | Weight per Meter |
|---|---|---|---|---|
| M12 / ½” | 1.75 mm | 40–200 mm | 19 mm | 0.89 kg |
| M16 / ⅝” | 2.0 mm | 50–300 mm | 24 mm | 1.58 kg |
| M20 / ¾” | 2.5 mm | 60–350 mm | 30 mm | 2.47 kg |
| M24 / 1″ | 3.0 mm | 70–400 mm | 36 mm | 3.85 kg |
| M30 / 1¼” | 3.5 mm | 80–500 mm | 46 mm | 6.02 kg |
| M36 / 1½” | 4.0 mm | 100–600 mm | 55 mm | 8.80 kg |
Actual stud dimensions used in flange joints are determined by the flange pressure class and nominal pipe size.
Thread Engagement Requirements
Proper thread engagement is essential to ensure that load transfer between stud and nut occurs without thread stripping.
Engineering guidelines typically recommend:
Minimum thread engagement ≥ 1 × nominal stud diameter
For high-strength bolting assemblies used in pressure equipment, heavy hex nuts provide deeper thread engagement compared with standard hex nuts.
9. Stud Bolt Grade Strength Table
The mechanical strength of stud bolts is defined by material specifications such as ASTM A193 or ASTM A320.
Typical mechanical properties for common stud bolt grades are summarized below.
| Grade | Yield Strength | Ultimate Tensile Strength | Hardness Range |
|---|---|---|---|
| ASTM A193 B7 | 720 MPa | 860 MPa | 24–35 HRC |
| ASTM A193 B7M | 620 MPa | 760 MPa | 20–30 HRC |
| ASTM A193 B16 | 760 MPa | 860 MPa | 28–36 HRC |
| ASTM A193 B8 | 205 MPa | 515 MPa | 95 HRB |
| ASTM A193 B8M | 205 MPa | 515 MPa | 95 HRB |
| ASTM A320 L7 | 720 MPa | 860 MPa | 24–35 HRC |
Mechanical properties must be verified during production through standardized testing procedures.
10. Torque Guidance for Stud Bolt Tightening
Achieving proper preload in stud bolts depends on the torque applied during installation. However, torque alone does not directly produce bolt tension; friction between threads and nut surfaces significantly influences the final preload achieved.
The fundamental relationship between torque, preload, and bolt diameter is expressed as:
Where:
T = tightening torque
K = friction factor (nut factor)
F = desired preload
D = nominal bolt diameter
Lubrication applied to threads can significantly alter the friction coefficient and therefore the torque required to achieve a given preload.
Stud Bolt Torque Chart (Typical Engineering Reference)
The following torque values represent typical ranges used in industrial flange assembly. Actual torque values may vary depending on lubrication conditions and project specifications.
| Stud Size | Recommended Torque | Lubricated Torque | Dry Torque | Typical Grade |
|---|---|---|---|---|
| ½” | 70 Nm | 60 Nm | 85 Nm | B7 |
| ⅝” | 140 Nm | 120 Nm | 160 Nm | B7 |
| ¾” | 240 Nm | 200 Nm | 270 Nm | B7 |
| 1″ | 470 Nm | 400 Nm | 520 Nm | B7 |
| 1¼” | 820 Nm | 700 Nm | 900 Nm | B7 |
| 1½” | 1450 Nm | 1250 Nm | 1600 Nm | B16 |
These values are typically used as guidance during controlled tightening procedures.
11. Bolt Preload Calculation Guide
Correct preload in a stud bolt ensures that the clamping force across the gasketed flange joint remains sufficient to prevent leakage.
The stress experienced by the stud bolt can be calculated using the following relationship:
Where:
σ = Bolt stress
F = Applied bolt force
A = Tensile stress area
Preload Calculation from Torque
The preload generated during tightening can be estimated using:

Where:
F = Bolt preload force
T = Applied torque
K = Nut factor
D = Bolt diameter
This equation shows that torque must be carefully controlled to avoid overloading the stud bolt.
Engineering Calculation Example
Assume the following parameters for a flange joint:
Stud diameter = 24 mm
Applied torque = 400 Nm
Nut factor = 0.2
Using the preload equation:
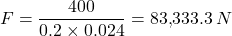
Resulting preload:
F ≈ 83,000 N
This preload contributes to the clamping force required to compress the gasket and maintain sealing integrity.
Mechanical Property Table
Mechanical performance characteristics of stud bolt materials are summarized below.
| Material Grade | Yield Strength | Tensile Strength | Elongation | Hardness |
|---|---|---|---|---|
| ASTM A193 B7 | 720 MPa | 860 MPa | 16% | 24–35 HRC |
| ASTM A193 B16 | 760 MPa | 860 MPa | 16% | 28–36 HRC |
| ASTM A193 B8 | 205 MPa | 515 MPa | 30% | 95 HRB |
| ASTM A193 B8M | 205 MPa | 515 MPa | 30% | 95 HRB |
| ASTM A320 L7 | 720 MPa | 860 MPa | 16% | 24–35 HRC |
These mechanical properties ensure that the stud bolts remain within the elastic deformation range during tightening and operation.
Corrosion Resistance Comparison
Material selection for stud bolts often depends on the environmental conditions in which the fasteners will operate.
Corrosion behavior varies significantly between carbon steels, stainless steels, and high-alloy materials.
The following table provides a comparative overview.
| Material | Marine Environment | Acidic Environment | High Humidity | Hydrocarbon Service |
|---|---|---|---|---|
| Carbon Steel | Poor | Poor | Moderate | Good |
| Stainless Steel 304 | Moderate | Moderate | Good | Good |
| Stainless Steel 316 | Good | Good | Excellent | Good |
| Duplex Stainless Steel | Excellent | Good | Excellent | Excellent |
| Alloy Steel | Moderate | Poor | Moderate | Excellent |
Protective coatings may also be applied to improve corrosion resistance.
Inspection & Quality Control Methods
Inspection and quality control are essential to ensure that stud bolts meet the mechanical and dimensional requirements specified in international standards.
Quality verification begins with raw material inspection and continues through all stages of manufacturing.
The following testing and inspection methods are commonly applied.
Positive Material Identification (PMI)
PMI testing is used to verify the chemical composition of the material.
Techniques include:
• X-ray fluorescence (XRF)
• Optical emission spectroscopy (OES)
PMI ensures that the stud bolt material matches the specified alloy grade.
Ultrasonic Testing (UT)
Ultrasonic inspection detects internal discontinuities within the stud material.
This method is used to identify:
• Internal cracks
• Inclusions
• Laminations
UT testing is often required for large diameter stud bolts used in critical equipment.
Magnetic Particle Inspection (MPI)
MPI is used for detecting surface and near-surface defects in ferromagnetic materials.
Typical defects detected include:
• Surface cracks
• Quench cracks
• Grinding cracks
Dye Penetrant Testing (DPT)
Dye penetrant inspection is used primarily for stainless steel studs where magnetic particle testing is not applicable.
This method detects surface-breaking defects.
Hardness Testing
Hardness testing ensures that stud bolts fall within specified hardness limits.
Common methods include:
• Rockwell hardness testing
• Brinell hardness testing
Maintaining correct hardness levels is important to prevent issues such as hydrogen embrittlement.
Dimensional Inspection
Dimensional checks verify that the stud bolts comply with specified tolerances.
Inspection parameters include:
• Overall length
• Thread pitch
• Thread profile
• Straightness
Thread plug gauges and ring gauges are used to confirm compliance with thread standards.
Thread Gauge Inspection
Thread gauge inspection ensures compatibility between stud bolts and mating nuts.
Inspection tools include:
• Go gauges
• No-go gauges
These gauges confirm that threads fall within acceptable tolerance ranges.
Certification Documentation
Industrial stud bolts supplied to EPC projects are typically delivered with material and inspection documentation.
Certification commonly includes:
EN 10204 3.1 certification
This document verifies that the product complies with specified material properties and testing requirements.
For critical projects, additional verification may include:
EN 10204 3.2 certification
This certification requires validation by an independent third-party inspection agency.
12. Industries Served
The use of Stud Bolts in pressure-retaining flange joints spans a wide range of industrial sectors where piping systems operate under high pressure, high temperature, or corrosive service environments. The structural reliability of these bolting assemblies directly influences the operational safety of processing equipment, pressure vessels, and pipeline infrastructure.
Stud bolts are therefore specified extensively across industries governed by internationally recognized mechanical and piping standards.
Oil & Gas Upstream Operations
Upstream oil and gas facilities include drilling installations, wellhead assemblies, and production platforms where high-pressure fluids are transported through complex piping networks.
Stud bolts are used in flange joints associated with:
• Wellhead equipment
• Christmas tree assemblies
• Drilling manifolds
• Flowline piping systems
• High-pressure valves
These installations often operate under fluctuating pressures and temperatures, requiring bolting systems capable of maintaining preload stability under dynamic conditions.
Petroleum Refineries
Refineries contain extensive piping networks connecting reactors, distillation columns, heat exchangers, and storage systems.
Stud bolts are used in flange joints across units such as:
• Crude distillation units
• Catalytic cracking systems
• Hydroprocessing units
• Sulfur recovery systems
• Heat exchanger networks
Refinery environments often expose bolting materials to elevated temperatures, hydrocarbon fluids, and corrosive compounds. Material selection for stud bolts therefore depends on process conditions and applicable design codes.
Petrochemical Processing Plants
Petrochemical facilities process hydrocarbons into chemical intermediates and polymer products. These plants include complex reactor systems operating at high pressures and temperatures.
Typical stud bolt applications include:
• Reactor flange assemblies
• Chemical transfer pipelines
• Heat exchanger connections
• Compressor discharge systems
• Storage tank piping systems
The integrity of bolted flange joints is critical to maintaining containment of process fluids in these facilities.
LNG Terminals
Liquefied natural gas facilities operate under extremely low temperatures during liquefaction, storage, and regasification processes.
Stud bolts used in LNG installations must maintain mechanical toughness under cryogenic conditions.
Typical applications include:
• LNG storage tank piping
• Cryogenic transfer lines
• Pump discharge flanges
• Regasification units
Low-temperature material grades are often specified for these applications to ensure resistance to brittle fracture.
Power Generation Plants
Thermal and combined-cycle power plants contain high-pressure steam systems used to drive turbines and generate electricity.
Stud bolts are used extensively in:
• Boiler systems
• Steam turbine casing joints
• Heat exchanger assemblies
• High-pressure steam pipelines
• Condenser systems
These systems operate under elevated temperature and pressure conditions where bolting materials must resist creep deformation and relaxation.
Offshore Production Platforms
Offshore installations present additional challenges due to exposure to marine environments and corrosive atmospheric conditions.
Stud bolts are used in flange joints within:
• Subsea pipeline connections
• Offshore processing modules
• Pumping systems
• Gas compression units
Materials with improved corrosion resistance are often specified for offshore applications.
Hydrogen Processing Facilities
Hydrogen production and processing systems involve high-pressure service environments and may present hydrogen embrittlement risks.
Stud bolt materials used in hydrogen service must therefore be carefully selected and heat treated to maintain adequate mechanical properties.
Heavy Industrial Equipment
Large-scale industrial equipment assemblies also rely on stud bolts for structural fastening.
Applications include:
• Large pressure vessel closures
• Turbine casings
• Compressor housings
• Industrial reactor assemblies
In these cases, stud bolts may be manufactured in larger diameters and custom lengths.
13. Export Capability & Global Supply
Stud bolts supplied to international EPC projects must meet documentation, packaging, and traceability requirements associated with global procurement standards.
Super Industries manufactures stud bolts intended for supply to international markets where mechanical fasteners are evaluated as part of large-scale capital equipment procurement programs.
Global Supply Regions
Stud bolts manufactured for industrial flange systems are supplied to engineering and procurement organizations operating in multiple geographic regions.
Typical export destinations include:
• United States
• Europe
• Middle East
• Southeast Asia
These markets require strict adherence to international material and manufacturing standards for mechanical fasteners used in pressure equipment.
Export Packaging
Stud bolts intended for international shipment must be packaged to prevent corrosion and mechanical damage during transportation.
Packaging practices may include:
• Protective oil coating
• Moisture-resistant wrapping
• Wooden export crates
• Segregated packaging by material grade
Proper packaging helps preserve thread integrity and prevents contamination during shipping.
Logistics Coordination
Export supply typically requires coordination between manufacturing facilities, freight carriers, and project procurement teams.
Logistics considerations include:
• Batch traceability documentation
• Export compliance documentation
• Packing lists and inspection reports
• Shipping documentation for international customs clearance
Maintaining documentation integrity is important for project procurement verification.
14. Procurement Perspective in EPC Projects
In Engineering, Procurement, and Construction (EPC) projects, stud bolts are typically specified within piping material specifications (PMS) or approved vendor lists.
Procurement teams evaluate stud bolt suppliers based on several technical criteria.
Material Compliance
Stud bolts must be manufactured from materials meeting the chemical composition and mechanical property requirements defined in project specifications.
Material verification typically includes:
• Mill test certificates
• Positive material identification (PMI)
• Mechanical property testing
Dimensional Accuracy
Stud bolts must conform to dimensional standards to ensure compatibility with flange assemblies used in piping systems.
Critical dimensional factors include:
• Thread pitch accuracy
• Stud length tolerance
• Straightness
• Thread profile conformity
Dimensional non-conformance can affect bolt preload distribution and joint integrity.
Documentation Requirements
EPC procurement processes require comprehensive documentation verifying compliance with applicable standards.
Typical documentation packages include:
• Material test certificates
• Heat treatment records
• Dimensional inspection reports
• Hardness testing records
These documents are used by project engineers and third-party inspectors to confirm product conformity.
15. Installation Practices for Stud Bolts
Proper installation procedures are essential to ensure that stud bolts develop the required preload to maintain gasket compression in flange joints.
Improper tightening practices can result in uneven load distribution, flange distortion, or gasket leakage.
Bolt Tightening Sequence
Stud bolts in flange assemblies should be tightened using a cross-pattern sequence.
This pattern distributes load evenly across the flange and prevents localized overstressing of the gasket.
Typical tightening sequence steps include:
- Initial hand tightening of all nuts
- First torque pass at approximately 30% of final torque
- Second pass at approximately 60% of final torque
- Final pass at 100% specified torque
This gradual tightening process helps equalize bolt tension across all studs.
Torque Wrench Use
Controlled torque application is normally performed using calibrated torque wrenches or hydraulic torque equipment.
Proper torque application ensures that:
• Required preload is achieved
• Bolt stress remains within allowable limits
Calibration of torque equipment should be verified periodically according to project quality requirements.
Lubrication of Threads
Lubrication applied to stud threads reduces friction and improves consistency in preload achieved during tightening.
Typical lubricants include:
• Graphite-based compounds
• Molybdenum disulfide lubricants
The lubrication condition must be considered when determining torque values.
Re-Torque Practices
Some gasket materials experience relaxation after initial compression.
Re-torque procedures may therefore be performed after initial system pressurization or thermal cycling to restore required bolt preload.
Storage Practices
Proper storage of stud bolts before installation helps prevent corrosion and mechanical damage.
Recommended storage practices include:
• Dry storage environments
• Protection from moisture
• Segregation by material grade
• Retention of original identification markings
Maintaining traceability during storage ensures that materials remain identifiable prior to install
Custom Engineering Capabilities
Industrial piping systems and heavy equipment installations sometimes require stud bolts with dimensions or materials outside standard catalog ranges.
Manufacturers may produce customized stud bolts to meet project-specific requirements.
Typical customization options include:
• Non-standard stud lengths
• Special thread pitch configurations
• High-temperature alloy materials
• Project-specific identification marking
• Special corrosion-resistant coatings
Such customization is often required in large capital projects where equipment designs deviate from standard flange configurations.
Engineering Conclusion
Bolted flange joints remain one of the most widely used mechanical sealing systems in industrial piping networks. Within these assemblies, Stud Bolts function as the primary load-bearing components responsible for maintaining the clamping force required to compress gaskets and sustain pressure containment.
The performance of stud bolts depends on several engineering factors, including:
• Proper material selection
• Controlled manufacturing processes
• Heat treatment compliance
• Dimensional accuracy
• Correct installation procedures
International standards governing stud bolts define mechanical properties, dimensional tolerances, and testing requirements intended to ensure predictable performance in pressure-retaining applications.
For EPC projects, stud bolts are evaluated not only as mechanical fasteners but also as critical components within the overall integrity of piping and pressure equipment systems. Compliance with recognized standards, documented manufacturing processes, and traceable quality verification are therefore essential elements in the procurement and deployment of stud bolts used in industrial infrastructure.